When it comes to transporting brown sugar efficiently and safely, selecting the right pneumatic conveying system is crucial. The choice between positive pressure and negative pressure systems can significantly impact operational efficiency, cost, and product integrity. Understanding the key differences and how to distinguish between them is essential for making an informed decision. This article will explore the fundamentals of both systems, their applications, and the factors to consider when choosing the appropriate one for brown sugar handling.
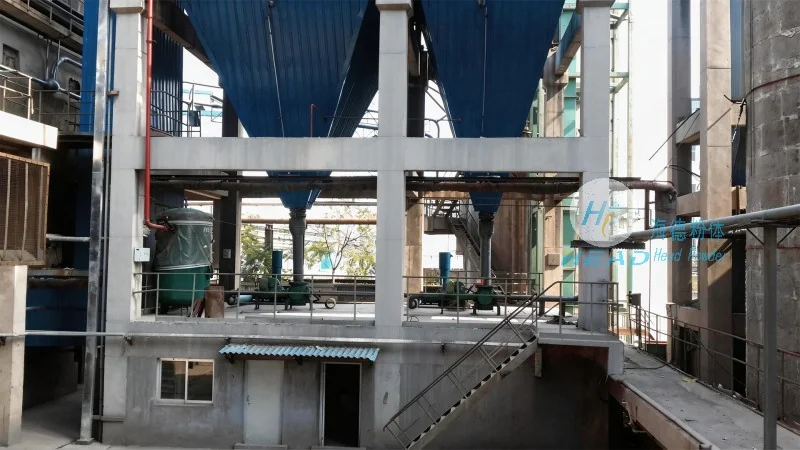
HeadPowder, a leading provider of pneumatic conveying solutions, specializes in customizing systems tailored to the unique needs of the sugar industry. With a focus on innovation and reliability, HeadPowder offers advanced technologies to enhance the efficiency and safety of brown sugar transportation. Based in Shandong, China, the company leverages decades of experience to deliver high-quality equipment and expert guidance for clients worldwide.
Pneumatic conveying is a method of transporting bulk materials like brown sugar using air or gas as the conveying medium. It involves moving the material through a pipeline by creating pressure differentials. The two primary types are positive pressure and negative pressure systems, each with distinct characteristics and applications.
Positive pressure conveying operates by blowing air into the pipeline, creating a positive pressure environment. The material is carried by the air stream, which moves from the source (e.g., a hopper or silo) to the destination (e.g., a storage tank or processing unit). This system is typically used for long-distance, high-capacity, and complex pipeline layouts. The air is supplied by a positive displacement blower or a centrifugal fan, and the pressure in the pipeline is maintained above atmospheric pressure.
Negative pressure conveying, on the other hand, creates a vacuum in the pipeline by drawing air out of the system. The material is drawn into the pipeline by the suction created by the air flow, moving from the source to the destination. This method is often employed for short-distance, low-capacity, or applications where dust containment is critical. The air is extracted by a vacuum pump, and the pressure in the pipeline is below atmospheric pressure.
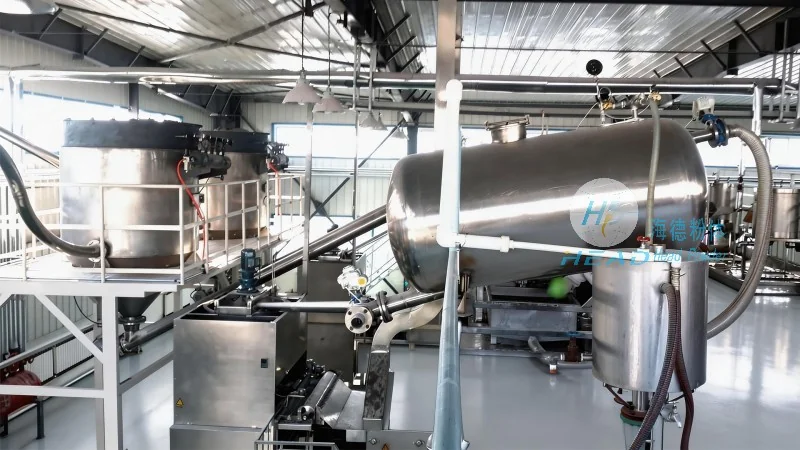
The choice between positive and negative pressure systems depends on several factors, including the distance of the conveying line, the material's properties, the required capacity, and the need for dust control. For brown sugar, which is often in granular form and can be prone to dust generation, the system must effectively manage particle flow and minimize product loss or contamination.
One critical factor is the pipeline layout. Positive pressure systems are better suited for long, complex pipelines with multiple bends and vertical lifts, as they can maintain consistent pressure and overcome resistance more effectively. Negative pressure systems are more suitable for short, straight pipelines where the material is moved over short distances with minimal changes in elevation.
Material properties also play a role. Brown sugar, being a dry, granular product, may require a system that can handle variations in particle size and moisture content. Positive pressure systems can handle larger particles and higher capacities, while negative pressure systems may be more effective for finer particles that require gentle handling to avoid degradation.
Dust control is another important consideration. Positive pressure systems can be equipped with dust collection and filtration systems to prevent dust from escaping into the environment. Negative pressure systems, by creating a vacuum, naturally draw dust into the pipeline, making it easier to capture and filter. However, this also means that the system must be well-sealed to prevent air leakage and maintain the vacuum.
There are several practical ways to distinguish between the two systems. First, check the pressure readings at the inlet and outlet of the pipeline. Positive pressure systems will show a pressure above atmospheric (e.g., 0.5 to 2 bar), while negative pressure systems will show a pressure below atmospheric (e.g., -0.5 to -2 bar). Second, observe the direction of air flow. In positive pressure systems, air moves from the blower into the pipeline, pushing the material forward. In negative pressure systems, air is drawn out of the pipeline by the vacuum pump, pulling the material in.
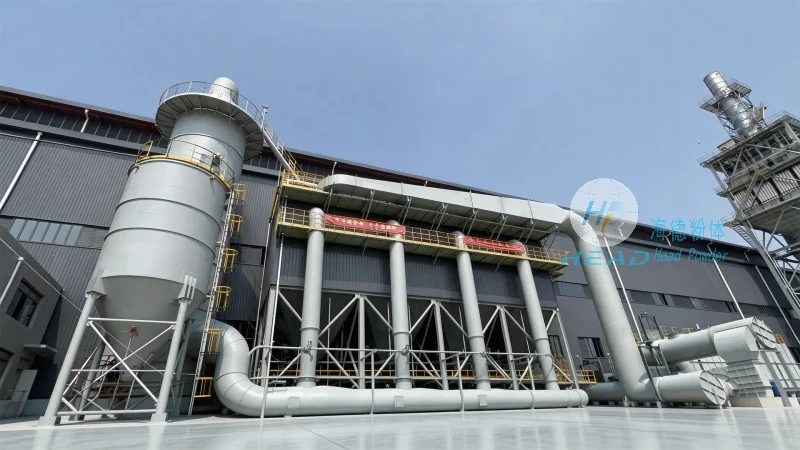
Third, examine the system components. Positive pressure systems typically include a blower, a hopper with a feeder, and a receiver with a dust filter. The blower is located at the inlet of the pipeline, and the air is directed into the material to be conveyed. Negative pressure systems consist of a vacuum pump, a hopper with a feeder, and a receiver with a dust filter. The vacuum pump is located at the outlet of the pipeline, and the air is drawn from the receiver to create suction.
For brown sugar processing facilities, the choice of system can impact overall operational efficiency. Positive pressure systems are commonly used in large-scale production where brown sugar is transported from storage silos to processing units over long distances. They can handle high capacities and complex layouts, making them ideal for industrial applications. Negative pressure systems are often used in smaller facilities or for short-distance transfers, such as moving brown sugar from a processing line to a packaging area.
HeadPowder's expertise lies in designing and implementing customized pneumatic conveying systems that meet the specific requirements of brown sugar handling. By evaluating the distance, material properties, and operational needs, HeadPowder can recommend the most suitable system—whether positive or negative pressure—to ensure optimal performance and product quality.
Choosing between positive and negative pressure pneumatic conveying systems for brown sugar requires careful consideration of various factors. Positive pressure systems offer advantages in long-distance, high-capacity applications with complex layouts, while negative pressure systems are better suited for short-distance, low-capacity, or dust-sensitive operations. By understanding the differences in pressure, air flow direction, and system components, and by evaluating the specific needs of the brown sugar handling process, facilities can select the most efficient and effective conveying system. HeadPowder Engineering, with its expertise and commitment to quality, provides the necessary guidance and solutions to help clients make informed decisions and optimize their brown sugar transportation processes.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top