Food powder pneumatic conveying equipment is a critical industrial solution designed for the efficient and hygienic transportation of bulk food powders. This machinery is widely utilized across the food processing sector, including applications involving flour, sugar, milk powder, and other fine food powders. The primary objective of this equipment is to ensure the safe and reliable transfer of powders between locations, while maintaining stringent product quality and hygiene standards throughout the process. Developed by Shandong HeadPowder Engineering Co., Ltd., a leading manufacturer based in Shandong, China, this equipment is engineered to meet the highest industry standards for food safety and operational efficiency.
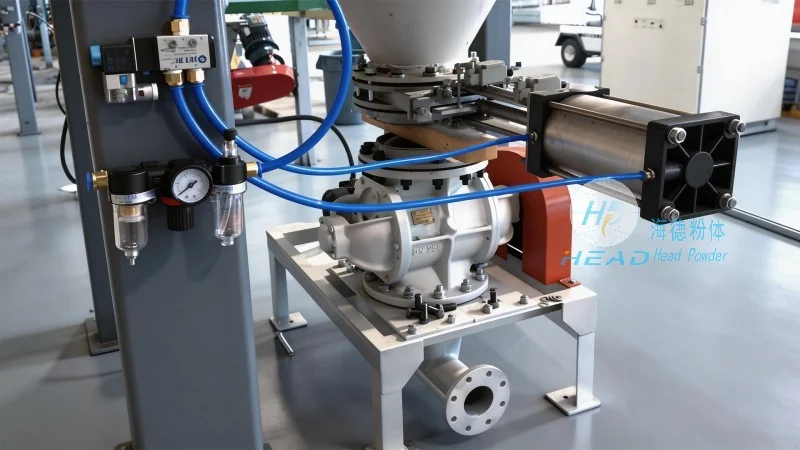
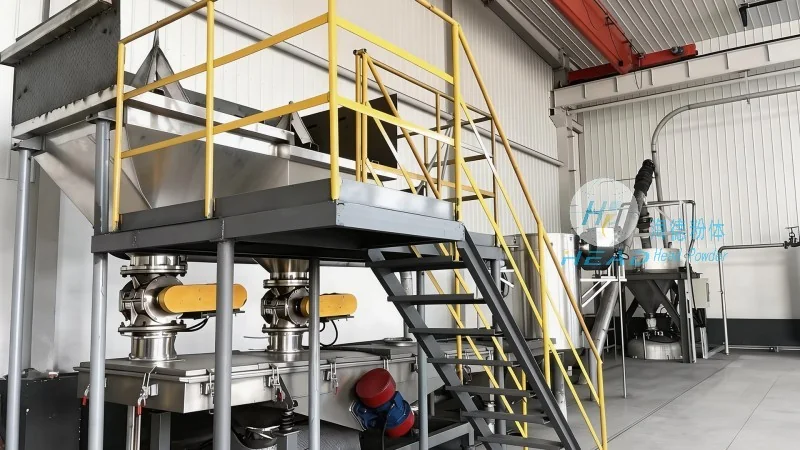
The operation of a food powder pneumatic conveying system relies on several interconnected components that work in unison to achieve efficient material handling. These components typically include a hopper for material storage, a conveyor line (operating under either positive or negative pressure), a dust collector, and a control system. The hopper is engineered to hold the food powder, ensuring a consistent feed to the conveyor system. The conveyor line serves as the core of the system, utilizing air pressure to move the powder through the pipeline. The dust collector is essential for maintaining air quality and preventing dust contamination, which is critical in food processing environments. The control system manages the entire operation, ensuring safe and efficient performance.
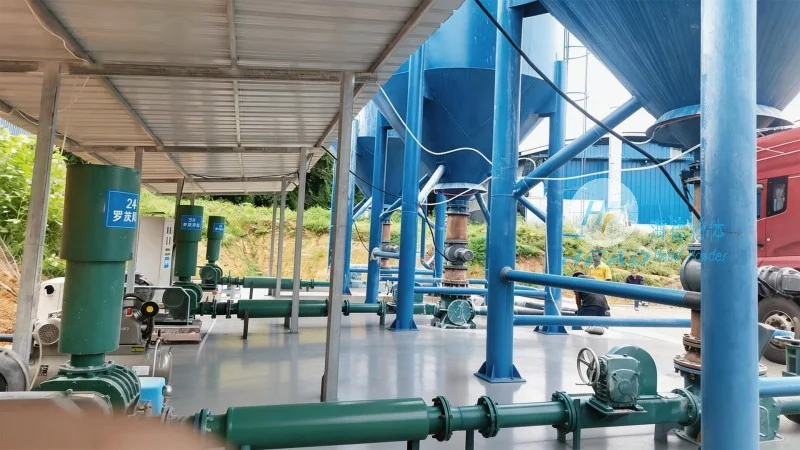
The operation process of a food powder pneumatic conveying machine begins with the loading of the food powder into the hopper. The powder is then fed into the conveyor line through a feeder, which regulates the flow rate. The conveyor line uses either positive pressure (where air is forced into the system to push the powder) or negative pressure (where air is drawn out to pull the powder). The positive pressure system is often preferred for food powders as it minimizes the risk of product contamination and ensures a smooth flow. As the powder moves through the pipeline, it is transported to the destination, such as a silo, storage tank, or processing unit. The system is designed to maintain consistent air pressure and flow rates to prevent clogging and ensure reliable operation.
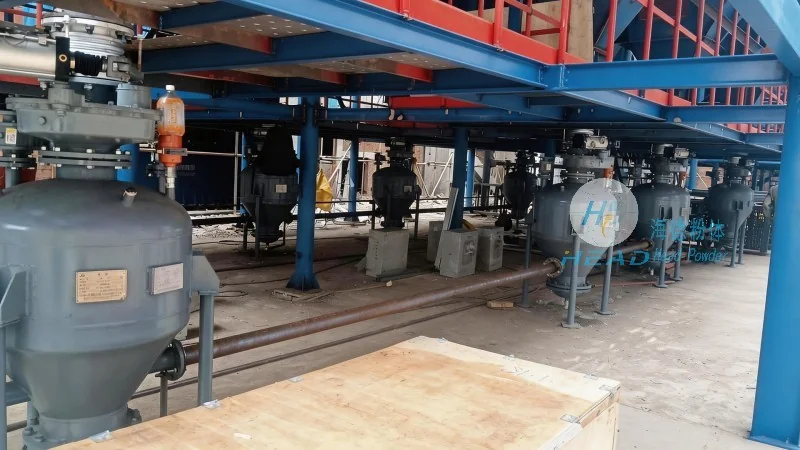
The working principle of food powder pneumatic conveying equipment is based on fluid dynamics and air movement principles. The system employs compressed air to create a flow that carries the food powder particles through the pipeline. The air and powder mixture is then separated at the destination, with the powder being collected and the air being filtered and recirculated. The positive pressure system operates by injecting high-pressure air into the hopper, which creates a pressure differential that propels the powder forward. The negative pressure system, conversely, draws air out of the pipeline, creating a vacuum that pulls the powder along. Both systems are designed to handle different types of food powders and operational requirements, ensuring optimal performance.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top