When it comes to transporting peas through pneumatic systems, businesses often face a critical decision: should they opt for positive pressure or negative pressure conveyance? This choice significantly impacts operational efficiency, equipment longevity, and overall system performance. Understanding the fundamental differences between these two methods is essential for selecting the most suitable solution for pea processing facilities.
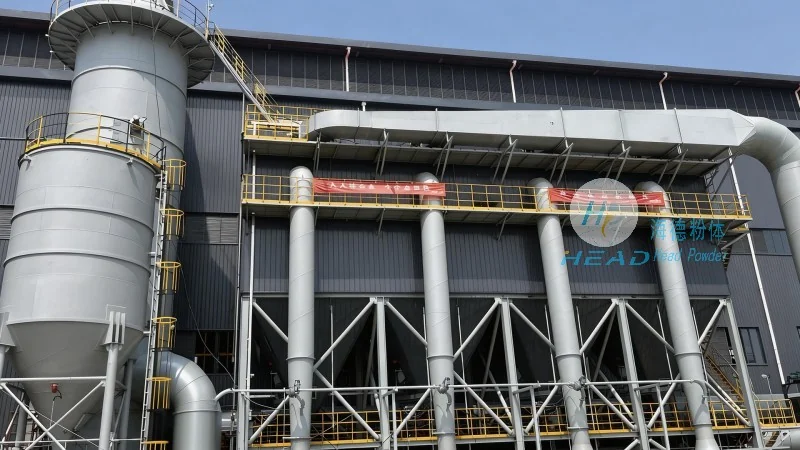
Positive pressure pneumatic conveying systems operate by forcing air or a carrier gas through the conveying line, pushing the material forward. In this method, the air moves in the same direction as the product flow. This approach is particularly effective for short to medium-distance transport and when dealing with bulk materials that may have a tendency to settle or clog. The positive pressure system ensures that the material is continuously propelled, reducing the risk of blockages and maintaining consistent flow rates. For pea processing, where the material is often dry and free-flowing, positive pressure can be an efficient choice for conveying from storage bins to processing lines.
Positive pressure systems typically use higher air velocities and pressures compared to negative pressure systems. This results in a more robust and reliable transport mechanism, especially when handling materials with varying particle sizes or moisture content. The equipment used in positive pressure systems includes high-pressure blowers or compressors, which generate the necessary force to move the material. The system design often incorporates features such as cyclone separators and filters to separate the product from the air stream, ensuring that the pea particles are collected efficiently and the air is cleaned before release. This method is generally more suitable for applications where the conveying distance is limited and the material is relatively dry and non-abrasive.
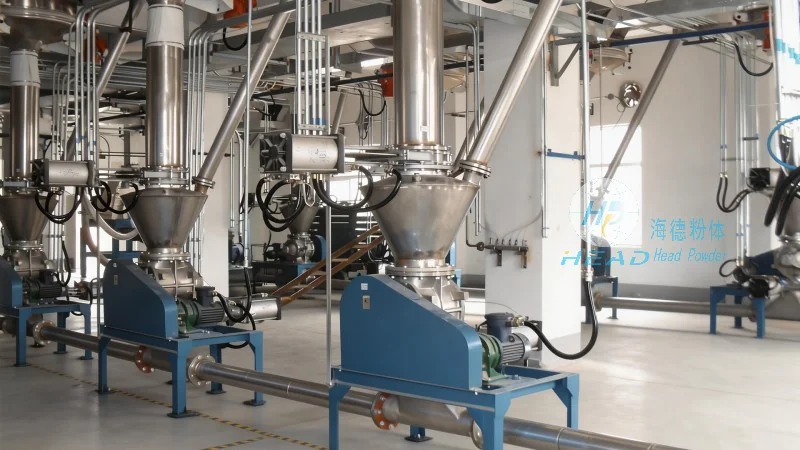
Negative pressure, or suction, pneumatic conveying systems work by creating a vacuum in the conveying line, drawing the material into the system. The air and product move in opposite directions, with the air being drawn into the system to pull the material along. This approach is ideal for longer distances and when the material needs to be transported from multiple points of origin to a central collection point. Negative pressure systems are commonly used in applications where the material is light and may be prone to dust or fine particles, as the vacuum helps to capture and transport these particles without the risk of spillage or contamination.
The primary distinction between positive and negative pressure systems lies in the direction of air flow and the method of material transport. Positive pressure systems use external force to push the material, while negative pressure systems rely on suction to draw the material in. This fundamental difference affects several key aspects of the system's performance and application suitability. For instance, positive pressure systems are generally more effective for short to medium distances and when the material is dense and has a high bulk density. In contrast, negative pressure systems excel in longer-distance transport and when dealing with materials that are light and may generate dust or require a more gentle handling approach.
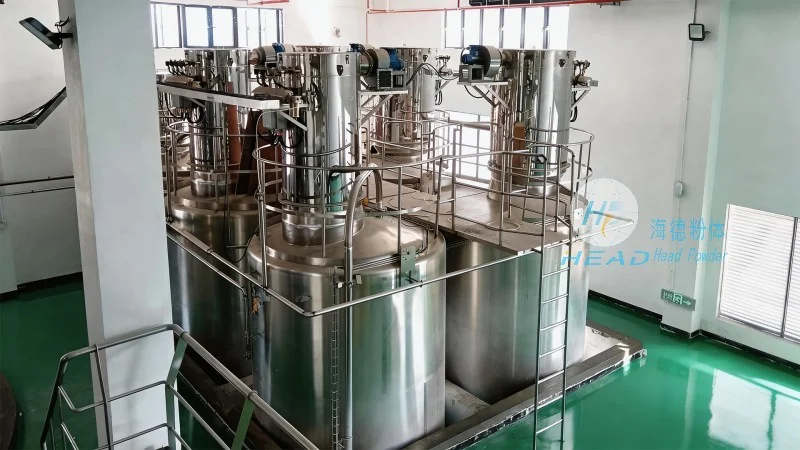
When selecting between positive and negative pressure pneumatic conveying for pea processing, several practical factors must be considered. The distance between the source and destination points is a critical factor. For short distances, such as moving peas from a storage silo to a processing machine within a few meters, a positive pressure system may be more cost-effective and efficient. Conversely, if the processing facility is spread over a larger area, with the need to transport peas from multiple storage locations to a central processing line over several hundred meters, a negative pressure system might be more suitable due to its ability to handle longer distances without significant pressure loss.
The physical properties of the pea material itself play a significant role in the choice of system. Peas are typically dry and have a relatively uniform particle size, which makes them well-suited for both positive and negative pressure systems. However, if the peas are moist or contain a high proportion of fine particles, the system design may need to account for increased friction and potential for clogging. Positive pressure systems may require additional components, such as cyclone separators with larger diameters, to handle the increased material load and prevent blockages. Negative pressure systems, on the other hand, may benefit from the use of filters to capture fine dust and maintain air quality.
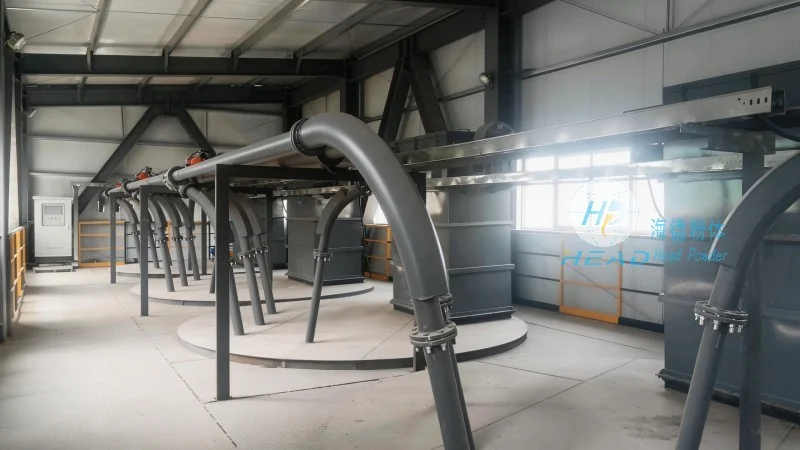
The cost and maintenance requirements of each system also influence the decision-making process. Positive pressure systems generally have higher initial costs due to the need for high-pressure blowers and robust piping. However, they often require less maintenance as the system operates under higher pressure, reducing the risk of leaks or material buildup. Negative pressure systems, while having lower initial costs, may require more frequent maintenance, particularly for filters and vacuum pumps, due to the continuous air flow and potential for dust accumulation. The operational costs, including energy consumption and replacement parts, should be evaluated over the system's lifecycle to determine the most economical choice for pea processing operations.
Choosing between positive and negative pressure pneumatic conveying for pea processing requires a careful assessment of operational needs, material characteristics, and system requirements. Positive pressure systems offer efficiency and reliability for short to medium-distance transport, while negative pressure systems provide flexibility and suitability for longer distances and varied material handling. By understanding the key differences in air flow direction, system design, and operational performance, pea processing facilities can select the most appropriate pneumatic conveying solution to optimize their production processes and ensure consistent quality in their final products.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top