Compound fertilizers are a cornerstone of modern agriculture, providing essential nutrients to crops while supporting sustainable farming practices. The efficient and reliable transport of these fertilizers from production facilities to distribution centers or application sites is critical for maintaining operational productivity and ensuring timely delivery to farmers. Traditional bulk material handling methods, such as belt conveyors or bucket elevators, often face challenges related to material degradation, contamination, and high energy consumption. In response to these limitations, pneumatic conveying technology has emerged as a superior alternative, offering a clean, efficient, and versatile solution for transporting compound fertilizers. This article provides an in-depth look at the principles, benefits, and practical applications of pneumatic conveying systems tailored for compound fertilizer transport, with a focus on the expertise of Shandong HeadPowder Engineering Co., Ltd., a leading provider of engineering solutions in this field.
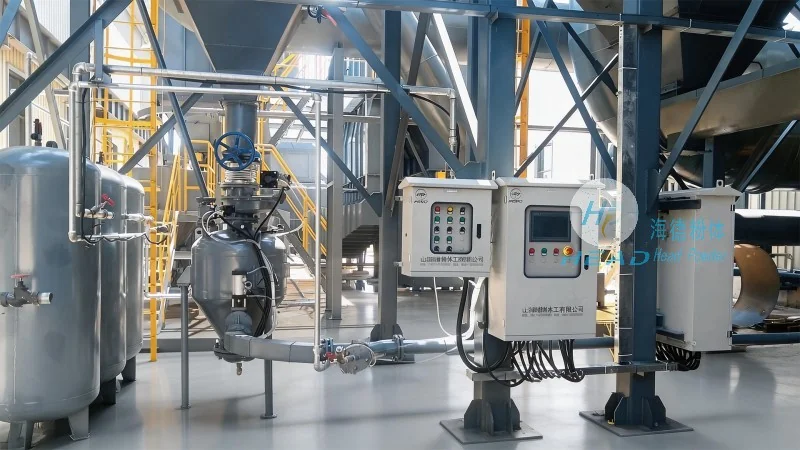
Pneumatic conveying systems utilize air or gas to transport bulk materials like compound fertilizers through a network of pipes. Unlike mechanical systems, which rely on physical contact and moving parts, pneumatic conveying minimizes product degradation and contamination, making it ideal for sensitive materials. The technology operates on the principle of creating a pressure differential between the conveying line and the ambient environment. By generating airflow, the system lifts and transports the fertilizer particles through the pipeline, delivering them to the desired destination with minimal loss and maximum efficiency. There are two primary types of pneumatic conveying systems: pressure and vacuum. Pressure systems use positive pressure to push material through the line, while vacuum systems use negative pressure to pull material. For compound fertilizers, pressure systems are often preferred due to their ability to handle high volumes and long distances with consistent performance. Shandong HeadPowder Engineering Co., Ltd. specializes in designing and manufacturing customized pneumatic conveying solutions that cater to the specific characteristics of compound fertilizers, ensuring optimal performance and reliability.
Implementing pneumatic conveying for compound fertilizer transport offers numerous advantages over traditional methods. First and foremost, it provides a clean and hygienic transport process, preventing cross-contamination between different fertilizer types or with other materials. This is particularly important in facilities where multiple fertilizer blends are handled, as it maintains product integrity and quality. Additionally, pneumatic conveying reduces material handling losses, as the system minimizes spillage and dust generation during transport. The enclosed pipeline system also helps control dust emissions, contributing to a safer and more environmentally friendly operation. From an operational perspective, pneumatic conveying systems are highly efficient, with lower energy consumption compared to mechanical conveyors, especially over long distances. They also offer greater flexibility in layout, allowing for complex routing and integration with existing production and storage infrastructure. Furthermore, these systems can be easily automated, enabling seamless integration with other process control systems and improving overall operational efficiency. Shandong HeadPowder Engineering Co., Ltd. leverages advanced engineering and material science to design pneumatic conveying systems that maximize these benefits, ensuring that clients achieve significant cost savings and improved productivity.
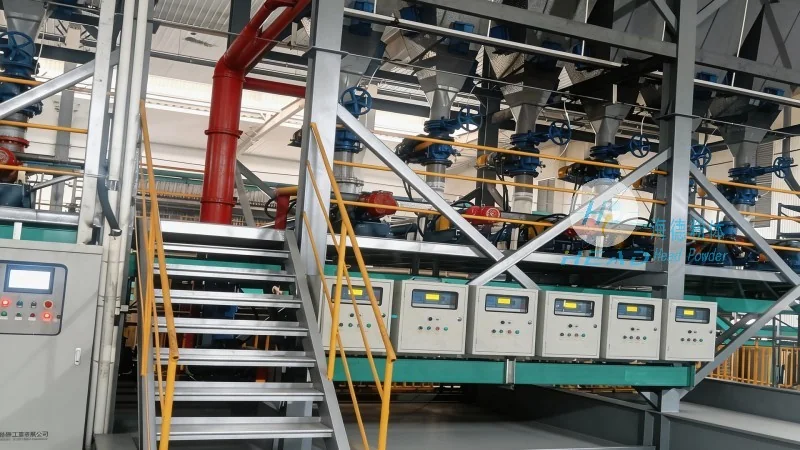
Effective pneumatic conveying of compound fertilizers relies on a combination of specialized components working in harmony. The core components include a material feeder, which accurately meters and introduces the fertilizer into the conveying line. The feeder must be designed to handle the specific flow characteristics of compound fertilizers, ensuring consistent material feed without blockages or segregation. A positive displacement blower or air compressor provides the necessary pressure to drive the material through the pipeline. The blower’s capacity and pressure rating are critical factors, as they determine the system’s throughput and transport distance capabilities. The conveying line itself is typically made of durable materials like stainless steel or corrosion-resistant alloys, capable of withstanding the abrasive nature of fertilizer particles and the effects of moisture or chemicals. To ensure smooth material flow and prevent blockages, the system may include in-line mixers or agitators, which help break up clumps and maintain a uniform flow rate. Additionally, the system incorporates control valves and sensors to monitor pressure, flow, and material levels, enabling real-time adjustments and preventing system failures. Shandong HeadPowder Engineering Co., Ltd. employs state-of-the-art design tools and simulation software to optimize these components, ensuring that each system is tailored to the client’s specific operational requirements and material characteristics.
Every compound fertilizer facility has unique operational needs, and a one-size-fits-all approach to pneumatic conveying is insufficient. Shandong HeadPowder Engineering Co., Ltd. recognizes this and offers comprehensive customization services to meet the specific demands of each client. The company works closely with clients to conduct thorough site assessments and process analyses, identifying the optimal conveying system configuration. This includes determining the required throughput, transport distance, and material characteristics, such as particle size, moisture content, and bulk density. Based on these analyses, the engineering team designs a customized system that integrates seamlessly with existing infrastructure, such as storage silos, blending equipment, and packaging lines. The company’s expertise in material handling engineering allows for the integration of pneumatic conveying with other processes, such as automated blending and quality control, creating a fully integrated material handling solution. Customization also extends to the system’s control and monitoring capabilities, with options for local or remote operation, data logging, and integration with enterprise resource planning (ERP) systems. This level of customization ensures that the pneumatic conveying system not only meets current operational needs but also supports future expansion and technological upgrades. Shandong HeadPowder Engineering Co., Ltd. emphasizes client collaboration throughout the design and implementation process, ensuring that the final solution is not only technically advanced but also practical and cost-effective.
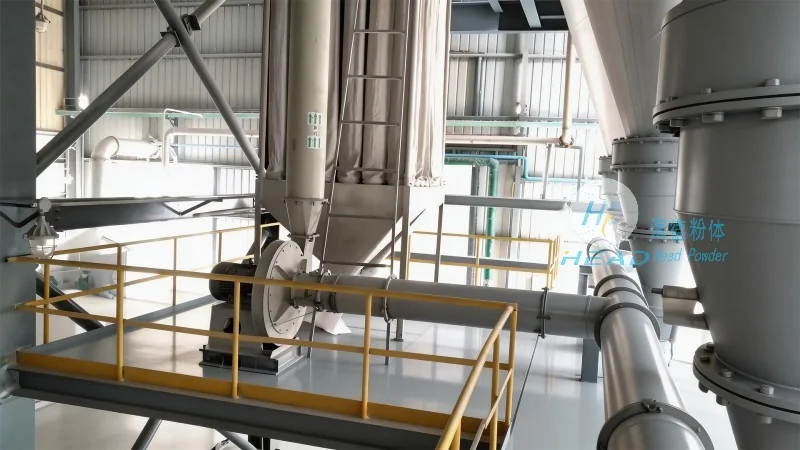
Shandong HeadPowder Engineering Co., Ltd. has successfully implemented pneumatic conveying systems for compound fertilizer transport in numerous projects across China. These case studies demonstrate the effectiveness and reliability of the company’s solutions. For example, a large fertilizer production facility in Shandong Province required a system to transport high-volume compound fertilizers from storage silos to packaging lines over a distance of 500 meters. The existing mechanical conveyor system was experiencing frequent breakdowns and material losses due to clumping and abrasion. By installing a customized pressure pneumatic conveying system, the facility achieved a 30% increase in throughput, reduced material losses by 15%, and minimized dust emissions. The system’s enclosed design also improved workplace safety, as it eliminated the need for manual handling of bulk materials. Another project involved a fertilizer blending plant that needed to transport multiple fertilizer blends to a distribution center. The company designed a multi-line pneumatic conveying system with individual control for each blend, ensuring precise and hygienic transport. The system’s flexibility allowed the plant to switch between different fertilizer types without interrupting production, improving operational efficiency. These case studies highlight the practical benefits of pneumatic conveying systems and the expertise of Shandong HeadPowder Engineering Co., Ltd. in delivering tailored solutions that address specific client challenges.
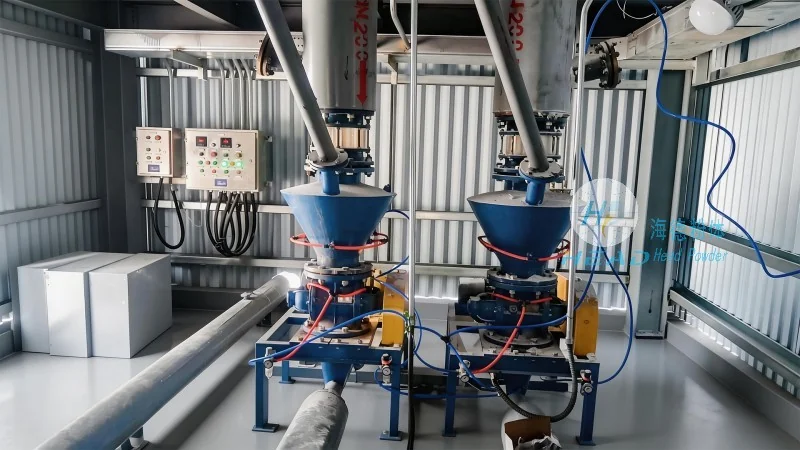
Ensuring the long-term performance and reliability of pneumatic conveying systems is crucial for maintaining operational efficiency and minimizing downtime. Shandong HeadPowder Engineering Co., Ltd. provides comprehensive maintenance and support services to help clients maximize the lifespan of their systems. Regular maintenance includes inspecting and cleaning key components, such as the material feeder, blower, and conveying line, to prevent blockages and ensure optimal airflow. The company recommends scheduled maintenance intervals based on the system’s usage and material characteristics, helping to identify potential issues before they lead to system failures. Additionally, the engineering team offers technical support and troubleshooting services, providing guidance on system operation and maintenance. By implementing a proactive maintenance strategy, clients can extend the life of their pneumatic conveying systems, reduce repair costs, and maintain consistent performance over time. The durability of the components, particularly the conveying line and blower, is a key factor in long-term performance. Shandong HeadPowder Engineering Co., Ltd. uses high-quality materials and robust designs to ensure that its systems can withstand the harsh conditions of compound fertilizer transport, providing reliable service for years to come.
Pneumatic conveying technology represents a significant advancement in the efficient and clean transport of compound fertilizers. By leveraging the expertise of companies like Shandong HeadPowder Engineering Co., Ltd., fertilizer producers can achieve higher productivity, reduced costs, and improved product quality. The benefits of pneumatic conveying—clean transport, reduced losses, energy efficiency, and flexibility—make it an ideal solution for modern fertilizer facilities. As the demand for compound fertilizers continues to grow, the adoption of advanced material handling technologies will be essential for meeting operational challenges and supporting sustainable agricultural practices. Shandong HeadPowder Engineering Co., Ltd. remains committed to providing innovative and reliable pneumatic conveying solutions, helping clients optimize their material handling processes and achieve long-term success in the fertilizer industry.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top