Chlorinated polyethylene (CPE) is a widely used polymer in various industrial applications due to its excellent weather resistance, chemical stability, and low temperature flexibility. When transporting CPE via pneumatic conveying systems, preventing pipeline blockages is a critical challenge that can significantly impact production efficiency and system reliability. This article explores effective strategies to mitigate blockages in air-lifted CPE delivery and highlights the essential design parameters that ensure smooth operation.
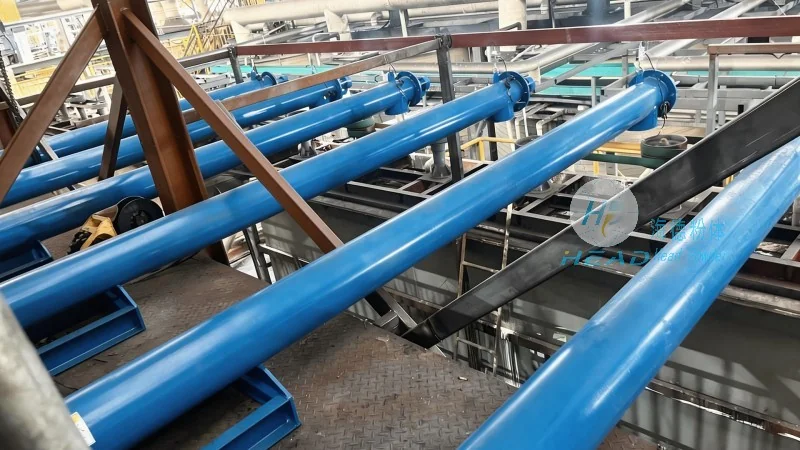
Pneumatic conveying systems rely on air flow to transport bulk materials like CPE through pipelines. However, CPE particles can exhibit cohesive properties that lead to agglomeration and blockages, especially at high concentrations or in long-distance transport. The risk of blockage increases with particle size, moisture content, and the presence of contaminants. To address these challenges, a systematic approach to system design is essential, focusing on material characteristics, air velocity, and pipeline configuration.
Several critical design parameters must be optimized to ensure efficient and unobstructed CPE transport through pneumatic systems. The first parameter is the air velocity, which must be maintained at a level that prevents particle settling but avoids excessive energy consumption. For CPE, typical conveying velocities range from 20 to 30 m/s, depending on particle size and pipeline diameter. Higher velocities can reduce the likelihood of blockages but increase operational costs. Conversely, insufficient velocity may lead to material accumulation and eventual clogging.
Another crucial parameter is the pipeline diameter and length. Larger diameters reduce friction losses and the risk of particle impact, while longer pipelines require higher air velocities to maintain material suspension. The use of smooth, corrosion-resistant materials for pipeline construction is also vital. Stainless steel or high-density polyethylene (HDPE) are common choices for CPE transport, as they minimize material adhesion and corrosion. Additionally, incorporating bends and elbows with gradual radii helps maintain air flow continuity and prevents pressure drops that could lead to blockages.
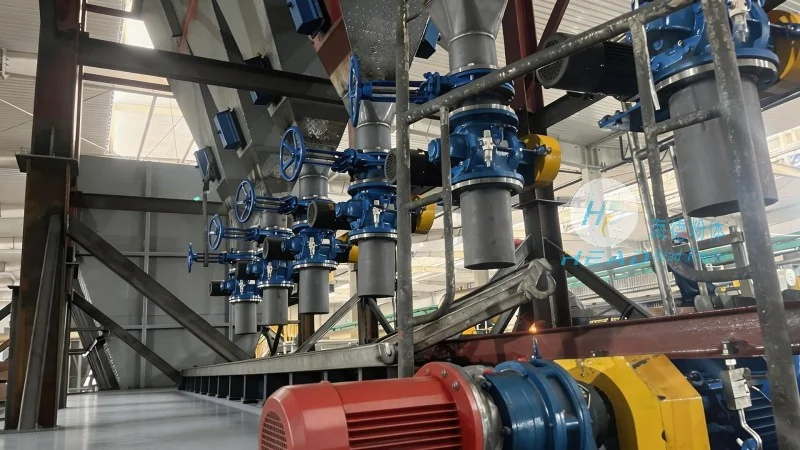
Feeder design is another critical aspect. The feeder must provide a consistent flow rate without creating surges or surpluses that could lead to material buildup. Screw feeders or rotary valves are often used for CPE, as they can handle cohesive materials and maintain a steady feed rate. The feeder's speed and capacity must be matched to the system's air flow and pipeline size to avoid overloading the conveying line.
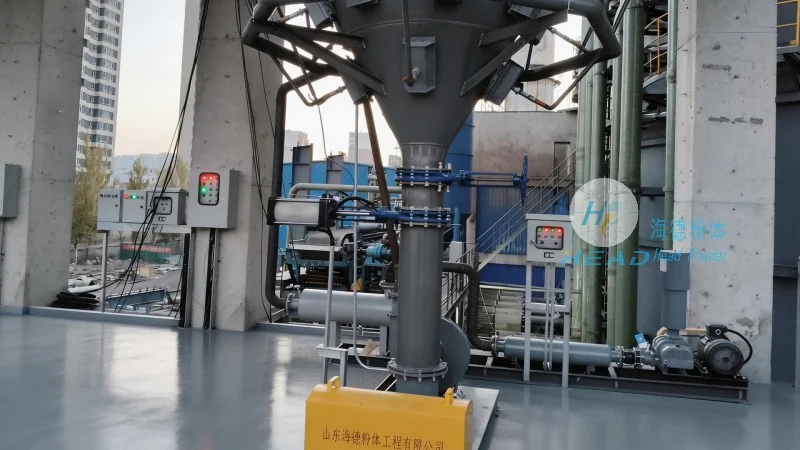
Preventing blockages also involves proper material handling and conditioning before entering the pneumatic system. CPE particles should be dried to reduce moisture content, as moisture can cause agglomeration and increase the risk of blockages. Drying equipment, such as rotary dryers or fluidized bed dryers, can be integrated into the system to ensure the material is in a dry state. Additionally, screening or sieving processes can remove oversized particles or contaminants that may contribute to blockages.
Conditioning the material by adding a small amount of anti-caking agent or lubricant can improve flow characteristics. However, it is essential to use compatible additives that do not affect the CPE's properties or the system's performance. Proper mixing and blending of additives are crucial to ensure uniform distribution and avoid localized blockages.
Even with optimal design, regular monitoring and maintenance are necessary to prevent blockages and ensure long-term system performance. Installing pressure sensors and flow meters along the pipeline allows operators to detect abnormal pressure drops or flow reductions, which may indicate impending blockages. Real-time monitoring systems can provide early warnings and enable timely intervention to prevent system shutdowns.
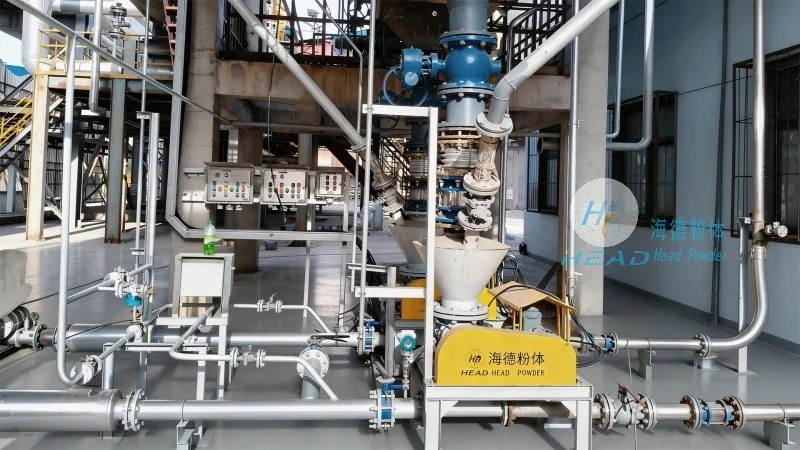
Maintenance activities should include regular cleaning of pipelines, feeders, and air filters. CPE particles can accumulate on surfaces over time, reducing flow capacity and increasing the risk of blockages. Cleaning procedures, such as reverse air flow or mechanical cleaning, should be scheduled based on system usage and material characteristics. Additionally, replacing worn components, such as seals and bearings, can prevent leaks or malfunctions that may contribute to blockages.
Preventing pipeline blockages in air-lifted chlorinated polyethylene transport requires a comprehensive approach that integrates optimal design parameters, material conditioning, and regular maintenance. By focusing on air velocity, pipeline configuration, feeder design, and material handling, pneumatic conveying systems can operate efficiently and reliably, minimizing downtime and maximizing production output. The expertise of companies like Shandong HeadPowder Engineering Co., Ltd. in pneumatic system design and material transport ensures that these critical parameters are addressed effectively, providing industrial clients with robust solutions for CPE delivery.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top