HeadPowder, a leading engineering company based in Shandong, China, specializes in the design and implementation of advanced pneumatic conveying systems tailored for the efficient transport of magnesium hydroxide over long distances. This system represents a sophisticated solution that addresses the unique challenges associated with handling fine powders like magnesium hydroxide, ensuring minimal product degradation and optimal operational efficiency.
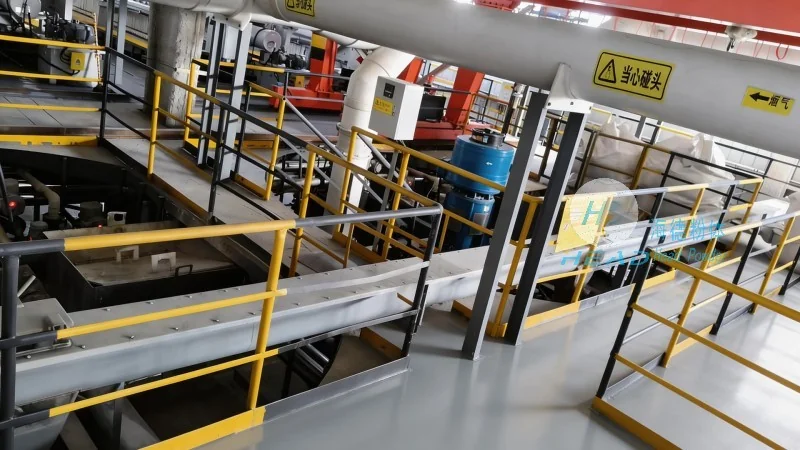
The long - distance pneumatic conveying system for magnesium hydroxide is engineered to deliver reliable and continuous material transport from the source to the destination. Key components include a high - capacity material feeder, a powerful air compressor system, and a network of pipelines equipped with specialized valves and control mechanisms. The system is designed to handle varying flow rates and pressures, adapting to the specific requirements of industrial applications such as chemical processing, pharmaceutical manufacturing, and environmental remediation.
Compared to traditional bulk material handling methods like belt conveyors or screw conveyors, pneumatic conveying offers several distinct advantages for magnesium hydroxide transport. The system minimizes product contamination and degradation by avoiding direct contact with metal surfaces, which is critical for maintaining the purity of magnesium hydroxide used in various industrial applications. Additionally, it enables seamless integration with existing production lines, reducing downtime and operational complexity. The ability to transport materials over extended distances without the need for intermediate storage or transfer points enhances overall process efficiency and reduces labor costs.
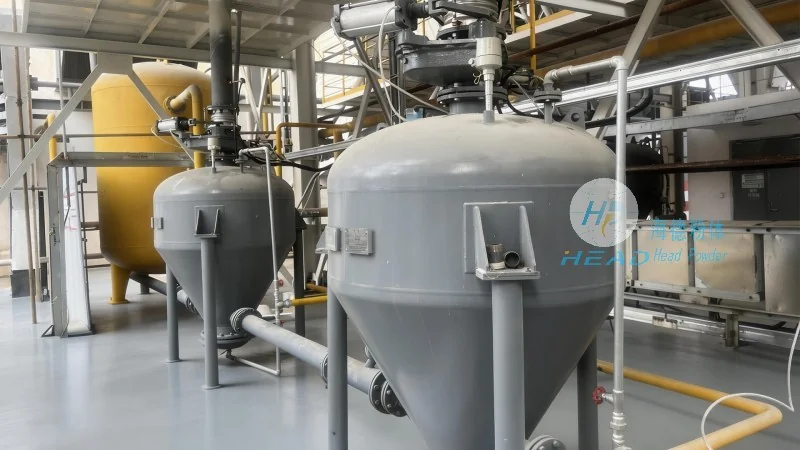
HeadPowder understands that each industrial project has unique specifications. Therefore, the pneumatic conveying system is highly customizable to meet specific operational needs. The system can be scaled to accommodate different production capacities, from small - scale laboratory applications to large - scale industrial operations. This flexibility allows clients to adapt the system as their business grows or as their material handling requirements evolve. The engineering team at HeadPowder works closely with clients to design a system that aligns with their production goals, ensuring optimal performance and cost - effectiveness.
Reliability is a top priority in the design of the long - distance pneumatic conveying system. High - quality materials and robust construction are used to ensure long service life and minimal maintenance requirements. The system incorporates advanced monitoring and control features that allow for real - time performance tracking and predictive maintenance. This proactive approach helps in identifying potential issues before they lead to system failures, reducing unexpected downtime and maintenance costs. Regular maintenance procedures are straightforward, and the company provides comprehensive support to clients, including training and technical assistance, to ensure the system operates at peak efficiency.
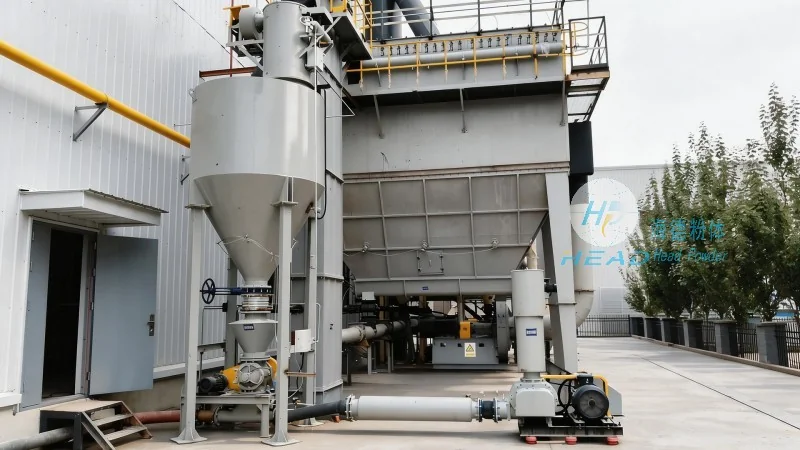
HeadPowder is committed to sustainable engineering practices. The pneumatic conveying system is designed with environmental impact in mind. By eliminating the need for water or other liquids in the conveying process, it reduces waste and minimizes the risk of contamination. The system also incorporates dust collection and filtration components to ensure compliance with environmental regulations and to protect the health and safety of personnel. This focus on environmental responsibility aligns with the growing demand for eco - friendly industrial solutions in the global market.
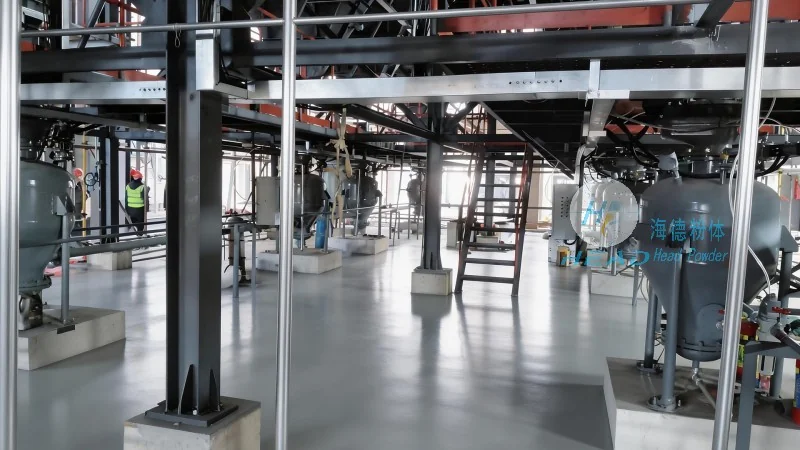
The long - distance pneumatic conveying system for magnesium hydroxide has been successfully implemented in various industries. For instance, in the chemical industry, it is used to transport magnesium hydroxide from storage silos to processing units, ensuring a consistent supply of raw material. In pharmaceutical manufacturing, the system maintains the high purity standards required for drug production by preventing cross - contamination. Environmental remediation projects also benefit from this technology, as it allows for the safe and efficient transport of magnesium hydroxide used in water treatment processes. These applications demonstrate the versatility and effectiveness of the system in different industrial settings.
HeadPowder's long - distance pneumatic conveying system for magnesium hydroxide represents a cutting - edge solution that combines advanced engineering with practical application. By addressing the specific challenges of handling fine powders over extended distances, the system enhances operational efficiency, product quality, and environmental sustainability. With a strong commitment to customization and reliability, HeadPowder continues to be a trusted partner in providing innovative material handling solutions for industries worldwide.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top