For industries dealing with fine powders like quartz, efficient material handling is crucial for maintaining product quality and operational efficiency. Pneumatic conveying systems offer a solution that can significantly enhance the process of transporting quartz powder from one location to another. This article explores the application and optimization of pneumatic conveying technology specifically tailored for quartz powder handling, highlighting key considerations and benefits.
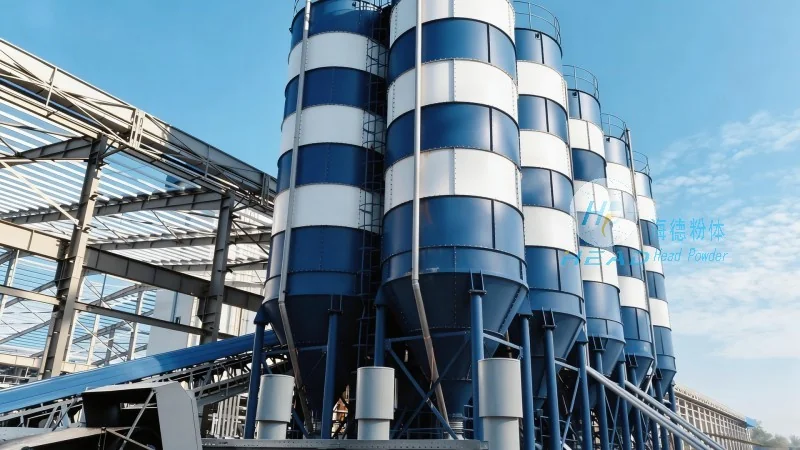
Quartz powder, with its fine particle size and potential for static charge accumulation, requires specialized handling methods to prevent clogging, dust generation, and material degradation. Pneumatic conveying uses compressed air or gas to transport dry bulk materials through a pipeline system. In the context of quartz powder, this technology provides a dust-free, enclosed method of transport that minimizes contamination and ensures consistent product quality. The design of the conveying system must account for the specific properties of quartz, such as its density, particle size distribution, and flow characteristics, to achieve optimal performance.
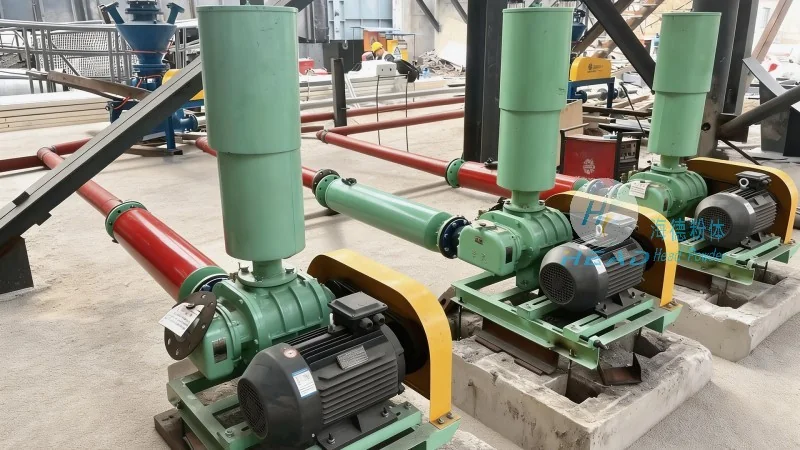
The effectiveness of a pneumatic conveying system for quartz powder depends on several critical components. These include the air compressor, which provides the necessary pressure to move the material; the feed hopper, which controls the flow of quartz powder into the system; and the pipeline network, which transports the material to the destination. Additionally, features like in-line mixers, cyclone separators, and dust collectors are often integrated to enhance system performance and ensure compliance with environmental regulations. Each component must be carefully selected and sized to match the specific requirements of the quartz powder application, ensuring reliable and efficient operation.
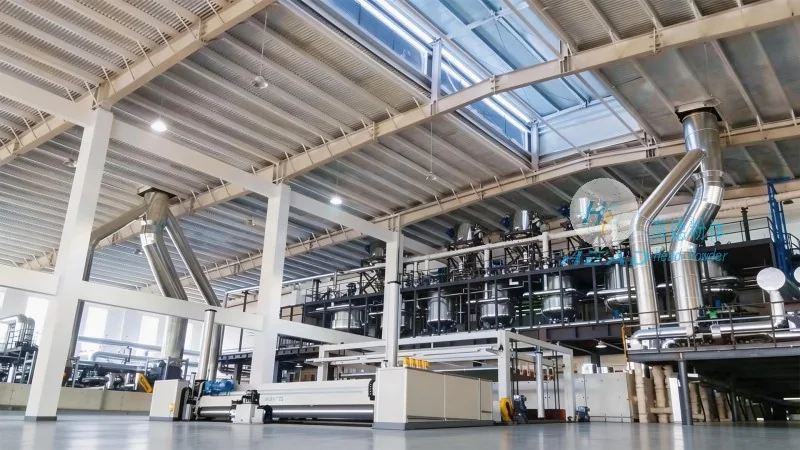
Optimization of pneumatic conveying systems for quartz powder involves several strategies aimed at maximizing efficiency, minimizing energy consumption, and reducing maintenance costs. One key approach is the selection of the appropriate conveying velocity, which balances the need to prevent material deposition in the pipeline with the requirement to minimize air consumption. Proper system sizing, based on the flow rate and particle characteristics of the quartz powder, is essential to avoid under- or over-pressurization. Regular maintenance, including cleaning of the pipeline and replacement of worn components, is also critical to maintain system performance and extend equipment life. Advanced control systems can further optimize operation by monitoring pressure, flow, and other parameters in real-time, adjusting system settings to adapt to changing conditions.
Adopting an optimized pneumatic conveying system for quartz powder handling offers numerous benefits for industrial operations. These include improved product quality through reduced contamination and dust exposure, enhanced operational safety by eliminating manual handling of powders, and increased productivity through faster and more reliable material transport. The enclosed nature of the system also helps in maintaining a clean working environment, which is particularly important in industries where product purity is paramount. Furthermore, optimized systems can lead to significant cost savings over time by reducing energy consumption, minimizing downtime due to clogging or equipment failure, and extending the lifespan of the conveying components.
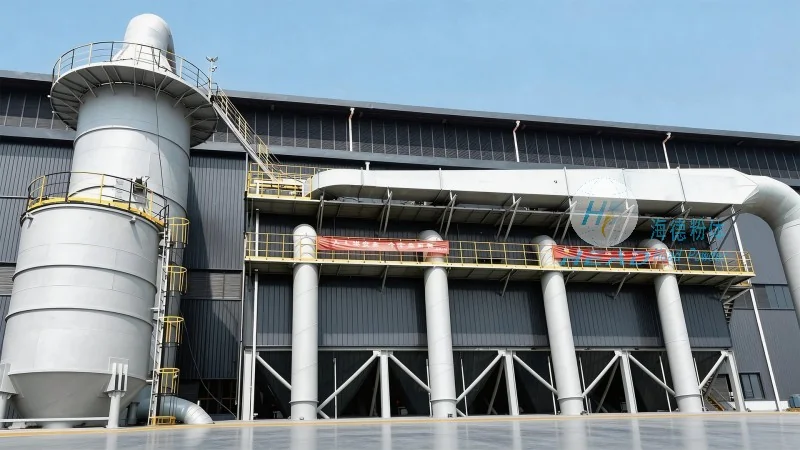
For companies dealing with quartz powder, investing in a well-designed and optimized pneumatic conveying system is a strategic decision that can yield long-term benefits. By understanding the specific requirements of quartz powder and implementing the right components and control strategies, industries can achieve efficient, reliable, and cost-effective material handling. Shandong HeadPowder Engineering Co., Ltd., with its expertise in engineering and manufacturing, offers tailored solutions that address the unique challenges of quartz powder handling, ensuring that clients receive systems that are optimized for their specific applications and operational needs.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top