HeadPowder, a leading engineering company based in Shandong, China, specializes in the design and implementation of pneumatic conveying systems for cement raw materials. This article provides an in-depth exploration of the working principles and classification applications of cement raw material pneumatic conveying, offering valuable insights for industry professionals.
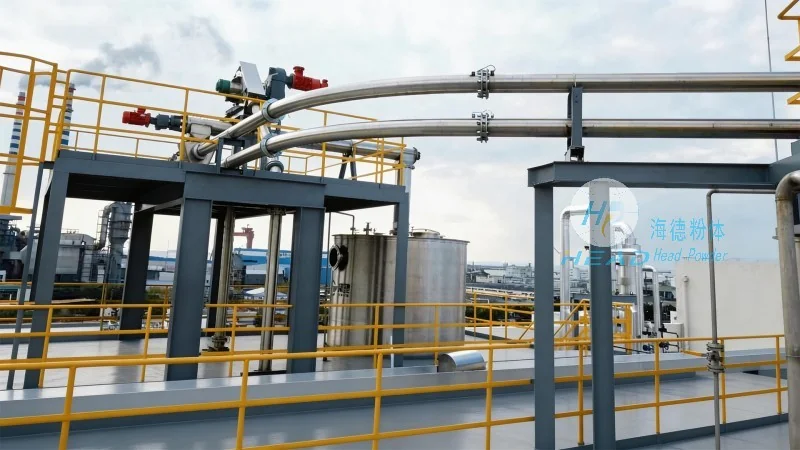
Pneumatic conveying, also known as air conveying, is a method of transporting bulk materials like cement raw materials (such as limestone, clay, and iron ore) using a stream of pressurized or vacuum air. This technology has become increasingly popular in the cement industry due to its efficiency, flexibility, and ability to handle a wide range of materials. The fundamental principle involves the use of air to create a flow that moves particles through a pipeline, eliminating the need for mechanical components like belts or buckets in traditional systems.
The working principle of cement raw material pneumatic conveying is centered on the interaction between the material particles and the air stream. In a typical system, raw materials are fed into a hopper, where they are then drawn or pushed by a controlled airflow through a pipeline. The key to efficient conveying lies in maintaining a stable flow rate and ensuring that the air velocity is sufficient to lift and transport the particles without causing excessive wear or degradation. The system typically includes components such as a feeder, a pipeline network, a separator, and a discharge device. The feeder controls the material feed rate, while the pipeline transports the material to the destination. The separator separates the material from the air stream, and the discharge device delivers the material to the next processing stage.
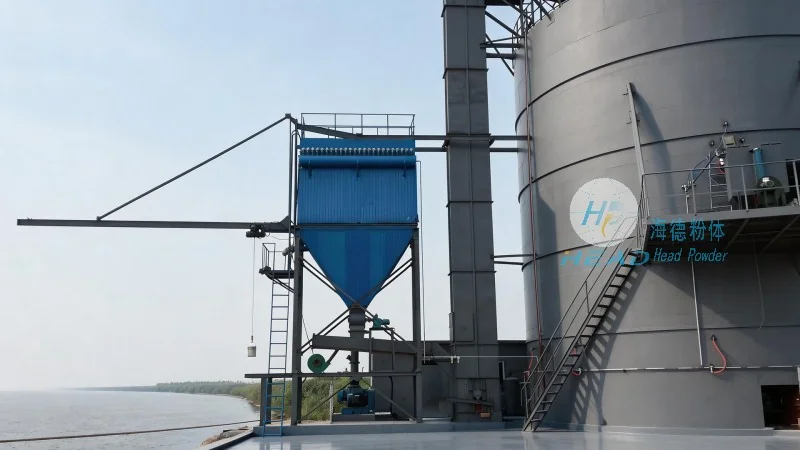
Pneumatic conveying systems for cement raw materials are broadly classified into three main types: suction (or vacuum) conveying, pressure conveying, and mixed (or combined) conveying. Each type has distinct characteristics and is suited to different operational requirements and material handling scenarios.
Suction conveying systems operate by creating a vacuum at the inlet of the pipeline, which draws the material from the source location. This method is ideal for applications where the material needs to be transported from a lower elevation or over short distances. The system typically uses a vacuum pump to generate the required pressure differential. Suction conveying is particularly effective for handling fine powders and granular materials, as it can maintain a consistent flow without causing material degradation. However, it has limitations in terms of the maximum distance and material size it can handle efficiently.
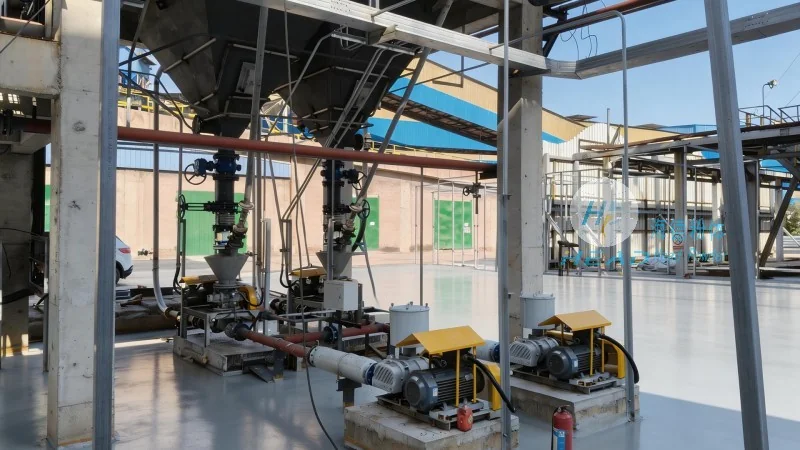
Pressure conveying systems, on the other hand, use compressed air to push the material through the pipeline. The system operates by injecting high-pressure air into the material stream at the inlet, which accelerates the particles and propels them through the pipeline. This method is suitable for longer distances and larger material particles. Pressure conveying systems are often used in applications where the material needs to be transported from a higher elevation or over significant distances. The main advantage of pressure conveying is its ability to handle larger particles and higher material loads, making it ideal for bulk material transport in cement plants.
Mixed conveying systems combine elements of both suction and pressure conveying. They use a combination of vacuum and pressure to achieve efficient material transport. This approach allows for greater flexibility in handling a wide range of materials and operational conditions. Mixed systems are particularly useful in complex conveying networks where materials need to be transported over varying distances and elevations. The system typically includes a vacuum section for initial material pickup and a pressure section for the final transport, ensuring optimal performance and energy efficiency.
The classification of pneumatic conveying systems directly impacts their application in the cement industry. Suction systems are commonly used for transporting raw materials from stockpiles to the raw mill, where the material is ground into fine powders. Pressure systems are often employed for transporting finished raw meal from the mill to the kiln, where it is calcined to form clinker. Mixed systems are used in scenarios where the material needs to be transported over long distances or through complex network configurations, such as in large-scale cement production facilities.
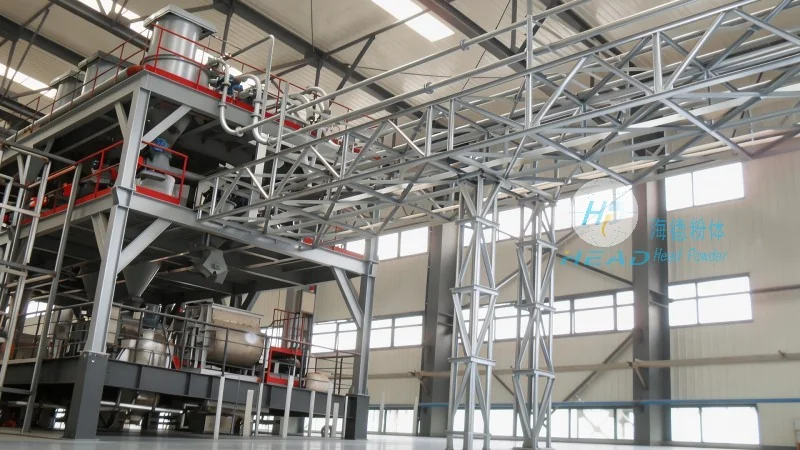
Implementing pneumatic conveying systems for cement raw materials offers several advantages over traditional mechanical systems. First, it eliminates the need for mechanical components like conveyors or elevators, reducing maintenance costs and downtime. Second, it provides a cleaner and more hygienic environment, as the material is enclosed within the pipeline, preventing dust and contamination. Third, it offers greater flexibility in terms of layout and material handling, allowing for easy integration into existing cement plant infrastructure. Finally, pneumatic conveying systems are energy-efficient, as they use air to transport materials, which is more cost-effective compared to mechanical systems that rely on motors and belts.
HeadPowder Engineering Co., Ltd., with its headquarters in Shandong, China, provides comprehensive solutions for cement raw material pneumatic conveying systems. By understanding the working principles and classification applications of these systems, cement manufacturers can optimize their material handling processes, improve efficiency, and reduce operational costs. The company's expertise in designing and implementing tailored pneumatic conveying solutions ensures that clients receive systems that meet their specific operational requirements and material characteristics.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top