HeadPowder, a leading engineering firm based in Shandong, China, specializes in advanced solutions for sintered dust pneumatic conveying systems. This article provides an in-depth exploration of the working principles, classification methods, and practical applications of such systems, offering valuable insights for industry professionals seeking efficient material handling solutions.
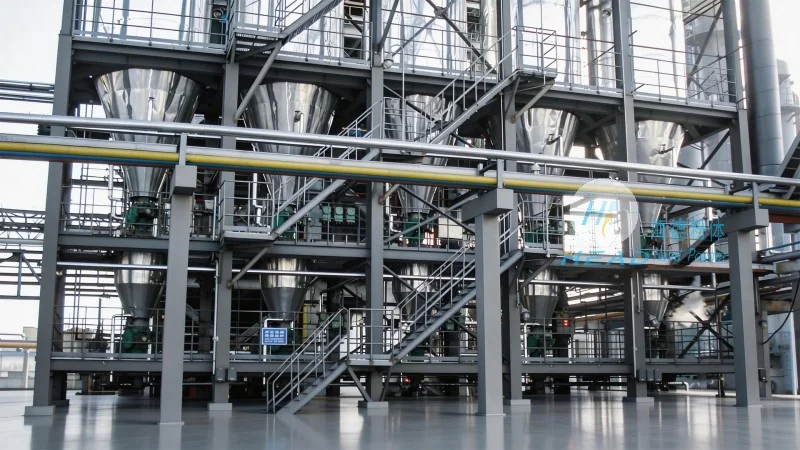
Sintered dust pneumatic conveying is a method of transporting fine particulate materials, such as sintered dust, through a pipeline using air or gas as the conveying medium. The core principle involves creating a pressure differential within the system to move the material from the source to the destination. The process typically includes several key components: a dust feeder, a conveying pipeline, a separator, and a receiver. The dust feeder ensures a consistent flow of material into the pipeline, while the conveying pipeline transports the material using air pressure. The separator then separates the material from the air stream, and the receiver collects the processed dust. This system leverages the principles of fluid dynamics and particle mechanics to achieve efficient and reliable material transport.
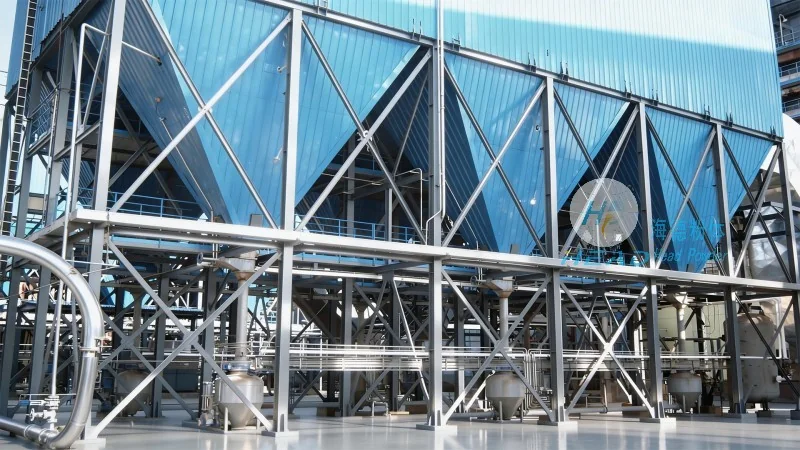
Sintered dust pneumatic conveying systems can be classified based on several factors, including the type of air flow, the pressure level, and the application requirements. The primary classifications include positive pressure systems, negative pressure systems, and hybrid systems. Positive pressure systems operate by blowing air into the pipeline, pushing the material forward. Negative pressure systems, on the other hand, draw air and material out of the pipeline, creating a vacuum. Hybrid systems combine elements of both positive and negative pressure to optimize performance for specific applications. Additionally, systems can be categorized by the conveying medium, such as air, nitrogen, or other gases, and by the particle size and density of the sintered dust being transported. Each classification has distinct advantages and is suitable for different operational scenarios, allowing for tailored solutions to meet specific industry needs.
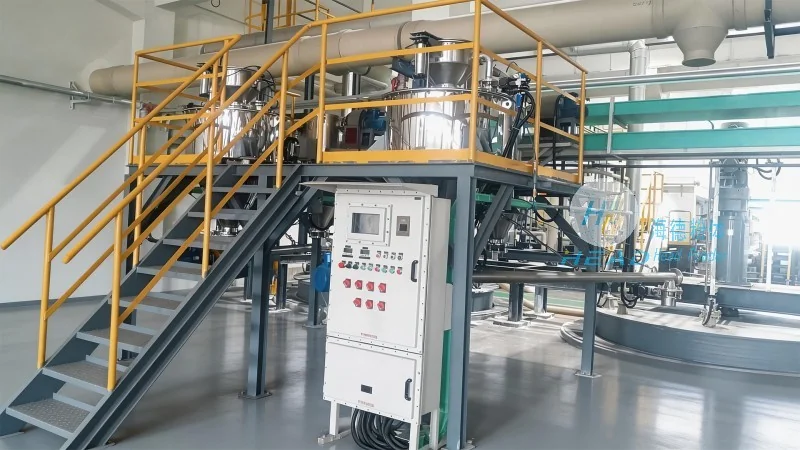
The application of sintered dust pneumatic conveying spans various industries, including steel production, cement manufacturing, and mineral processing. In steel plants, it is commonly used to transport sintered ore, a crucial raw material for ironmaking, from storage facilities to blast furnaces. The system ensures a continuous and efficient supply of raw material, enhancing production efficiency and reducing downtime. In cement plants, sintered dust is often used as a secondary raw material, and pneumatic conveying facilitates its transport from storage silos to the cement grinding mills. This method minimizes material loss and contamination, maintaining product quality. In mineral processing, the system is employed to handle fine sintered dust from processing operations, transporting it to disposal or recycling facilities. The versatility of sintered dust pneumatic conveying makes it an essential technology for optimizing material handling in these and other industrial sectors.
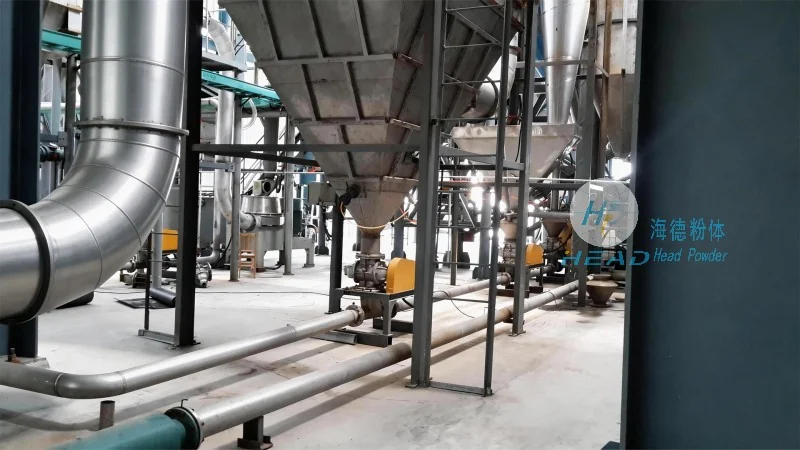
Implementing sintered dust pneumatic conveying offers several advantages, including high transport efficiency, reduced material degradation, and lower maintenance costs compared to traditional methods like belt conveyors. The system minimizes material exposure to external contaminants, preserving product quality and reducing waste. Additionally, it allows for flexible and compact system layouts, making it suitable for space-constrained industrial environments. However, there are also considerations to keep in mind, such as the need for proper air filtration to prevent dust accumulation and ensure compliance with environmental regulations. The system's performance is also influenced by factors like particle size distribution, moisture content, and air pressure, which must be carefully managed to achieve optimal results. Proper system design and maintenance are critical to maximizing the benefits and minimizing potential issues in sintered dust pneumatic conveying applications.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top