For industrial applications requiring the efficient and safe handling of copper sulfate, specialized conveying systems are essential. This article provides an overview of copper sulfate conveying systems, focusing on the benefits and characteristics of pneumatic conveying technology. The discussion will cover key aspects such as system design, operational advantages, and the role of advanced engineering solutions in optimizing material transport processes.
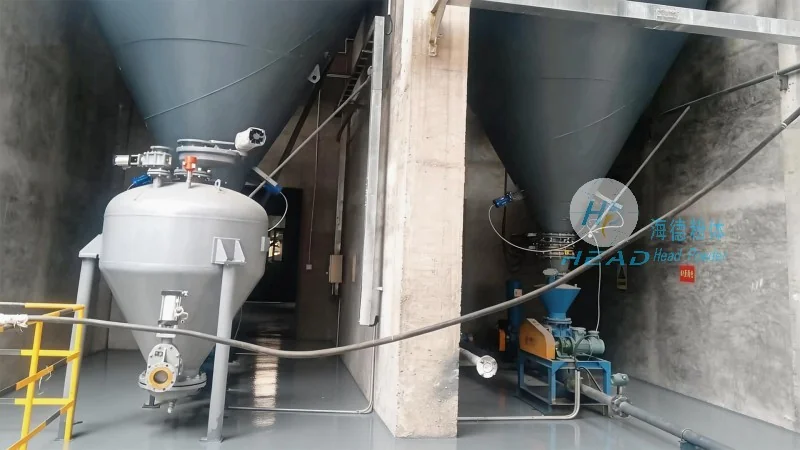
Copper sulfate conveying systems are engineered to transport copper sulfate powder or granules from storage to processing or packaging areas. These systems typically consist of several critical components, including a hopper for material storage, a feeder to control the flow rate, a conveying line (often equipped with air ducts), and a receiver for the material at the destination. The design of the system is tailored to the specific characteristics of copper sulfate, such as its density, moisture content, and potential for dust generation, ensuring optimal performance and safety.
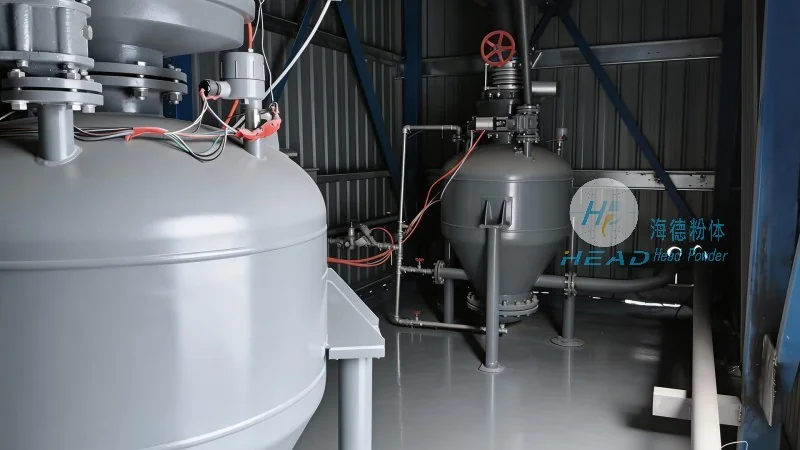
Pneumatic conveying is a preferred method for copper sulfate transport due to its ability to handle fine powders and granules efficiently. Unlike mechanical systems, which may cause material degradation or contamination, pneumatic systems use air pressure to move material through a sealed pipeline. This approach offers several key advantages, including high transport efficiency, reduced risk of product contamination, and the ability to handle materials in a dust-free environment. Additionally, pneumatic conveying systems can be designed for both low and high-pressure applications, making them adaptable to various industrial settings.
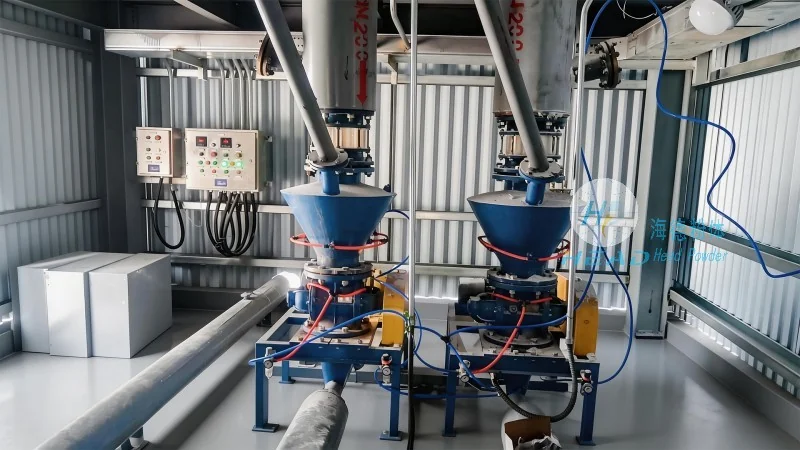
The adoption of pneumatic conveying for copper sulfate transport brings significant operational benefits. One of the most notable is the reduction in labor costs associated with manual handling, as the system automates the material movement process. This automation also minimizes the risk of human error and workplace accidents, enhancing overall safety. Furthermore, the sealed nature of pneumatic systems prevents dust exposure, which is crucial for maintaining a safe working environment and complying with occupational health regulations. The energy efficiency of modern pneumatic conveying systems also contributes to lower operational costs over time.
HeadPowder, a leading provider of industrial conveying solutions, understands that each copper sulfate processing facility has unique requirements. Therefore, their systems are designed with customization in mind. Whether a facility needs a small-scale system for laboratory use or a large-scale system for bulk production, HeadPowder can tailor the conveying solution to meet specific throughput, distance, and material handling needs. The company’s engineering team works closely with clients to assess operational parameters and recommend the most suitable conveying technology, ensuring optimal performance and cost-effectiveness.
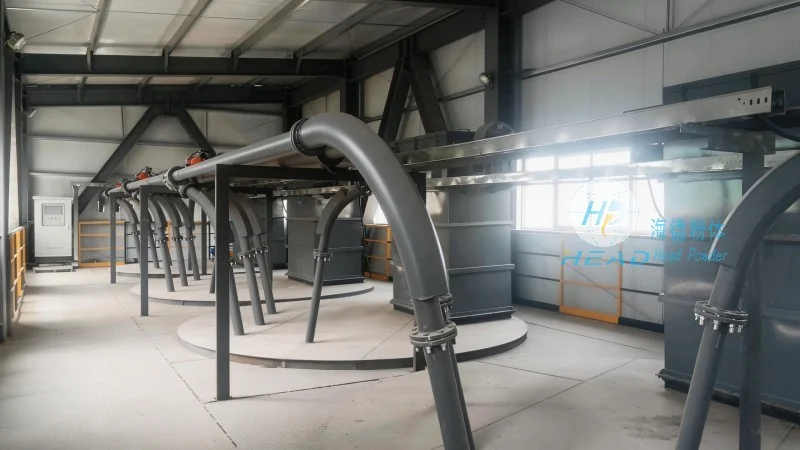
HeadPowder, or Shandong HeadPowder Engineering Co., Ltd., is a professional manufacturer and supplier of industrial conveying equipment based in Shandong, China. With years of experience in the field, the company specializes in developing and manufacturing high-quality copper sulfate conveying systems and other material handling solutions. HeadPowder’s commitment to quality and innovation has earned them a reputation for reliability and customer satisfaction in the industry. The company’s facilities are equipped with advanced manufacturing technologies and rigorous quality control processes to ensure that every product meets the highest standards. HeadPowder’s location in Shandong, China, allows them to leverage local resources and expertise while providing global clients with efficient and cost-effective solutions.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top