Phosphorus pentoxide (P₂O₅) is a critical chemical widely used in various industrial applications, including the production of phosphoric acid, flame retardants, and specialty chemicals. The efficient and safe transportation of this hazardous material is paramount for industrial operations. This article provides an in-depth analysis of pneumatic conveying systems designed for the handling of phosphorus pentoxide, focusing on the technical aspects, operational considerations, and industry best practices.
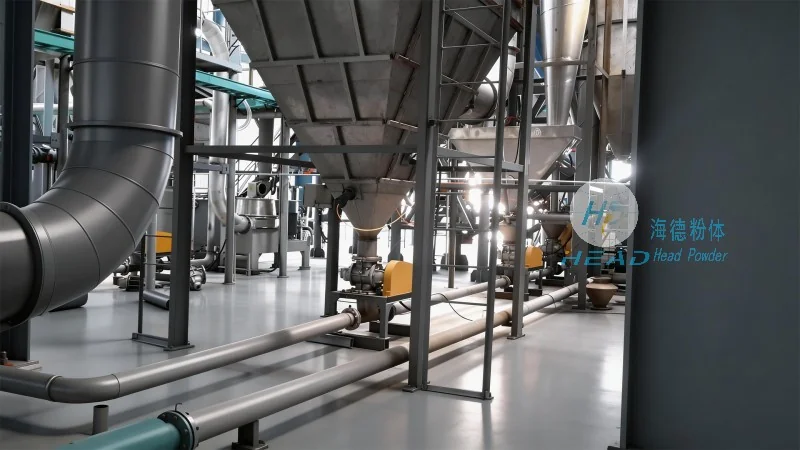
Phosphorus pentoxide is a highly reactive and hygroscopic substance that requires specialized equipment for safe and reliable transport. Pneumatic conveying systems offer a solution by utilizing air or other gases to move the material through a pipeline network. These systems are particularly suitable for phosphorus pentoxide due to their ability to handle fine powders and minimize material contact with equipment surfaces, reducing the risk of contamination and equipment corrosion.
The core components of a pneumatic conveying system for phosphorus pentoxide typically include a material feed hopper, a rotary valve or feeder, a conveying pipeline, a dust collector or filter system, and a receiving hopper or storage tank. The material feed hopper is designed to store and meter the phosphorus pentoxide, ensuring a consistent flow rate. The rotary valve or feeder controls the discharge of the material into the conveying pipeline, preventing air leakage and maintaining system pressure. The conveying pipeline is usually made of corrosion-resistant materials such as stainless steel or special alloys to withstand the chemical properties of phosphorus pentoxide. The dust collector or filter system is essential for capturing any airborne particles, ensuring compliance with environmental regulations and maintaining air quality. The receiving hopper or storage tank collects the material at the destination, allowing for further processing or storage.
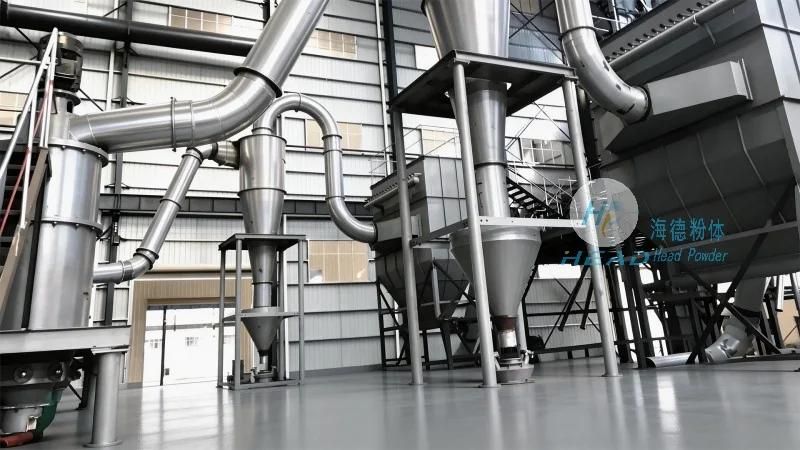
The operation of a pneumatic conveying system for phosphorus pentoxide is based on the principle of air flow and pressure differentials. There are two main types of pneumatic conveying systems: pressure and vacuum. Pressure systems use compressed air to push the material through the pipeline, while vacuum systems use a vacuum pump to draw the material into the pipeline. The choice between pressure and vacuum systems depends on factors such as the distance of transport, the material's characteristics, and the system's capacity. System design considerations include the selection of appropriate air velocities to prevent material settling or blockages, the sizing of the pipeline and components to handle the material's flow rate, and the implementation of safety features such as pressure relief valves and explosion-proof designs. Additionally, the system must be equipped with proper ventilation and dust control measures to protect personnel and the environment from exposure to phosphorus pentoxide dust.
Compared to traditional methods like bucket elevators or belt conveyors, pneumatic conveying systems offer several advantages for handling phosphorus pentoxide. These include reduced material degradation due to minimal contact with equipment, lower risk of contamination from external sources, and improved safety through enclosed systems. Pneumatic conveying also allows for flexible system layouts, enabling the integration of multiple feeding and receiving points. The systems are highly efficient in terms of energy consumption and can handle high volumes of material with minimal labor requirements. Furthermore, pneumatic conveying systems can be easily scaled up or down to accommodate changes in production needs, providing flexibility for industrial operations.
Phosphorus pentoxide pneumatic conveying systems are widely used in various industries that rely on phosphorus-based chemicals. These include the fertilizer industry, where phosphorus pentoxide is used to produce phosphoric acid, a key component in fertilizer production. The chemical industry also utilizes these systems for the manufacturing of flame retardants, plasticizers, and other specialty chemicals. Additionally, the pharmaceutical and food processing industries may use phosphorus pentoxide in the production of certain additives or ingredients. The systems are also employed in research and development laboratories for the handling of small quantities of phosphorus pentoxide in experimental processes.
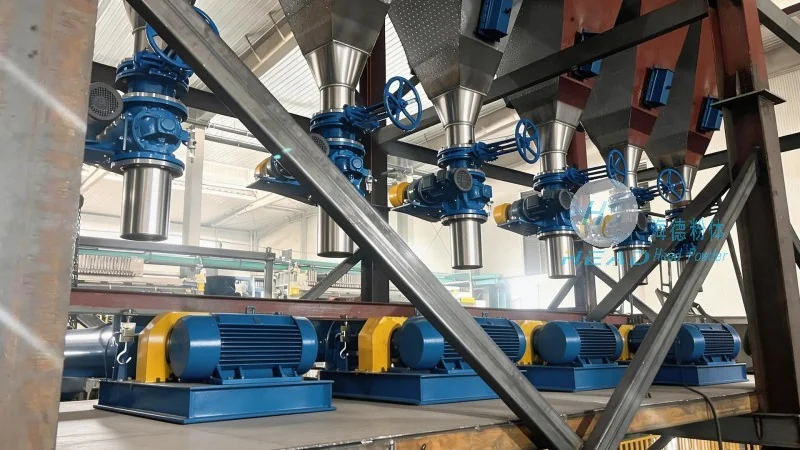
Shandong HeadPowder Engineering Co., Ltd., a leading provider of industrial conveying solutions, specializes in designing and manufacturing pneumatic conveying systems tailored to the unique needs of phosphorus pentoxide handling. With years of experience in the field, HeadPowder has developed advanced systems that incorporate the latest technologies to ensure optimal performance and safety. The company's systems are designed to meet the stringent requirements of the chemical industry, including compliance with environmental regulations and safety standards. HeadPowder's expertise lies in customizing the system components, such as the material feeders and pipeline materials, to withstand the corrosive properties of phosphorus pentoxide. The company also provides comprehensive support, including installation, maintenance, and technical assistance, to ensure the long-term reliability of the conveying systems.
Pneumatic conveying systems play a crucial role in the efficient and safe handling of phosphorus pentoxide, a vital chemical in modern industry. As industrial processes continue to evolve, the demand for advanced conveying solutions will increase. Future trends in phosphorus pentoxide pneumatic conveying systems may include the integration of automation and control systems for real-time monitoring and optimization, the use of more durable and corrosion-resistant materials, and the development of more energy-efficient designs. Despite these advancements, the core principles of safe and reliable material transport remain unchanged. By adhering to industry best practices and leveraging the expertise of companies like Shandong HeadPowder Engineering Co., Ltd., industries can ensure the continued safe and efficient handling of phosphorus pentoxide, supporting the growth of various sectors that rely on this essential chemical.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top