HeadPowder, a leading enterprise in the field of pneumatic conveying technology, specializes in the design, manufacturing, and integration of advanced systems for handling nitrile rubber. This article provides a detailed overview of the classification and key components of nitrile rubber pneumatic conveying systems, highlighting the technical aspects and practical applications that define this critical equipment in industrial processes.
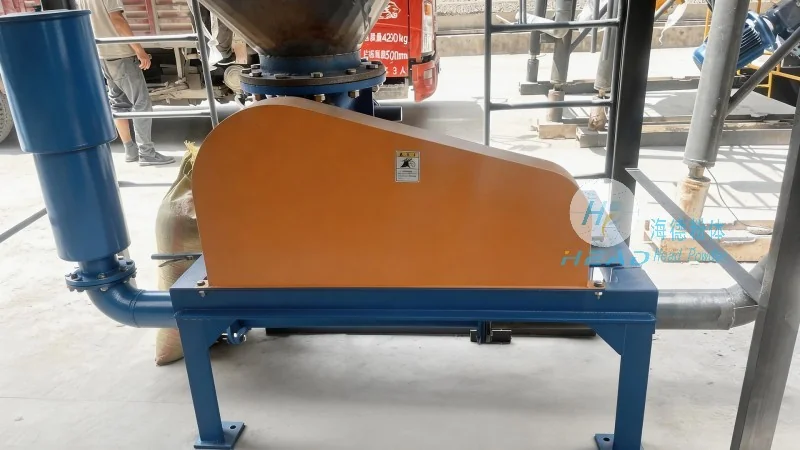
Nitrile rubber, also known as NBR, is a synthetic rubber with excellent resistance to oil, fuel, and chemicals, making it a preferred material in various industrial applications, including automotive, aerospace, and manufacturing sectors. Pneumatic conveying systems are essential for efficiently transporting nitrile rubber powders or granules from one location to another within a production facility. These systems utilize compressed air or other gases to move the material through a pipeline, offering advantages such as reduced contamination, improved safety, and enhanced process control compared to traditional mechanical conveying methods.
Nitrile rubber pneumatic conveying systems can be broadly classified based on the conveying principle and the pressure used. The primary categories include pressure systems, vacuum systems, and mixed systems. Pressure systems operate by introducing compressed air into the material stream, propelling the nitrile rubber through the pipeline. These systems are suitable for long-distance and high-volume conveying tasks. Vacuum systems, on the other hand, create a negative pressure environment to draw the material into the pipeline, often used for short-distance or low-volume applications. Mixed systems combine elements of both pressure and vacuum, offering flexibility for diverse operational requirements.
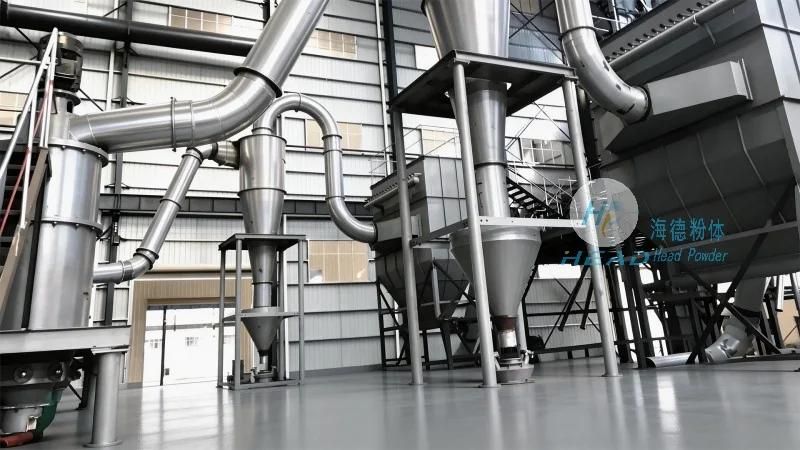
The effectiveness of a nitrile rubber pneumatic conveying system depends on several critical components that work in concert to ensure efficient material handling. The main components include the air compressor or vacuum pump, which provides the necessary pressure or vacuum; the material feed hopper, which stores and feeds the nitrile rubber into the system; the conveying pipeline, typically made of materials resistant to nitrile rubber and chemicals; the control valves and regulators, which manage the flow of air and material; and the dust collection or filtration system, which ensures compliance with environmental regulations and maintains air quality. Each component is carefully selected and integrated to optimize performance and durability in handling nitrile rubber.
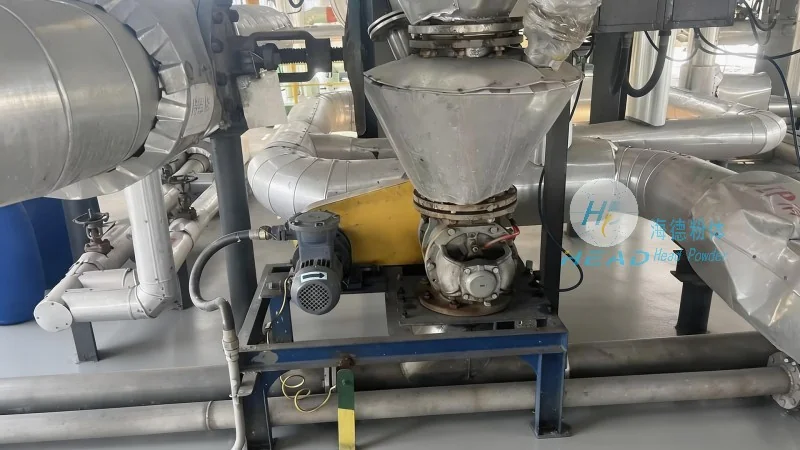
Nitrile rubber pneumatic conveying systems are widely used in industries where the material's chemical resistance and mechanical properties are crucial. Common applications include the transportation of nitrile rubber powders from storage silos to processing lines, the transfer of granules between mixing and extrusion equipment, and the handling of nitrile rubber in recycling or reprocessing operations. Operational considerations include the selection of appropriate pipeline materials to prevent degradation or contamination of the nitrile rubber, the maintenance of consistent air pressure to avoid material blockages or uneven flow, and the implementation of proper filtration to protect downstream equipment from dust and particulate matter. These factors are essential for ensuring the long-term reliability and efficiency of the system.
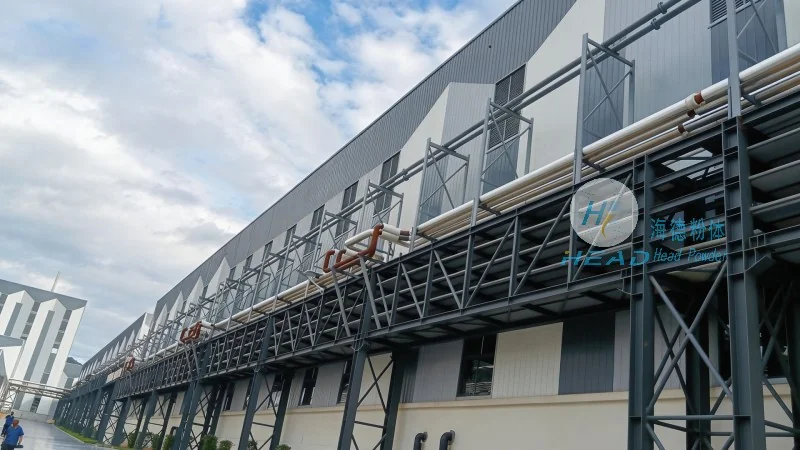
Compared to mechanical conveying methods, nitrile rubber pneumatic conveying systems offer several advantages, including reduced risk of material contamination, improved safety by eliminating the need for manual handling, and enhanced process control through precise flow regulation. However, these systems also present challenges, such as the need for regular maintenance of air compressors and filtration systems, potential for material buildup in pipelines, and the requirement for proper system design to prevent air leaks or pressure losses. Addressing these challenges through proper system design, regular maintenance, and quality control measures ensures that nitrile rubber pneumatic conveying systems deliver optimal performance and longevity.
Shandong HeadPowder Engineering Co., Ltd., with its headquarters in Shandong, China, is a reputable provider of nitrile rubber pneumatic conveying systems. The company leverages advanced engineering and manufacturing capabilities to develop customized solutions tailored to the specific needs of clients in various industries. By focusing on the classification and key components of these systems, HeadPowder ensures that its products meet the highest standards of efficiency, reliability, and safety, supporting the smooth operation of industrial processes that rely on nitrile rubber handling. With a commitment to innovation and quality, HeadPowder continues to be a trusted partner in the pneumatic conveying technology sector.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top