When it comes to the efficient handling and transportation of borax granules, specialized equipment plays a crucial role in industrial processes. This article delves into the specifics of borax granular material conveying equipment, exploring its design principles and the technology behind its operation.
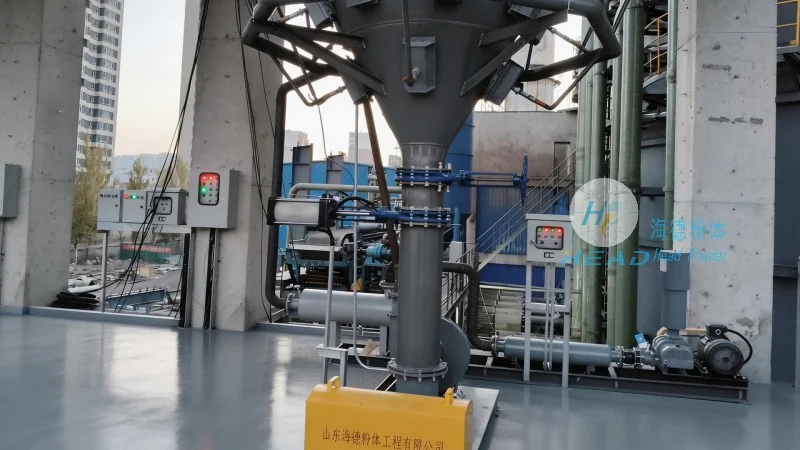
Borax granular material conveying equipment is a specialized system engineered to transport borax granules from one location to another within industrial settings. These systems are designed to handle the unique properties of borax granules, such as their size, density, and flow characteristics, ensuring reliable and efficient material movement. The equipment is commonly used in various industries, including chemical manufacturing, food processing, and pharmaceuticals, where the consistent and safe transport of borax granules is essential for production continuity.
The design of borax granular material conveying equipment is based on several key principles that ensure optimal performance and reliability. One of the primary principles is the adaptation to the physical characteristics of borax granules. Borax granules typically have a certain size range and density, which influences the choice of conveyor type and components. For instance, screw conveyors or belt conveyors may be selected based on the granule size and the required conveying distance. The design also considers the need for minimal material degradation and contamination, as borax is often used in applications where purity is critical.
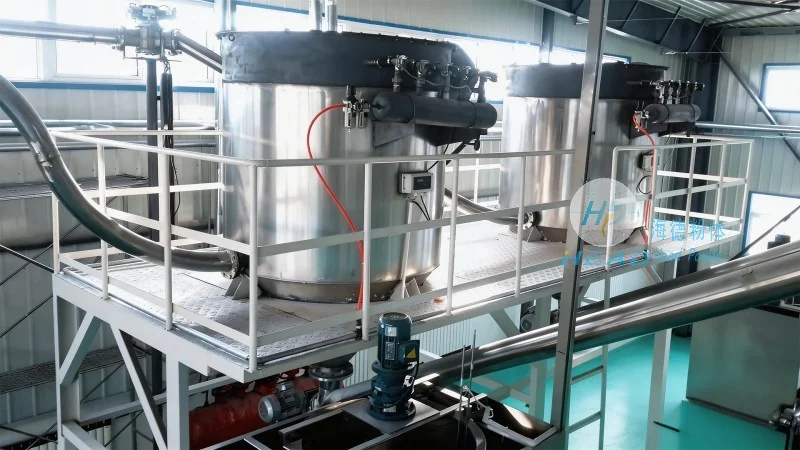
Another critical design principle is the integration of components that ensure smooth and continuous operation. This includes the selection of appropriate drive mechanisms, such as electric motors or gearboxes, to provide the necessary power for conveying. The system may also incorporate features like variable speed drives to adjust the conveying rate based on process requirements. Additionally, the design emphasizes durability and ease of maintenance, as industrial equipment must withstand continuous operation and potential wear from the material being conveyed.
Several key components make up a borax granular material conveying system, each playing a vital role in the overall operation. The feeding mechanism, often a hopper or a feeder, is responsible for introducing the borax granules into the conveyor system. This component must be designed to handle the flow characteristics of the granules, preventing blockages or uneven feeding. The conveyor itself, whether a screw, belt, or pneumatic conveyor, is the heart of the system, responsible for moving the material through the process. The screw conveyor, for example, uses a rotating screw to push the granules forward, while a belt conveyor relies on a moving belt to transport the material. The discharge mechanism, such as a discharge hopper or a valve, then releases the borax granules at the desired location.
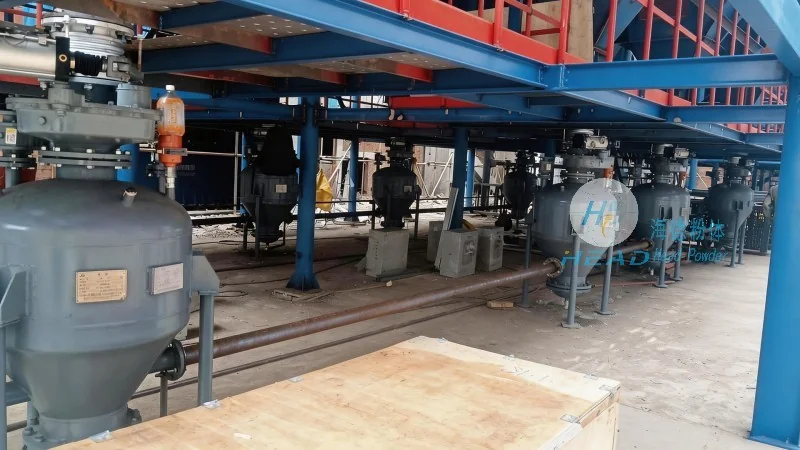
Control systems are also integral to the design, enabling operators to monitor and adjust the conveying process as needed. These systems may include sensors to detect the level of material in the hopper or the speed of the conveyor, providing real-time feedback to maintain optimal operation. The design also considers safety features, such as emergency stop buttons and protective guards, to ensure the safety of personnel operating the equipment.
Borax granular material conveying equipment is widely used in various industrial applications due to its efficiency and reliability. In chemical manufacturing, it is used to transport borax granules to reactors or storage tanks, ensuring a steady supply of raw material for production. In food processing, the equipment is used to convey borax granules for use in food products, where purity and consistent quality are paramount. The equipment also finds applications in pharmaceuticals, where the precise handling of borax granules is essential for drug formulation.
The benefits of using specialized borax granular material conveying equipment include improved efficiency in material handling, reduced labor costs, and enhanced safety in the workplace. The equipment minimizes the risk of material spillage or contamination, which can be costly and hazardous. Additionally, the design of the equipment ensures that the borax granules are handled gently, preserving their quality and preventing degradation. This is particularly important in industries where the quality of the final product is directly linked to the quality of the raw materials used.
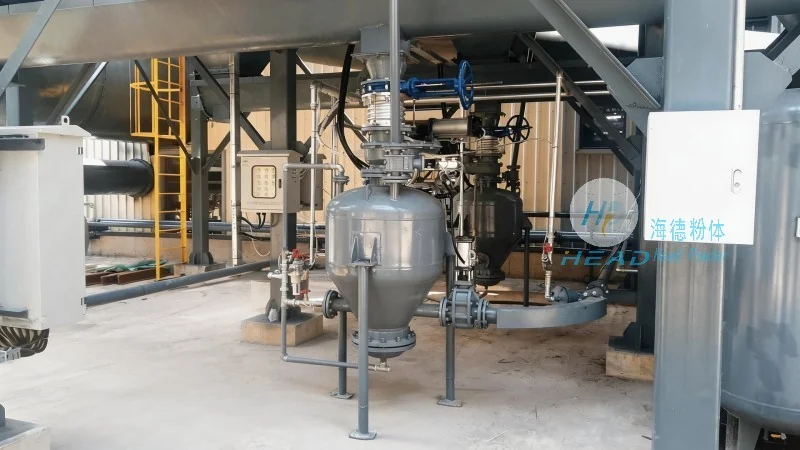
HeadPowder, or Shandong HeadPowder Engineering Co., Ltd., is a reputable company based in China, specializing in the design and manufacturing of material handling equipment. With a focus on innovation and quality, HeadPowder has established itself as a trusted provider of borax granular material conveying equipment and other industrial solutions. The company's expertise lies in understanding the unique requirements of different industries and tailoring equipment to meet those needs. HeadPowder's products are known for their durability, efficiency, and reliability, making them a preferred choice for businesses in need of reliable material handling solutions.
HeadPowder's commitment to customer satisfaction is evident in its comprehensive approach to equipment design and support. The company works closely with clients to understand their specific needs and provides customized solutions that address their unique challenges. Whether it's a new installation or the replacement of existing equipment, HeadPowder offers expert guidance and support throughout the process. The company's facilities are equipped with advanced technology and skilled personnel, ensuring that each piece of equipment is manufactured to the highest standards. HeadPowder's dedication to quality and customer service has earned it a strong reputation in the industry, making it a reliable partner for businesses seeking efficient and reliable material handling solutions.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top