When it comes to efficient handling and transportation of granular materials, especially in industrial applications, the use of specialized equipment is crucial. One such equipment is the ABS granular material conveying system, which plays a vital role in various manufacturing and processing industries. This article aims to explore what ABS granular material conveying equipment is and delve into its design principles, providing insights into its functionality and importance in modern industrial operations.
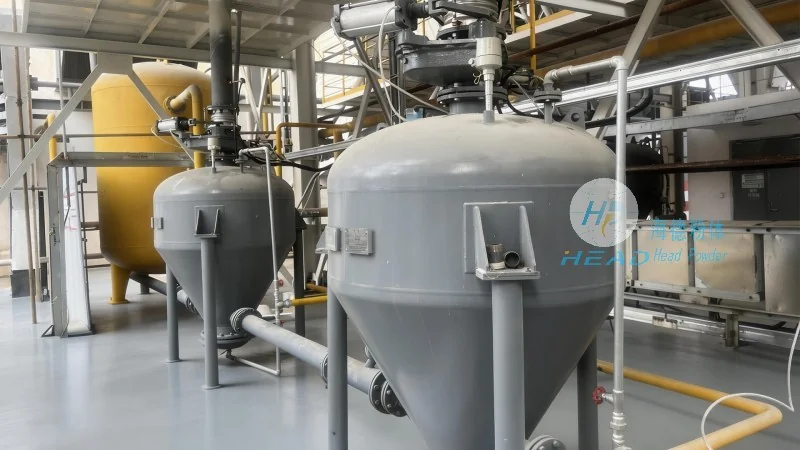
Understanding ABS Granular Material Conveying Equipment
ABS granular material conveying equipment refers to a range of machinery designed to transport and handle bulk granular materials, such as powders, pellets, or small particles. These materials can include chemicals, food products, pharmaceuticals, or industrial raw materials. The primary function of this equipment is to move these materials from one location to another within a production facility or between different stages of a process efficiently and reliably. The equipment is engineered to handle various types of granular materials, ensuring minimal loss, contamination, or degradation during the conveying process.
The Design Principles Behind ABS Conveying Systems
The design of ABS granular material conveying equipment is based on several key principles that ensure optimal performance, safety, and efficiency. These principles include material handling efficiency, system reliability, and adaptability to different operational conditions. Let's break down the core design considerations:
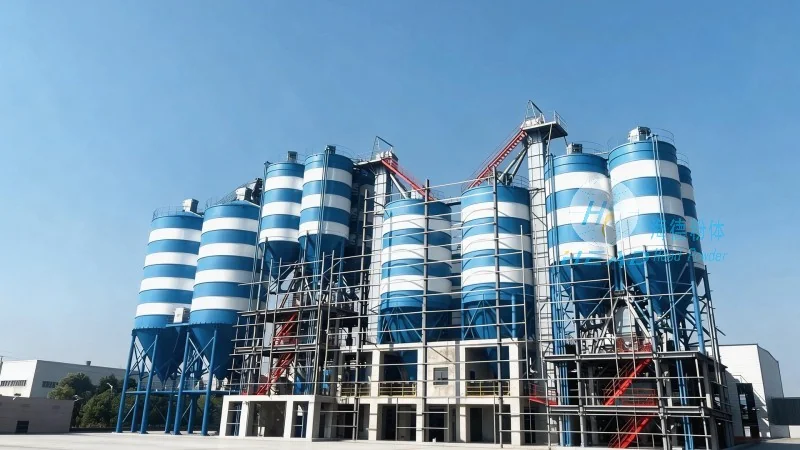
- Material Compatibility: The equipment is designed to handle a wide range of granular materials, from fine powders to larger pellets. The materials' properties, such as density, moisture content, and flow characteristics, are considered during the design phase to ensure the conveying system can accommodate them effectively.
- Flow Control and Uniformity: Maintaining consistent material flow is critical to prevent blockages or uneven distribution. The design incorporates features like hopper design, feed mechanisms, and flow control devices to ensure smooth and uniform material movement through the system.
- Energy Efficiency: Modern ABS conveying systems are designed with energy efficiency in mind. This includes optimizing motor selection, reducing friction in moving parts, and using advanced control systems to minimize energy consumption while maintaining high conveying rates.
- Safety and Reliability: Safety is a top priority in industrial equipment design. The ABS conveying system incorporates safety features such as overload protection, emergency stop mechanisms, and robust construction to ensure reliable operation and protect personnel and equipment.
Key Components of ABS Granular Material Conveying Equipment
ABS granular material conveying equipment typically consists of several key components that work together to achieve efficient material transport. These components include:
- Feed Hopper: The hopper is the initial component where granular materials are loaded. It is designed to store and feed the material into the conveying system, ensuring a consistent supply of material to the conveyor.
- Conveying Mechanism: This is the core part of the system responsible for moving the material. Common types of conveying mechanisms include screw conveyors, pneumatic conveyors, and belt conveyors, each with its own advantages and applications.
- Control System: The control system manages the operation of the conveying equipment, including start/stop functions, speed control, and monitoring of material flow. Advanced control systems may also include sensors to detect blockages or other issues.
- Discharge and Dosing Unit: The discharge unit is where the material is released from the conveying system. The dosing unit ensures accurate and controlled release of the material to the next stage of the process or for packaging.
Applications and Industries Using ABS Conveying Equipment
ABS granular material conveying equipment is widely used across various industries due to its versatility and efficiency. Some common applications include:
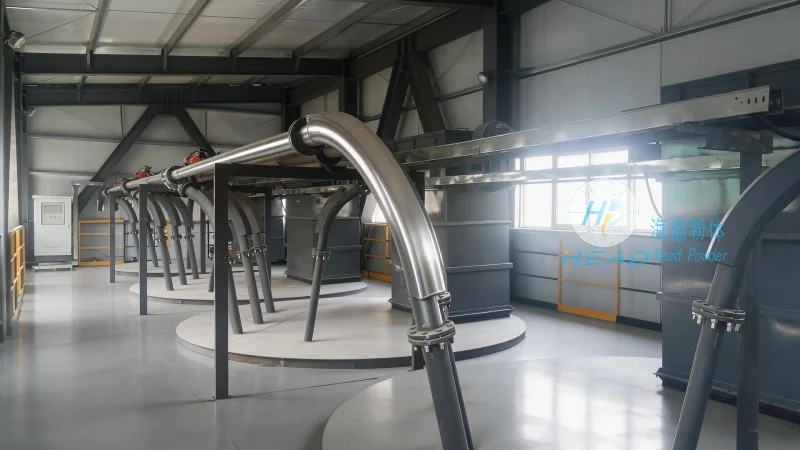
- Chemical Industry: Transporting chemical powders and pellets in manufacturing processes, ensuring safe and efficient handling.
- Food and Beverage Industry: Conveying food-grade powders, such as flour, sugar, or spices, in food processing plants.
- Pharmaceutical Industry: Handling pharmaceutical powders and granules in production lines, maintaining strict hygiene and contamination control.
- Plastic and Polymer Industry: Transporting plastic pellets and granules in manufacturing facilities, supporting the production of various plastic products.
Advantages of Using ABS Granular Material Conveying Equipment
Implementing ABS granular material conveying equipment offers several advantages for industrial operations:
- Increased Efficiency: The equipment enhances the overall efficiency of material handling processes, reducing downtime and improving production throughput.
- Reduced Labor Costs: Automated conveying systems minimize the need for manual labor in material transport, leading to cost savings and improved safety.
- Improved Product Quality: By ensuring consistent material flow and minimizing contamination, the equipment helps maintain product quality and meet regulatory standards.
- Space Efficiency: Modern conveying systems are designed to fit into limited spaces, making them suitable for compact industrial setups.
Conclusion
ABS granular material conveying equipment is a critical component in modern industrial operations, enabling efficient and reliable transport of bulk granular materials. The design principles behind these systems focus on material compatibility, flow control, energy efficiency, and safety. By understanding the functionality and advantages of ABS conveying equipment, industries can enhance their production processes, reduce costs, and improve overall operational efficiency. For businesses seeking to optimize their material handling processes, investing in high-quality ABS conveying systems is a strategic decision that can yield significant long-term benefits.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China
