Ammonium nitrate (AN) is a widely used industrial chemical, and its efficient and safe transportation is crucial for various industrial applications. Pneumatic conveying systems have become a preferred method for handling AN due to their ability to transport the material in a dust-free environment, reducing the risk of explosion and improving operational safety. This article provides an overview of the classification and key components of ammonium nitrate pneumatic conveying systems, highlighting the technical aspects and practical considerations for their design and implementation.
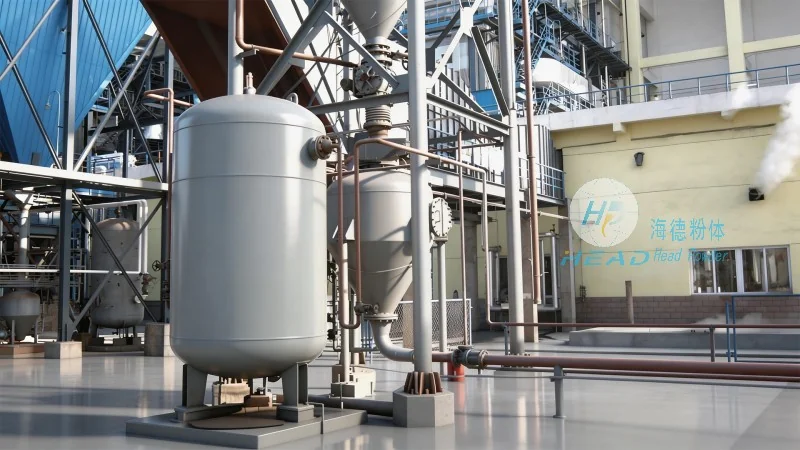
Ammonium nitrate is a highly reactive and potentially hazardous material, making the selection of an appropriate conveying system critical. Pneumatic conveying systems utilize air or other gases to transport bulk materials like AN through a pipeline network. These systems are designed to handle the specific properties of AN, including its granular nature, density, and potential for dust generation. The choice of system type and components depends on factors such as the distance of transport, the required flow rate, and the environmental regulations in the operating location.
Ammonium nitrate pneumatic conveying systems can be broadly classified into two main categories based on the direction of air flow and the method of material transport: aspiration (suction) systems and pressure (blowing) systems.
Aspiration systems operate by creating a negative pressure at the material intake point, drawing the AN into the pipeline using a vacuum source. This type of system is suitable for short to medium-distance transport, typically up to 100 meters, and is often used in applications where the material is stored in a hopper or silo near the processing plant. The key components of an aspiration system include a vacuum pump, a hopper with a feeder, a filter to capture any fine particles, and a discharge unit at the receiving end. The system works by pulling air and AN particles into the pipeline, where the air acts as a carrier medium. The material is then separated from the air at the discharge point, and the air is filtered before being released back into the environment.
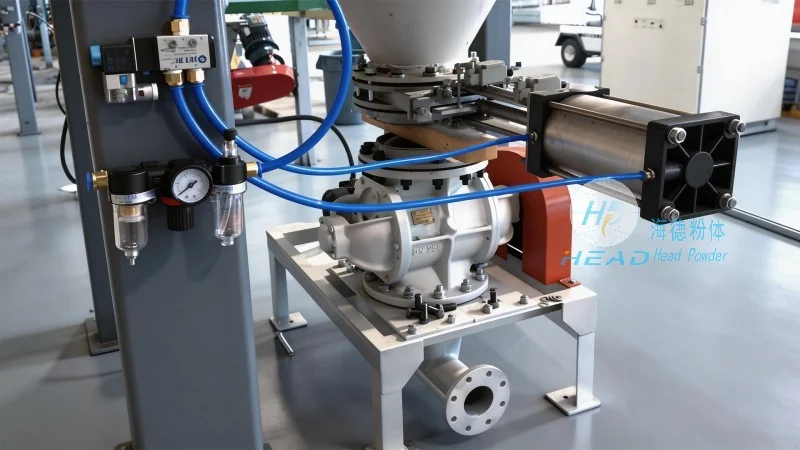
Pressure systems, on the other hand, use a positive pressure to push the AN through the pipeline. A blower or compressor generates the necessary pressure, and the material is fed into the pipeline using a feeder. This type of system is ideal for longer distances, up to several hundred meters, and can handle higher flow rates compared to aspiration systems. Pressure systems are commonly used in industrial settings where the AN is produced or stored at a central location and needs to be transported to multiple processing points. The components of a pressure system include a blower, a feeder, a pipeline network, and a receiving hopper with a dust collection system. The air is introduced at the feed end, and the AN particles are carried along the pipeline by the moving air, ensuring a continuous flow of material.
Regardless of the system type, ammonium nitrate pneumatic conveying systems consist of several critical components that work together to ensure efficient and safe operation. These components are designed to handle the specific characteristics of AN, such as its granular size, density, and potential for dust generation. The main components include:
The feeder and hopper are the initial components of the system, responsible for storing and feeding the ammonium nitrate into the pipeline. The hopper is typically made of corrosion-resistant materials, such as stainless steel or special alloys, to prevent the AN from reacting with the container and causing degradation. The feeder is designed to provide a consistent flow rate of AN, ensuring that the material is fed at a controlled rate into the pipeline. This is crucial to prevent blockages and maintain the system's efficiency. The feeder may include a rotary valve or a screw feeder, which can handle the granular nature of AN without causing excessive wear or dust generation.
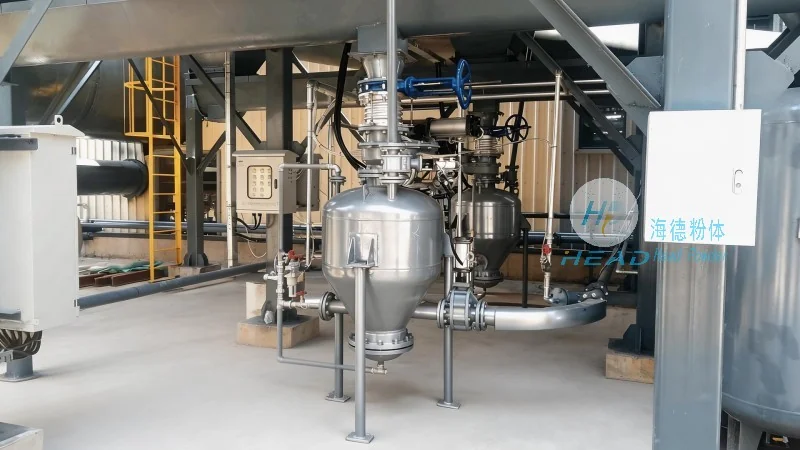
The air supply system is a critical component of both aspiration and pressure pneumatic conveying systems. In aspiration systems, a vacuum pump provides the necessary negative pressure to draw the AN into the pipeline. The vacuum pump is typically a rotary vane or a liquid ring pump, designed to handle the dust and moisture in the air. In pressure systems, a blower or compressor generates the positive pressure required to push the AN through the pipeline. The air supply system must be capable of delivering the required air volume and pressure to maintain the flow rate and prevent material buildup in the pipeline. The air is often filtered to remove any contaminants that could damage the system components or affect the quality of the AN.
The conveying pipeline is the main channel through which the ammonium nitrate is transported. The pipeline is typically made of stainless steel or other corrosion-resistant materials to withstand the chemical properties of AN and prevent corrosion over time. The diameter and length of the pipeline are determined based on the required flow rate and the distance of transport. The pipeline may include bends, elbows, and other fittings to direct the flow of material and air. To ensure smooth operation, the pipeline is often equipped with cleaning mechanisms, such as air cannons or sweepers, to remove any material buildup or blockages.
At the receiving end of the pneumatic conveying system, the ammonium nitrate is separated from the air carrier. This is typically done using a cyclone separator or a bag filter, which captures the AN particles and returns them to the receiving hopper. The air, now free of AN particles, is filtered to remove any remaining dust and then released back into the environment. The separation system is designed to handle the high velocity of the air and the density of the AN particles, ensuring that the material is efficiently collected and the air is clean. The collection system may include a dust collector or a baghouse filter, which can handle the dust generated during the conveying process.
The control and monitoring systems are essential for the safe and efficient operation of the ammonium nitrate pneumatic conveying system. These systems include sensors and controllers that monitor the pressure, flow rate, and temperature of the system. The sensors are typically installed at key points in the pipeline, such as the feeder, the pipeline, and the receiving hopper. The controllers use this data to adjust the air flow and feeding rate, ensuring that the system operates within safe limits. The control system may also include alarms and safety interlocks to prevent overpressure or other hazardous conditions. This helps to maintain the integrity of the system and protect the personnel operating it.
The design of an ammonium nitrate pneumatic conveying system requires careful consideration of several factors to ensure its effectiveness and safety. The system must be designed to handle the specific properties of AN, including its granular size, density, and potential for dust generation. The following are some of the key design considerations:

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top