Iron concentrate pneumatic conveying systems are critical in industrial operations for efficiently transporting iron ore concentrates. These systems utilize air or gas as the conveying medium to move bulk materials like iron concentrate from one location to another. The classification and composition of such systems are essential for understanding their functionality and application in various industrial settings.
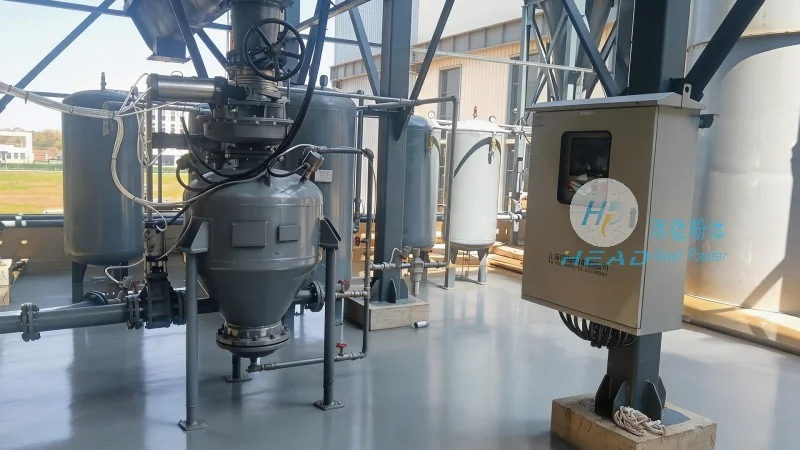
Iron concentrate pneumatic conveying systems can be classified based on several key factors, including the conveying medium, the pressure used, and the system design. The primary classifications include positive pressure systems, negative pressure (or vacuum) systems, and mixed pressure systems. Positive pressure systems use compressed air to push the material through the pipeline, making them suitable for long-distance and high-capacity transport. Negative pressure systems, on the other hand, use a vacuum to draw material into the system, which is ideal for handling fine powders and preventing dust emissions. Mixed pressure systems combine both approaches, offering flexibility in handling different material characteristics and system requirements.
The composition of an iron concentrate pneumatic conveying system involves several critical components that work together to ensure efficient material transport. The main components include the material feed hopper, which stores and feeds the iron concentrate into the system; the air compressor or vacuum pump, which provides the necessary pressure or vacuum; the conveying pipeline, which transports the material and air mixture; the separation equipment, such as cyclones or filters, which separates the material from the air; and the discharge equipment, which delivers the iron concentrate to the final destination. Each component plays a vital role in the overall performance and reliability of the system.
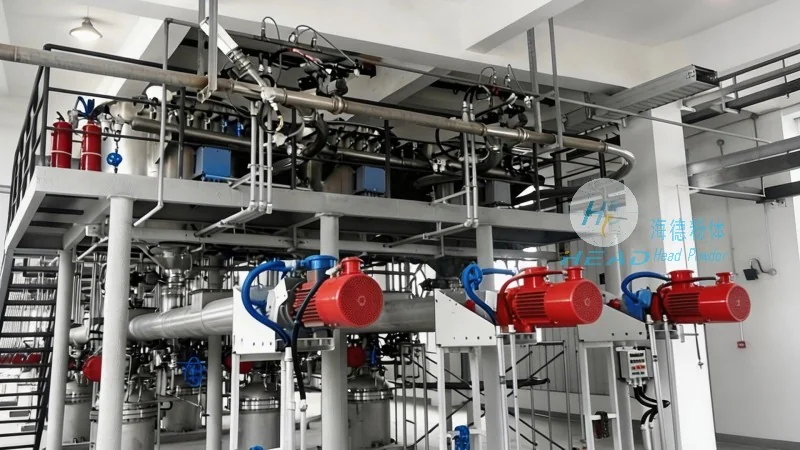
The material feed hopper is a crucial component in the iron concentrate pneumatic conveying system. It is designed to store a large quantity of iron concentrate and feed it into the system at a controlled rate. The hopper typically includes a feeder, such as a rotary valve or a screw feeder, which regulates the flow of material into the conveying line. This ensures consistent and uniform material feed, preventing blockages and maintaining system efficiency. The design of the hopper and feeder also considers factors like material flowability, moisture content, and dust control to minimize operational issues.
The air compressor or vacuum pump is responsible for generating the pressure or vacuum needed to convey the iron concentrate. In positive pressure systems, a high-pressure air compressor provides the necessary force to push the material through the pipeline. The compressor must be capable of delivering the required air volume and pressure to handle the material's density and pipeline length. In negative pressure systems, a vacuum pump creates a low-pressure environment that draws the material into the system. The choice of compressor or pump depends on the system's classification and the specific material being transported. Proper maintenance and sizing of the compressor or pump are essential to ensure optimal performance and minimize energy consumption.
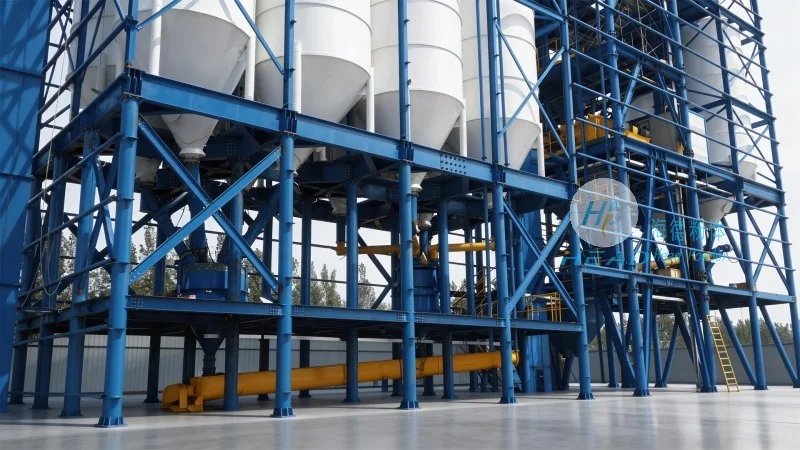
The conveying pipeline is a critical part of the iron concentrate pneumatic conveying system, as it carries the material and air mixture from the feed hopper to the discharge point. The pipeline is typically made of materials like stainless steel or plastic, which are resistant to corrosion and wear from the iron concentrate. The pipeline design includes various fittings, such as elbows, tees, and reducers, which direct the flow of material and air. The pipeline must be properly sized to accommodate the material's flow rate and the air velocity required for efficient transport. Proper installation and maintenance of the pipeline and fittings are essential to prevent leaks, blockages, and system inefficiencies.
Separation equipment, such as cyclones or filters, is used to separate the iron concentrate from the air in the conveying system. The cyclone separator uses centrifugal force to separate the material from the air, while the filter removes fine particles and dust from the air stream. The choice of separation equipment depends on the material's particle size, moisture content, and the required air quality. Proper operation and maintenance of the separation equipment are crucial to ensure that the iron concentrate is delivered in a clean and dry state, and that the air is discharged without excessive dust emissions.
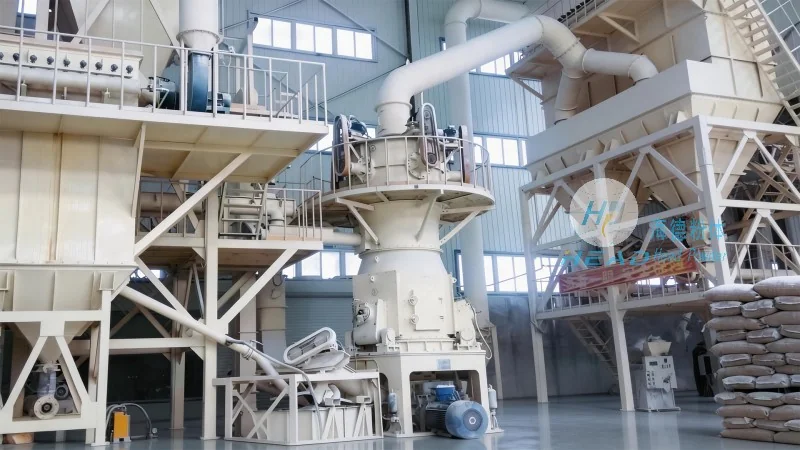
The discharge equipment is responsible for delivering the iron concentrate from the conveying system to the final destination. This can include a discharge hopper, a rotary valve, or a screw conveyor, depending on the application. The discharge equipment must be designed to handle the material's characteristics, such as its density and flowability, and to prevent blockages or spillage. Proper sizing and maintenance of the discharge equipment are essential to ensure smooth and efficient material delivery.
The integration of all components in an iron concentrate pneumatic conveying system is critical for its overall performance. The system typically includes control panels and sensors that monitor key parameters, such as pressure, flow rate, and material level. These controls allow for automatic operation and adjustment of the system, ensuring optimal performance and minimizing downtime. Proper integration and control of the system components are essential to maintain efficiency, reliability, and safety in the operation of the iron concentrate pneumatic conveying system.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top