HeadPowder, a leading enterprise in the field of material handling solutions, specializes in the design, manufacturing, and installation of advanced pneumatic conveying systems for various industrial applications. This article provides a detailed overview of the classification and key components of borax pneumatic conveying systems, highlighting the technical aspects and practical applications that define these efficient material transport solutions.
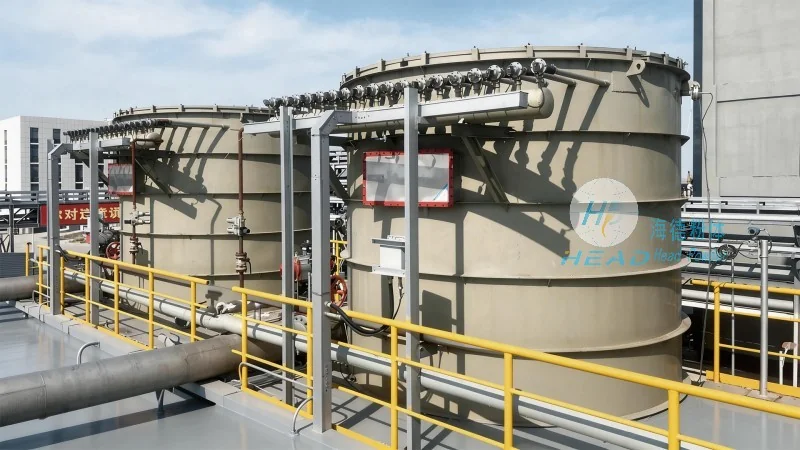
Borax, a widely used chemical compound in industries such as glass manufacturing, detergents, and pharmaceuticals, requires reliable and efficient transportation methods to ensure smooth production processes. Pneumatic conveying systems offer a solution by utilizing air pressure to move bulk materials like borax from one location to another. These systems are designed to handle the specific properties of borax, including its particle size, moisture content, and flow characteristics, while maintaining high levels of efficiency and safety.
Borax pneumatic conveying systems can be classified based on several key factors, including the conveying principle, system configuration, and application requirements. The primary classifications include:
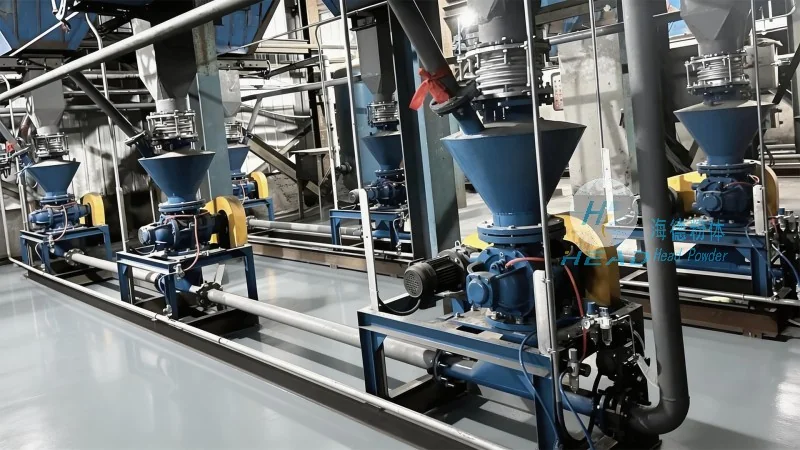
Each classification has its own advantages and is selected based on the specific operational needs of the borax handling facility. The choice of system type directly impacts the efficiency, cost, and maintenance requirements of the overall material transport process.
The effectiveness of a borax pneumatic conveying system depends on the integration of several critical components, each playing a vital role in the material transport process. The main components include:
The successful implementation of a borax pneumatic conveying system requires careful consideration of several factors, including the material's physical properties, the conveying distance, and the required flow rate. For example, the particle size and moisture content of borax can affect the system's performance, as larger or more moist particles may require higher air velocities or different feeder designs. Additionally, the distance between the feed and discharge points influences the choice of system type, with longer distances often necessitating negative pressure systems or more powerful PCUs.
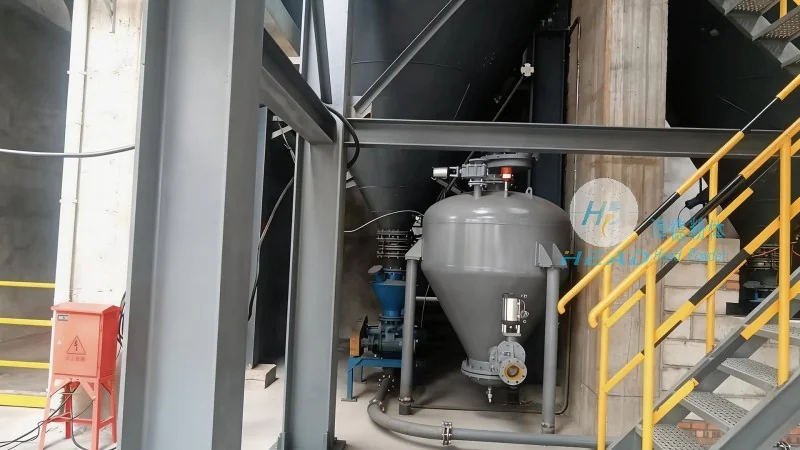
HeadPowder, with its extensive experience in material handling solutions, provides customized borax pneumatic conveying systems tailored to the specific needs of each client. Our team of engineers works closely with clients to assess their operational requirements, material characteristics, and site conditions to design and install systems that maximize efficiency, reduce costs, and ensure long-term reliability.
Borax pneumatic conveying systems are essential for efficient and safe material transport in industries that rely on borax. By understanding the classification and key components of these systems, businesses can select the most appropriate solution for their needs. HeadPowder, as a trusted provider of material handling solutions, continues to innovate and provide advanced systems that meet the evolving demands of the industry, ensuring that borax is transported effectively and reliably from source to destination.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top