Protein powder, a critical component in the food and supplement industries, requires reliable and efficient handling systems to maintain product quality and operational efficiency. Pneumatic conveying offers a solution that leverages air flow to transport powdered materials like protein powder, ensuring minimal product degradation and optimal process performance. This article explores the principles and applications of pneumatic conveying for protein powder, highlighting how it can enhance material handling in industrial settings.
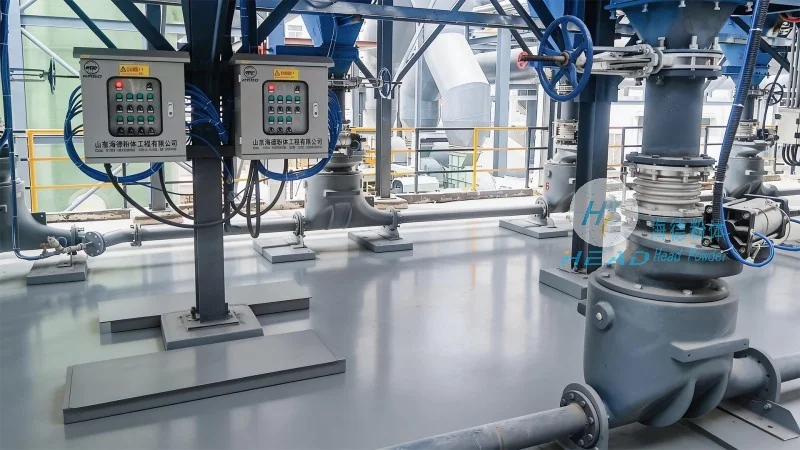
Pneumatic conveying systems use air pressure or vacuum to move powder particles through a pipeline. For protein powder, which is often sensitive to moisture and temperature changes, the choice of system design is crucial. There are two main types: pressure and vacuum systems. Pressure systems use compressed air to push material forward, while vacuum systems use a vacuum to draw material into the pipeline. Each type has advantages depending on the application, such as the distance to be covered and the material's characteristics. The system must be designed to handle the specific properties of protein powder, including its flowability, moisture content, and potential for caking, to ensure smooth and continuous operation.
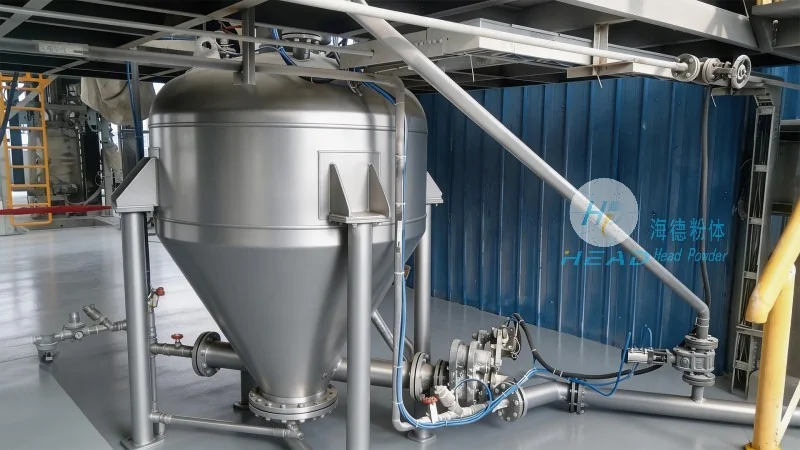
Effective pneumatic conveying for protein powder relies on several key components that work together to ensure efficient material transport. These include the hopper or feeder, which provides a consistent feed of powder; the conveyor line, which is typically made of materials resistant to corrosion and contamination, such as stainless steel; and the air compressor or vacuum pump, which generates the necessary pressure or vacuum. Additionally, filters and cyclones are used to separate the powder from the air stream, preventing product loss and maintaining air quality. The control system, which monitors pressure, flow, and other parameters, plays a vital role in maintaining the system's performance and preventing issues like blockages or overloading.
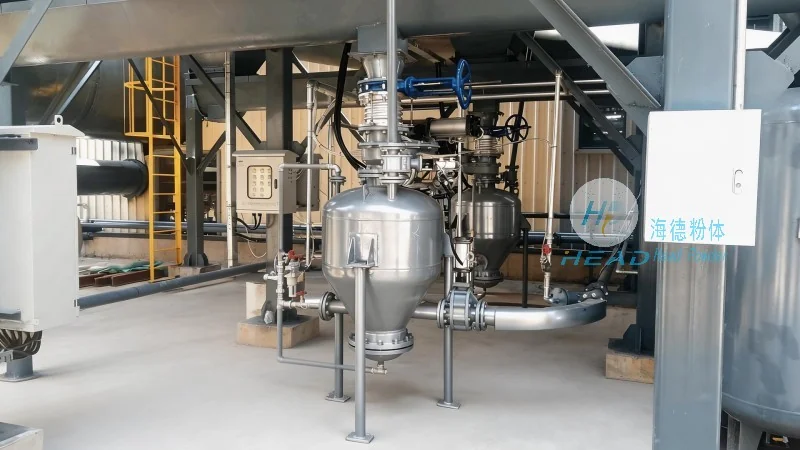
Implementing a pneumatic conveying system for protein powder offers several benefits that improve overall operational efficiency and product quality. One of the primary advantages is the ability to transport material over long distances without the need for multiple transfer points, reducing the risk of contamination and product degradation. The system also minimizes product handling, which is essential for maintaining the purity and nutritional value of protein powder. Furthermore, pneumatic conveying can be integrated with other processing equipment, such as mixers and blenders, to create a seamless production line. This integration improves workflow and reduces downtime, leading to increased productivity. Another benefit is the reduced need for manual labor, as the system can operate continuously with minimal supervision, enhancing safety and operational consistency.
Pneumatic conveying systems are widely used in the protein powder industry for various applications. For example, in large-scale production facilities, these systems are used to transport raw protein powder from storage silos to processing equipment, such as extruders or mixers. In supplement manufacturing, pneumatic conveying is used to move finished protein powder products from packaging lines to storage areas or distribution centers. The system's ability to handle different powder types, including whey, soy, and casein protein powders, makes it versatile for various production needs. Additionally, in research and development settings, pneumatic conveying is used to transport small batches of protein powder for testing and quality control, ensuring accurate and consistent results.
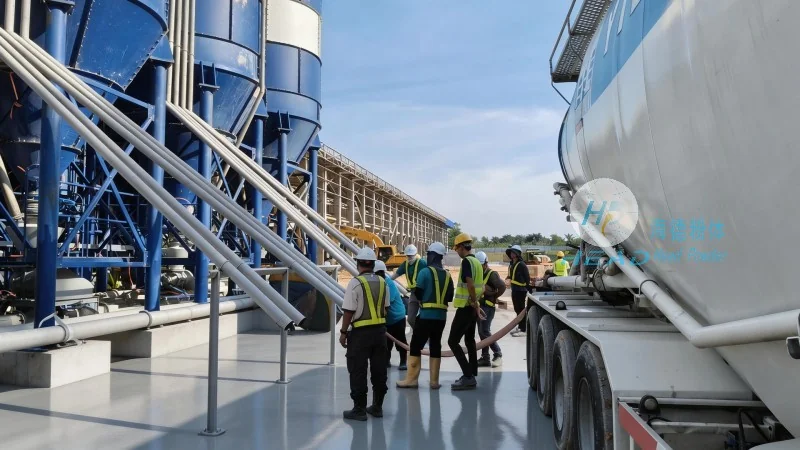
When selecting a pneumatic conveying system for protein powder, several factors must be considered to ensure optimal performance and cost-effectiveness. First, the system must be designed to handle the specific properties of the protein powder, such as its flowability and moisture content. The material of construction is also critical, as it must be resistant to corrosion and contamination from the powder. The system's capacity and the distance to be covered are other important considerations, as these affect the size and type of components required. Additionally, the system's energy efficiency and maintenance requirements should be evaluated to ensure long-term operational costs are manageable. Consulting with a professional, such as Shandong HeadPowder Engineering Co., Ltd., which specializes in protein powder handling systems, can provide valuable guidance in selecting the right system for your specific needs.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top