HeadPowder, a leading enterprise in the field of material handling solutions, specializes in the design, manufacturing, and supply of advanced pneumatic conveying systems. This article provides an overview of the powder electrolyte pneumatic conveying line, focusing on its structural components and operational principles. The company, based in Shandong, China, leverages decades of industry experience to deliver efficient and reliable systems tailored to the needs of various industrial applications.
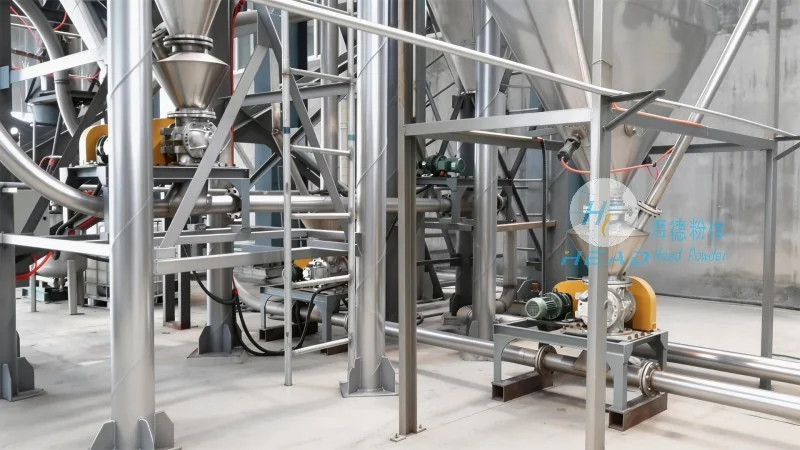
The powder electrolyte pneumatic conveying system is a sophisticated piece of equipment engineered to transport fine powders, such as electrolytes used in battery manufacturing, with precision and efficiency. At its heart are several key components that work in tandem to ensure smooth operation. The system typically includes a hopper for material storage, a feeder to control the flow rate, a conveying line (often equipped with cyclones or filters for separation), and a receiver for the discharged material. Each component plays a critical role in maintaining the integrity of the powder and optimizing the conveying process.
The operation of the powder electrolyte pneumatic conveying line relies on the principles of pneumatic transport, where air is used as the medium to move the material. The process begins with the material being fed from the hopper into the conveying line. As air is introduced, it creates a flow that lifts and transports the powder particles through the system. The system may employ positive pressure or negative pressure (suction) methods, depending on the specific requirements of the application. Positive pressure systems use blowers to force air and material through the line, while negative pressure systems use vacuum pumps to draw material into the line. The choice of method depends on factors like the material's properties, the distance to be conveyed, and the desired flow rate.
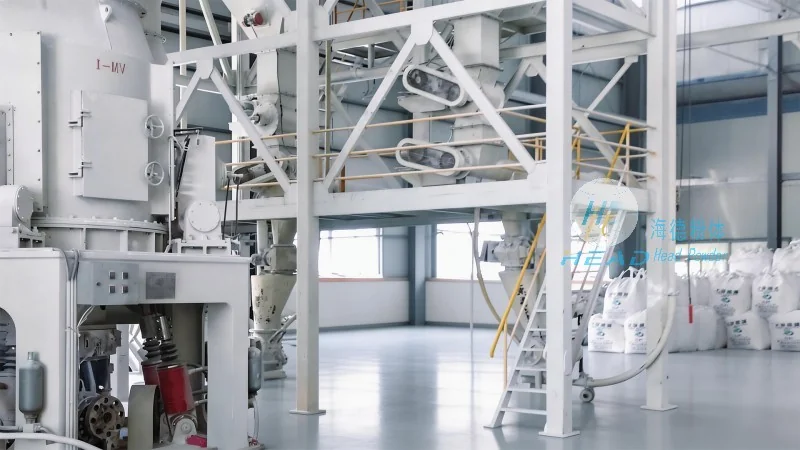
HeadPowder's engineers have designed the powder electrolyte pneumatic conveying system with a focus on durability, efficiency, and safety. The system's structure incorporates high-quality materials, such as stainless steel, to resist corrosion and ensure long-term performance, which is particularly important when handling electrolytes that may be chemically active. The hopper and feeder are designed to minimize material degradation and prevent caking, while the conveying line is equipped with features like cyclones to separate any entrained air or dust, maintaining the purity of the powder. The receiver is designed to safely collect the material, preventing spillage and ensuring a clean operation. The entire system is engineered to meet stringent industry standards, ensuring compliance with safety and environmental regulations.
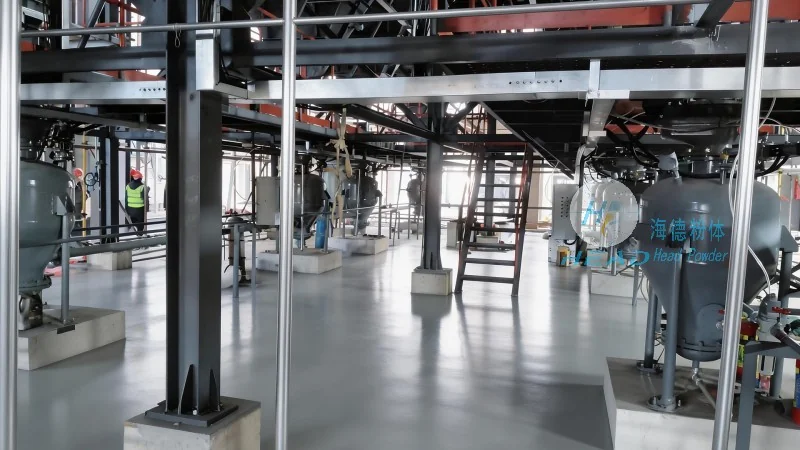
Implementing a pneumatic conveying system for powder electrolytes offers several advantages over traditional methods like bucket elevators or belt conveyors. One of the primary benefits is the ability to transport materials in a closed system, which minimizes dust emissions and improves workplace safety. This is crucial in industries where powder handling is a common practice, as it reduces the risk of respiratory issues and contamination. Additionally, the system allows for precise control over the flow rate, ensuring consistent material delivery to downstream processes. The closed-loop design also helps maintain the quality of the powder, preventing exposure to moisture or contaminants that could affect its performance. Furthermore, the system is compact and can be integrated into existing production lines, reducing the need for extensive infrastructure changes.
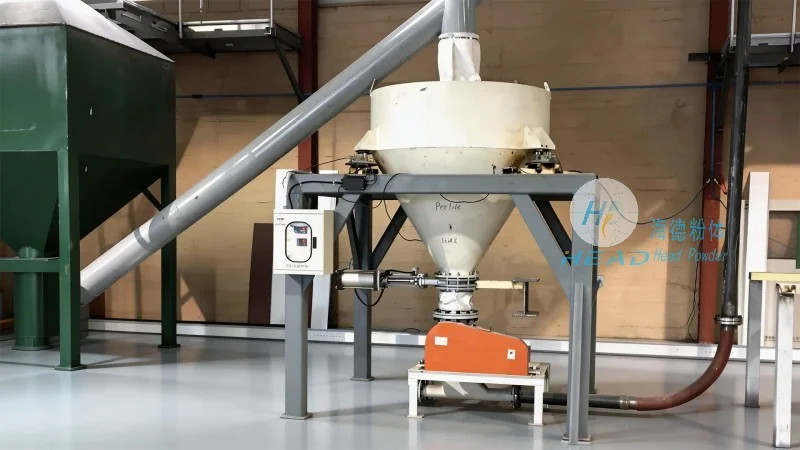
The powder electrolyte pneumatic conveying system is widely used in various industries that rely on the efficient handling of fine powders. In the battery manufacturing industry, for example, these systems are essential for transporting electrolyte powders to production lines, where they are used in the assembly of lithium-ion batteries. The automotive and electronics industries also benefit from these systems when handling materials used in components like capacitors and sensors. Other applications include the chemical and pharmaceutical industries, where precise material handling is critical to maintaining product quality. HeadPowder's systems are designed to meet the specific needs of these industries, providing reliable and efficient solutions that enhance productivity and reduce operational costs.
HeadPowder Engineering Co., Ltd., based in Shandong, China, stands as a trusted provider of powder electrolyte pneumatic conveying systems. By combining advanced engineering, high-quality materials, and a deep understanding of industrial needs, the company delivers systems that are both efficient and durable. The structure and working principle of the powder electrolyte pneumatic conveying line, as described in this article, highlight the sophistication and reliability of these systems. For industries seeking to improve their material handling processes, HeadPowder offers tailored solutions that enhance productivity, ensure safety, and maintain the quality of their products. With a commitment to excellence and customer satisfaction, HeadPowder continues to lead the way in providing innovative material handling solutions.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top