Heptahydrate magnesium sulfate, also known as Epsom salt, is a widely used chemical compound in various industrial applications. The pneumatic conveying system designed for handling this material efficiently is a critical piece of equipment for many processing facilities. This article provides an overview of the system's structure and operational principles, highlighting its role in ensuring safe and effective material transport.
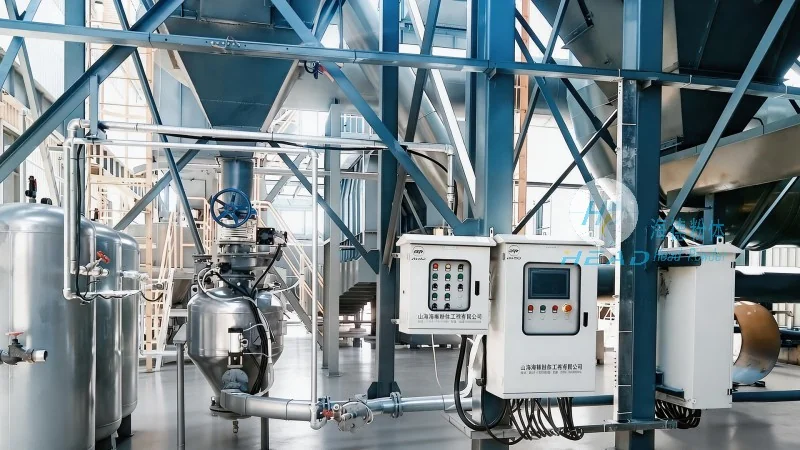
The pneumatic conveying system for heptahydrate magnesium sulfate is engineered to transport the material from storage silos or processing units to downstream equipment such as mixers, reactors, or packaging systems. The system operates by using compressed air to create a flow that moves the solid particles through a pipeline network. This method offers several advantages over traditional mechanical conveying systems, including reduced risk of dust contamination, lower maintenance requirements, and the ability to handle materials that are difficult to move by other means.
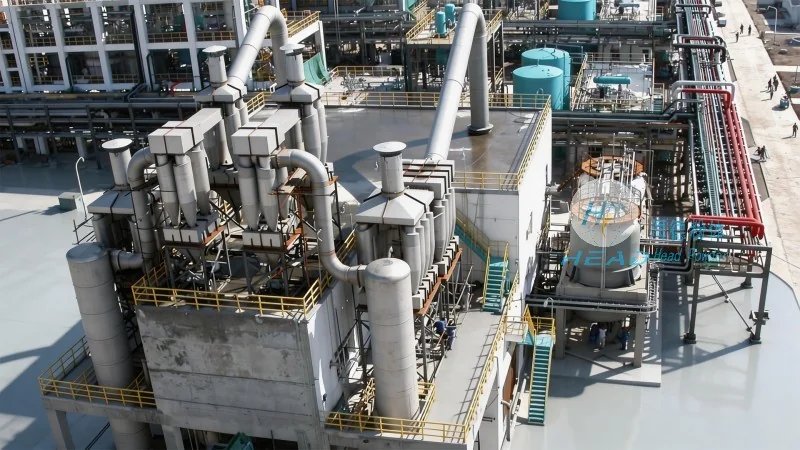
HeadPowder, the manufacturer of this pneumatic conveying system, is a leading company in the chemical processing equipment industry. With a focus on innovation and quality, HeadPowder has established itself as a trusted provider of solutions for material handling challenges. The company is headquartered in Shandong, China, and specializes in designing and manufacturing custom pneumatic conveying systems tailored to the specific needs of its clients.
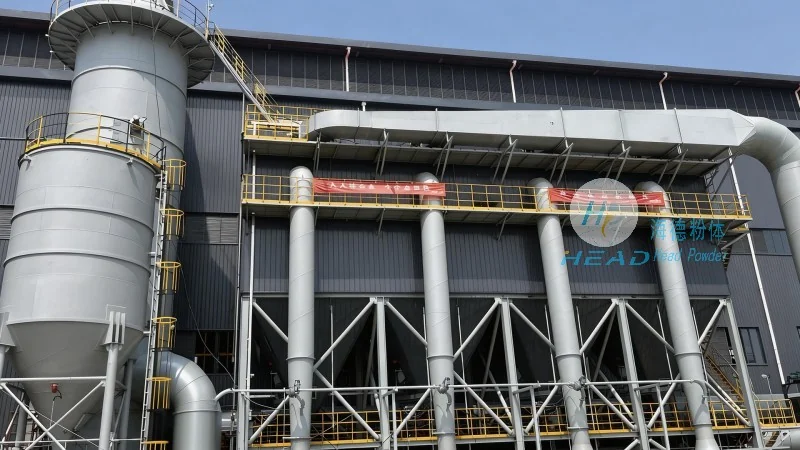
The pneumatic conveying system for heptahydrate magnesium sulfate typically consists of several key components that work together to ensure reliable operation. These include a material feeder, a pressure vessel or hopper, a pipeline network, and a control system. The material feeder is responsible for feeding the heptahydrate magnesium sulfate into the system at a controlled rate, while the pressure vessel helps to maintain consistent pressure within the system. The pipeline network transports the material from the feeder to the discharge point, and the control system monitors and regulates the operation of the entire system to prevent overpressure or underflow.
The operation of the pneumatic conveying system relies on the principle of fluidization and pneumatic transport. Compressed air is introduced into the pipeline at a specific pressure and flow rate, creating a flow that lifts and transports the heptahydrate magnesium sulfate particles. The air and material mixture travels through the pipeline, and the material is discharged at the end of the line. The system is designed to maintain a consistent flow rate and pressure, ensuring that the material is transported safely and efficiently without causing blockages or damage to the equipment.
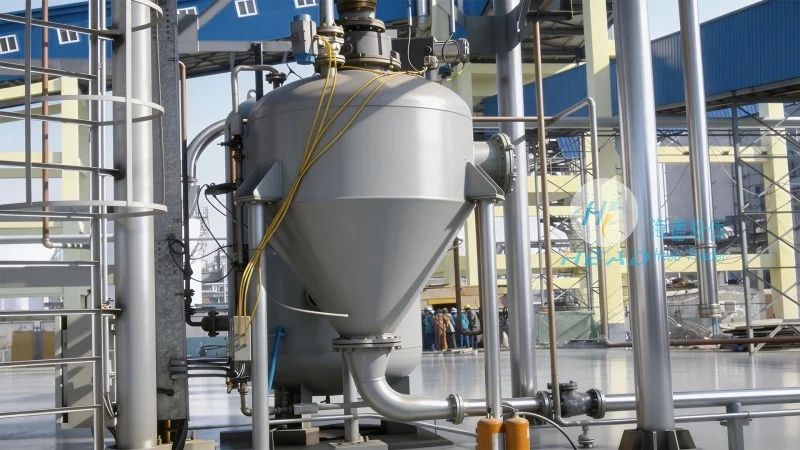
The pneumatic conveying system for heptahydrate magnesium sulfate offers several technical advantages that make it an ideal choice for many industrial applications. These include its ability to handle abrasive or corrosive materials, its low maintenance requirements, and its compact design that can be integrated into existing processing facilities. The system is commonly used in the chemical, pharmaceutical, and food processing industries, where the safe and efficient transport of heptahydrate magnesium sulfate is essential for product quality and regulatory compliance.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top