HeadPowder, a leading provider of industrial conveying systems, specializes in the design and implementation of pneumatic conveying solutions tailored for fertilizer granules. As a division of Shandong HeadPowder Engineering Co., Ltd., based in Shandong, China, the company leverages decades of expertise to deliver efficient, reliable, and cost-effective solutions for the fertilizer industry. This article explores the key aspects of pneumatic conveying systems for fertilizer granules, highlighting the technical advantages, operational benefits, and the role of HeadPowder in providing customized solutions.
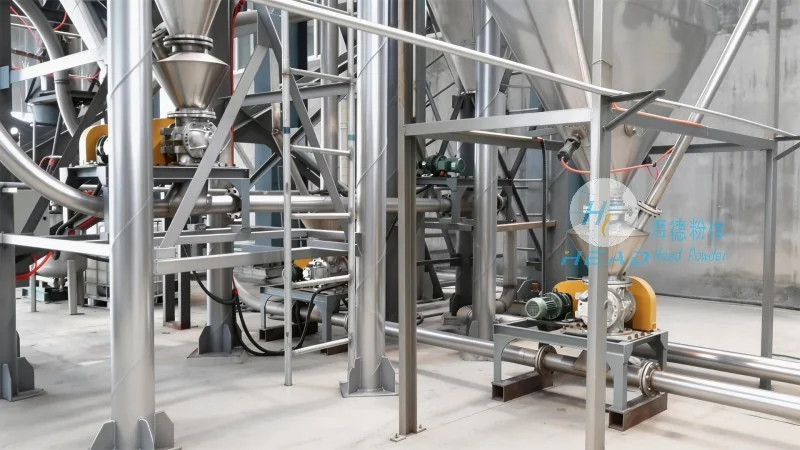
Pneumatic conveying is a method of transporting bulk materials, such as fertilizer granules, through a pipeline using air or gas as the conveying medium. Unlike traditional mechanical conveying systems like screw conveyors or belt conveyors, pneumatic systems offer several advantages, including the ability to handle fragile or abrasive materials without causing damage, reduced risk of contamination, and the capacity to transport materials over long distances with minimal maintenance. For fertilizer granules, which are often sensitive to handling and require gentle transport to preserve their quality and effectiveness, pneumatic conveying is an ideal choice. The technology involves creating a pressure differential within the pipeline, either by using a positive pressure system (where air is blown into the pipeline) or a negative pressure system (where air is drawn out), to move the granules from the source to the destination. HeadPowder’s engineers design systems that optimize the pressure, flow rate, and pipeline configuration to ensure efficient and consistent transport of fertilizer granules, minimizing product degradation and maximizing system performance.
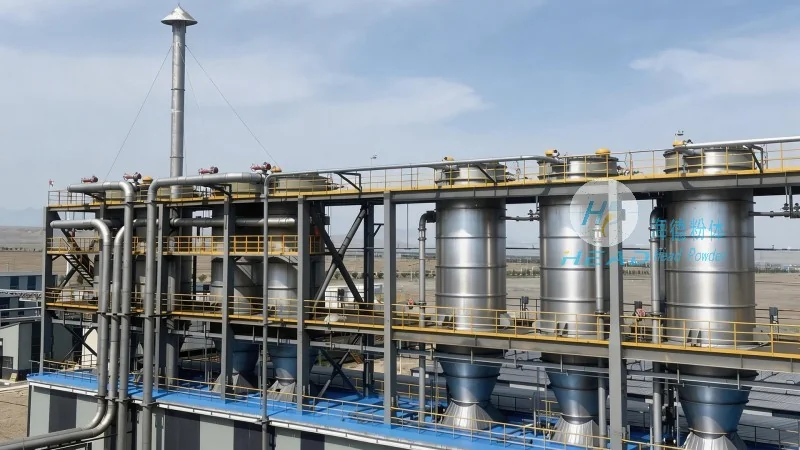
HeadPowder’s pneumatic conveying solutions for fertilizer granules are engineered with a focus on durability, efficiency, and adaptability. The company utilizes high-quality materials, such as stainless steel and corrosion-resistant alloys, to construct pipelines and components that can withstand the harsh conditions of fertilizer handling, including moisture, dust, and chemical exposure. This ensures long-term reliability and minimal downtime for the end-user. Additionally, HeadPowder’s systems are designed to be energy-efficient, with optimized air flow and pressure control mechanisms that reduce operational costs while maintaining high transport rates. The company also offers customizable solutions, allowing clients to tailor the system to their specific production needs, including varying capacities, distances, and material characteristics. For example, a positive pressure system may be preferred for short-distance transport of bulk fertilizer granules, while a negative pressure system could be more suitable for longer distances or when dealing with dusty environments. HeadPowder’s expertise in both system design and installation ensures that each solution is optimized for the unique requirements of the fertilizer facility, whether it involves handling raw materials, intermediate products, or finished granules.
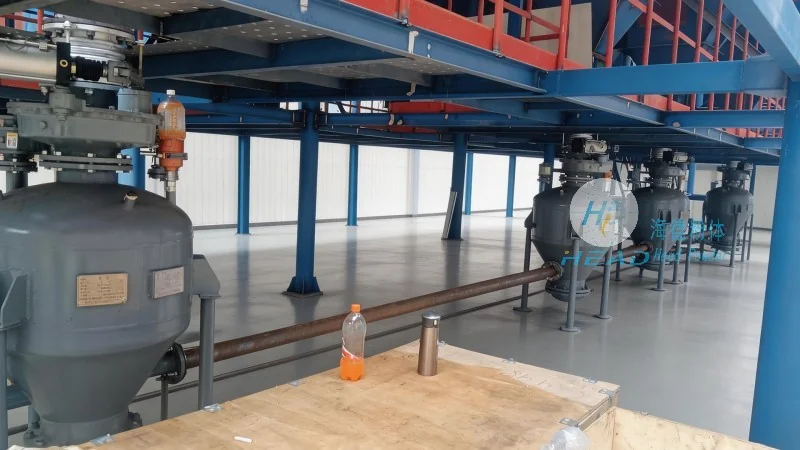
The application of pneumatic conveying for fertilizer granules spans various stages of the production and distribution process. In the manufacturing phase, these systems are used to transport raw materials, such as urea or ammonium nitrate, from storage silos to processing units. During the granulation process, pneumatic conveyors efficiently move the wet or dry granules from the granulator to the drying or cooling equipment. After processing, the finished fertilizer granules are conveyed to packaging or storage areas, ensuring a seamless flow of materials throughout the facility. The operational advantages of using pneumatic systems in these scenarios are significant. Unlike mechanical conveyors, which can cause abrasion or breakage to the granules, pneumatic systems gently transport the material, preserving its size and shape. This is crucial for maintaining the fertilizer’s effectiveness, as particle size directly impacts its nutrient release and application performance. Furthermore, pneumatic conveyors can operate in enclosed environments, reducing dust emissions and improving workplace safety. The ability to transport materials vertically and horizontally with minimal space requirements also makes these systems ideal for facilities with limited floor space or complex layouts. HeadPowder’s systems are designed to integrate seamlessly with existing production lines, minimizing disruptions during installation and ensuring a smooth transition to the new conveying technology.
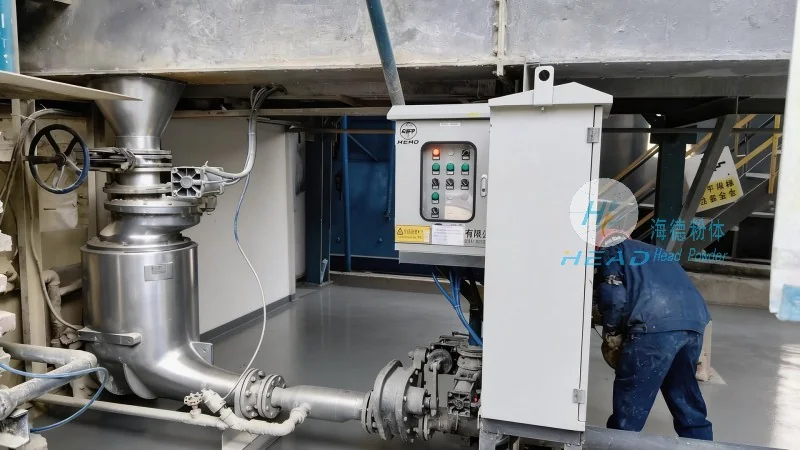
At HeadPowder, the focus is on providing tailored solutions that meet the specific needs of each client. The company’s engineering team works closely with clients to assess their current operations, identify pain points, and develop a customized pneumatic conveying system for fertilizer granules. This includes evaluating factors such as the type and size of fertilizer granules, the required transport capacity, the distance between source and destination, and any environmental or safety regulations that must be adhered to. Once a design is finalized, HeadPowder handles all aspects of the project, from manufacturing and supply of components to installation and commissioning. The company also provides comprehensive after-sales support, including maintenance services, spare parts availability, and technical assistance to ensure the system operates at peak performance over its lifespan. This commitment to customer satisfaction and long-term partnership is a key differentiator for HeadPowder in the fertilizer conveying industry.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top