Silage material pneumatic conveying machines are critical equipment in modern agricultural and livestock operations, designed to efficiently transport high-moisture forage materials like silage from storage to processing or feeding areas. These systems leverage the principles of pneumatic transport to move bulk materials through a sealed pipeline using air pressure or suction, offering advantages such as hygienic handling, reduced labor, and flexible layout. The operation and working principle of such machines are essential for optimizing material flow and ensuring consistent performance in agricultural settings.
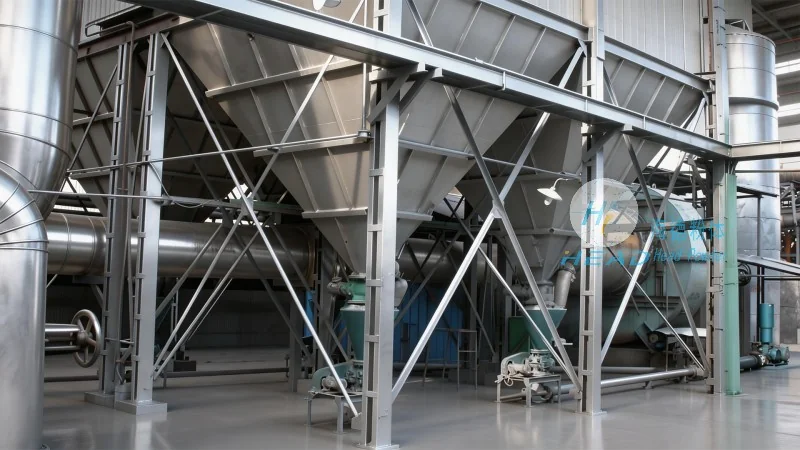
A typical silage material pneumatic conveying system consists of several interconnected components that work in tandem to achieve efficient material transport. The primary components include:
- **Feeding Unit**: This is where the silage material is introduced into the system. It may feature a hopper or a rotary valve to control the flow rate and ensure a steady supply of material.
- **Air Supply System**: Comprised of a blower or compressor that generates the necessary air pressure or vacuum to move the material through the pipeline. The air supply is crucial for creating the pressure differential required for pneumatic transport.
- **Conveying Pipeline**: A network of pipes that transports the silage material and air mixture. The pipeline design, including diameter and material, is critical for minimizing pressure loss and ensuring smooth flow.
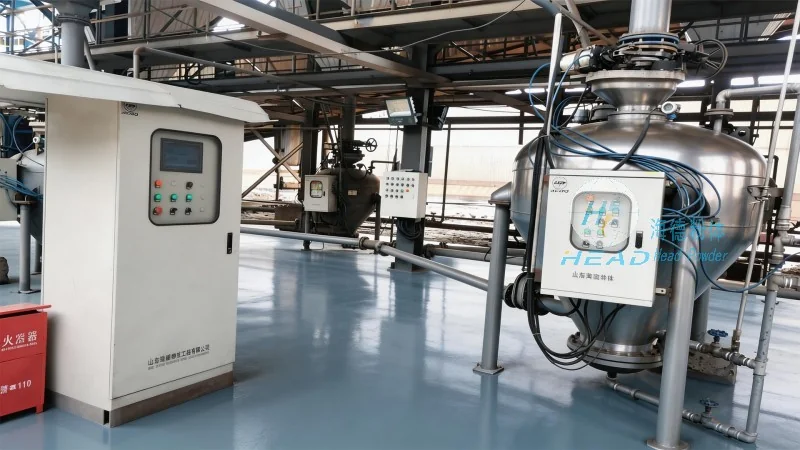
- **Separation and Cleaning Equipment**: After the material reaches its destination, a separator (such as a cyclone or filter) removes the air from the material stream, allowing the silage to be discharged while the air is recirculated or vented.
- **Control System**: An automated control panel that monitors and regulates the operation of the system, including air pressure, flow rate, and material level.
The working principle of a silage material pneumatic conveying machine is based on the movement of material particles suspended in a stream of air. There are two main types of pneumatic conveying: pressure and suction. For silage applications, pressure systems are more common due to their ability to handle high-moisture, sticky materials without clogging.
In a pressure system, the blower creates positive pressure at the inlet of the conveying pipeline. The silage material is fed into the pipeline, and the high-pressure air forces the material to move through the system. The air and material mixture travels through the pipeline to the discharge point, where the separator separates the material from the air. The separated air is then returned to the blower for recirculation, while the silage is collected in a storage or feeding bin.
The key to efficient operation lies in maintaining the correct air-to-material ratio. If the air flow is too low, the material may not be fully suspended and could cause blockages. Conversely, excessive air flow can lead to high energy consumption and reduced material transport efficiency. Proper system design and regular maintenance are essential to ensure optimal performance.
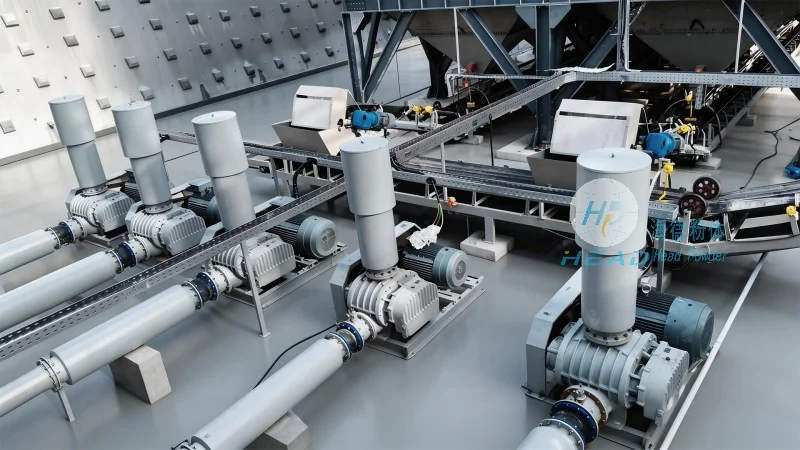
The operation of a silage material pneumatic conveying machine typically follows a sequence of steps to ensure smooth and continuous material transport. Here is a detailed breakdown of the process:
1. **Preparation and Setup**: Before operation, the system is checked for any blockages or leaks in the pipeline and air supply. The feeding hopper is filled with silage material, and the control system is set to the desired operating parameters (e.g., air pressure, flow rate).
2. **Material Feeding**: The rotary valve or hopper feeder starts, and the silage material is introduced into the conveying pipeline. The material is mixed with the high-pressure air from the blower, creating a slurry-like mixture that moves through the system.
3. **Conveying and Transport**: The air and material mixture travels through the pipeline to the discharge point. The pipeline may include bends, vertical sections, or horizontal runs, all designed to minimize pressure loss and maintain flow.
4. **Separation and Discharge**: At the discharge end, the separator (e.g., a cyclone) separates the silage material from the air. The silage is collected in a storage bin or feeding trough, while the air is filtered and recirculated back to the blower.
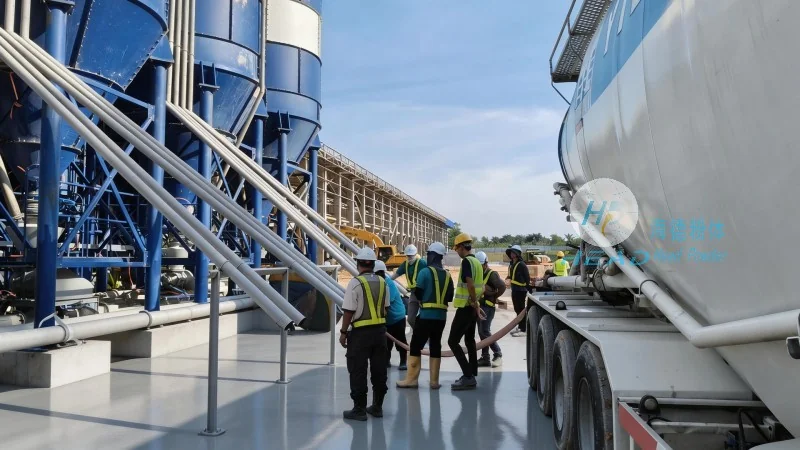
5. **System Monitoring and Adjustment**: The control system continuously monitors key parameters such as air pressure, material flow rate, and system temperature. If any deviations are detected, the system automatically adjusts the air flow or feeding rate to maintain optimal performance.
6. **Shutdown and Maintenance**: When the operation is complete, the system is shut down in an orderly manner. The pipeline is cleaned to remove any residual material, and routine maintenance tasks (e.g., filter replacement, blower inspection) are performed to ensure the system remains in good working condition.
Implementing a pneumatic conveying system for silage material offers several benefits that enhance operational efficiency and product quality. Some of the key advantages include:
- **Hygienic Handling**: The sealed pipeline prevents contamination from dust, pests, or environmental factors, ensuring the silage remains clean and safe for animal consumption.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top