HeadPowder, a leading provider in the field, specializes in designing and manufacturing advanced pneumatic conveying systems tailored for handling glucose and similar bulk materials. The company, based in Shandong, China, has established itself as a trusted partner for industries requiring efficient and reliable material transport solutions. This article delves into the operation process and working principles of their glucose material pneumatic conveying machines, offering insights into how these systems enhance productivity and operational efficiency.
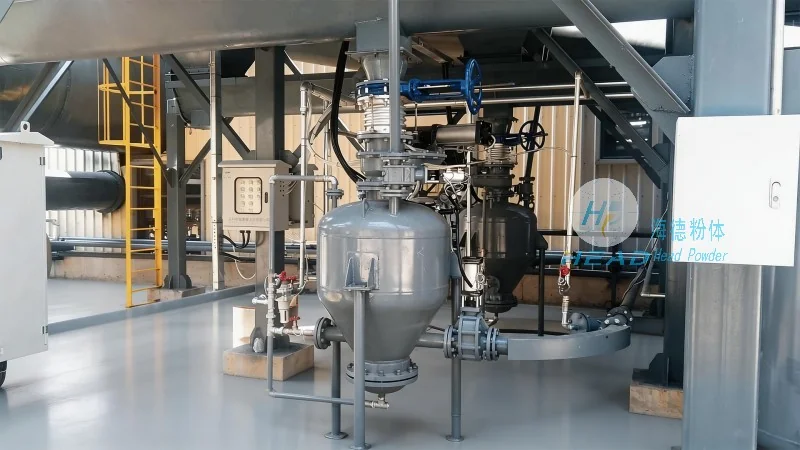
Pneumatic conveying machines utilize air or gas to transport bulk materials like glucose from one location to another. The technology offers several advantages over traditional methods, such as reduced labor costs, minimized product contamination, and improved safety in handling potentially hygienic or sensitive materials. HeadPowder's systems are engineered to meet stringent industry standards, ensuring compliance with food processing regulations and maintaining the quality of the glucose product throughout the conveying process.
The core components of HeadPowder's glucose pneumatic conveying system include a hopper for material storage, a rotary valve for controlled material discharge, a conveyor line (either positive or negative pressure depending on the application), and a receiver for the discharged material. The system may also incorporate additional features like a filter to remove dust or moisture, a pressure regulator to maintain consistent air pressure, and a control panel for monitoring and adjusting operational parameters. Each component is meticulously designed to handle the specific characteristics of glucose, such as its granular size, moisture content, and flowability.
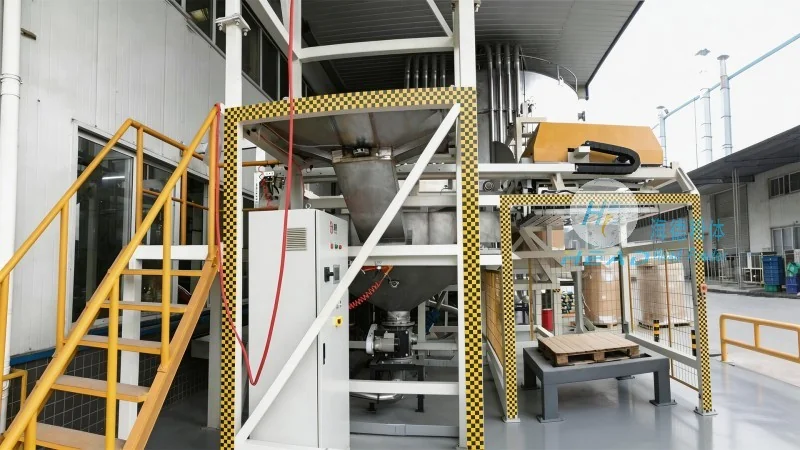
The operation of the glucose material pneumatic conveying machine begins with material loading into the hopper. The rotary valve then regulates the flow of glucose into the conveyor line, ensuring a steady feed rate. Compressed air is introduced into the system, creating a pressure differential that propels the material through the pipeline. As the material travels, it is mixed with the air stream, forming a slurry that moves efficiently to the receiver. The receiver collects the conveyed glucose, and the air is typically filtered and recycled back into the system to minimize waste and energy consumption. The entire process is automated, with the control panel allowing operators to adjust speed, pressure, and flow rates to optimize performance based on the specific requirements of the glucose handling operation.
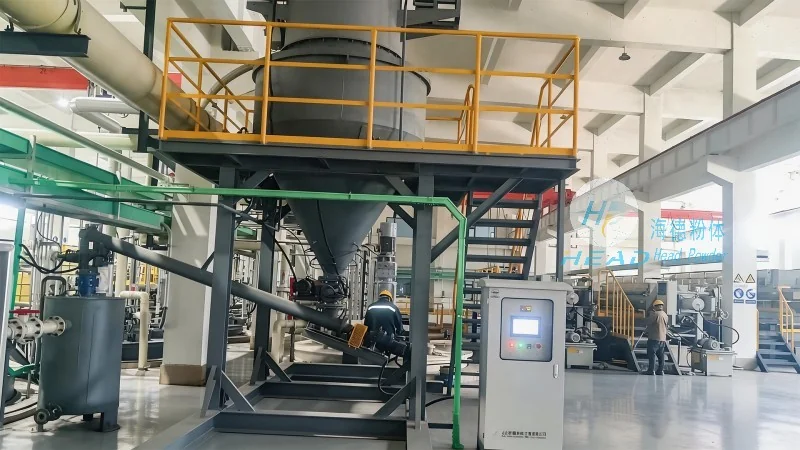
The working principle of the pneumatic conveying machine for glucose relies on the principles of fluid dynamics and particle transport. In positive pressure systems, compressed air is forced through the conveyor line, pushing the glucose particles forward. The air velocity is maintained above the material's terminal velocity to prevent settling or blockages. In negative pressure systems, a vacuum is created at the receiver end, drawing the material and air into the pipeline. Both systems are effective for glucose, with the choice depending on factors like the distance to be covered and the material's properties. HeadPowder's systems are designed to balance efficiency and energy consumption, ensuring that the conveying process is both effective and economical.
Implementing a pneumatic conveying system for glucose offers numerous benefits to manufacturers. These include increased throughput, reduced downtime due to fewer maintenance requirements, and improved product quality by minimizing exposure to contaminants. The technology is particularly suitable for applications in the food and pharmaceutical industries, where hygiene and product integrity are paramount. HeadPowder's glucose material pneumatic conveying machines have been successfully deployed in various facilities, supporting the smooth operation of glucose production lines and ensuring consistent supply of the material to downstream processes.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top