The biological enzyme material pneumatic conveyor is a specialized equipment designed for the efficient and safe transportation of materials that are sensitive to moisture, temperature, or air exposure, such as biological enzymes, pharmaceutical powders, and other fine chemicals. This equipment is particularly crucial in industries like biotechnology, pharmaceuticals, and food processing, where maintaining the integrity and activity of the conveyed materials is paramount. The system is manufactured by Shandong HeadPowder Engineering Co., Ltd., a leading company based in China, known for its advanced engineering solutions tailored to the needs of the biotech and pharmaceutical sectors. The design of this conveyor system integrates advanced pneumatic technology with precise control mechanisms to ensure optimal performance and minimal product degradation during the conveying process.
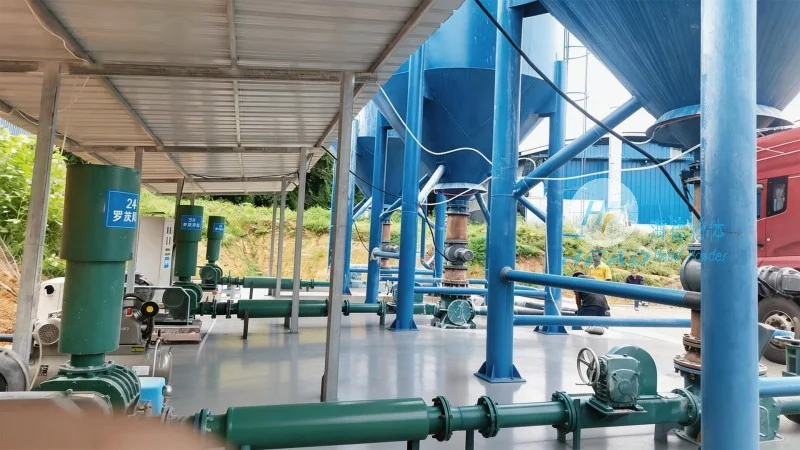
The biological enzyme material pneumatic conveyor consists of several core components that work in tandem to facilitate material transport. These include the hopper or feeding device, the conveying pipeline, the air supply system (blower or compressor), the control valves, and the discharge unit. The hopper is typically equipped with a feeding mechanism, such as a screw feeder or a rotary valve, to regulate the flow of the enzyme material into the pipeline. The pipeline is made of materials like stainless steel or food-grade plastic to prevent contamination and maintain the purity of the biological product. The air supply system generates the necessary air pressure to move the material through the pipeline, while the control valves allow for precise adjustment of air flow and pressure to optimize conveying efficiency. The discharge unit, often a rotary valve or a pressure relief valve, ensures the material is released safely and without spillage.
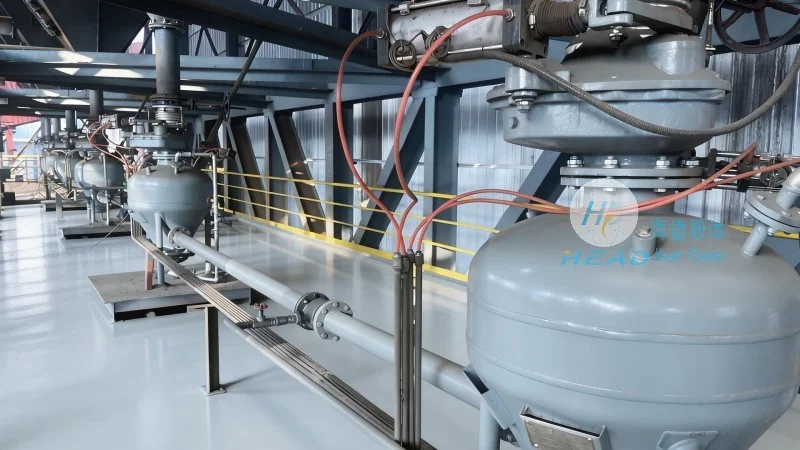
The operation of the biological enzyme material pneumatic conveyor follows a systematic sequence to ensure smooth and efficient material transport. The process begins with the loading of the biological enzyme material into the hopper. The feeding mechanism then regulates the flow of the material into the conveying pipeline, ensuring a consistent feed rate. Simultaneously, the air supply system generates the required air pressure, which is then introduced into the pipeline. The air flow, combined with the material, creates a slurry or suspension that is propelled through the pipeline to the discharge point. The control valves play a critical role in maintaining the air pressure and flow rate, preventing backflow and ensuring the material reaches the destination without clogging or loss. The discharge unit then releases the material into the receiving container, completing the conveying cycle. The entire process is typically automated, with sensors and control systems monitoring parameters like pressure, flow rate, and material level to ensure optimal performance and safety.
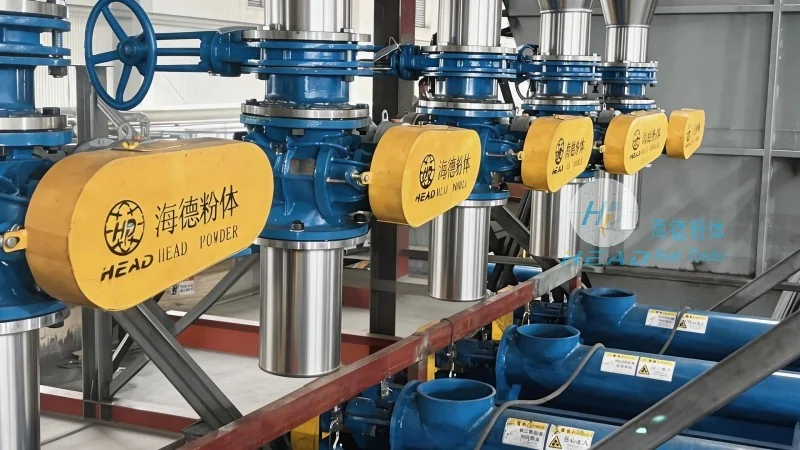
The working principle of the biological enzyme material pneumatic conveyor is based on the principles of pneumatic transport, where materials are conveyed using a gas stream. In this system, the air supply unit generates a high-pressure air flow, which is introduced into the conveying pipeline. The biological enzyme material is then introduced into the pipeline, either by gravity or by the feeding mechanism, and is carried along by the air stream. The air flow creates a negative pressure or a positive pressure environment, depending on the type of pneumatic conveyor (e.g., suction or pressure system), to move the material through the pipeline. The key to efficient conveying is the balance between the air flow rate and the material feed rate, which must be optimized to prevent clogging and ensure the material is transported without degradation. The system also incorporates features like air filtration and moisture control to maintain the quality of the biological enzyme material during transport. The discharge unit then separates the material from the air stream, allowing the material to be collected in the receiving container while the air is either recirculated or vented, depending on the system design.
The biological enzyme material pneumatic conveyor offers several advantages that make it ideal for transporting sensitive materials. These include its ability to maintain the integrity and activity of the biological enzyme product, its minimal contact with the material (reducing contamination risk), and its flexibility in handling different material types and conveying distances. The equipment is particularly suitable for applications in the biotechnology and pharmaceutical industries, where the quality and purity of the product are critical. It can be used for conveying enzymes from production lines to storage tanks, from processing units to packaging areas, or for transferring materials between different production stages. The conveyor system can also be customized to meet specific requirements, such as varying conveying capacities, pipeline lengths, and material characteristics, making it a versatile solution for various industrial needs.
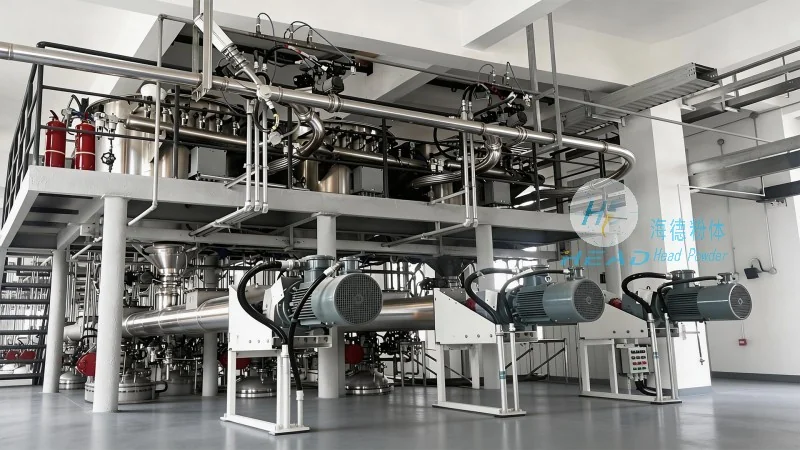
To ensure the reliable and long-term operation of the biological enzyme material pneumatic conveyor, regular maintenance and adherence to safety protocols are essential. Maintenance activities include cleaning the hopper and pipeline to prevent material buildup and clogging, checking the air supply system for proper operation, and inspecting the control valves and sensors for any signs of wear or malfunction. The equipment should be cleaned regularly, especially after handling different materials, to prevent cross-contamination. Safety considerations include ensuring proper ventilation to remove any dust or airborne particles, using appropriate personal protective equipment (PPE) when operating the equipment, and following the manufacturer's guidelines for operation and maintenance. Regular inspections and maintenance can help prevent breakdowns, reduce downtime, and ensure the safe and efficient operation of the conveyor system.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top