For industrial facilities dealing with bulk powder materials, efficient and reliable conveying systems are crucial for maintaining production efficiency and safety. The tonne bag powder conveying line, a specialized solution developed by Shandong HeadPowder Engineering Co., Ltd. based in China, offers a comprehensive approach to handling large volumes of powders from tonne bags. This system integrates advanced technology and robust engineering to ensure seamless material transfer, making it an essential component for various industries such as chemical, food, and pharmaceutical sectors.
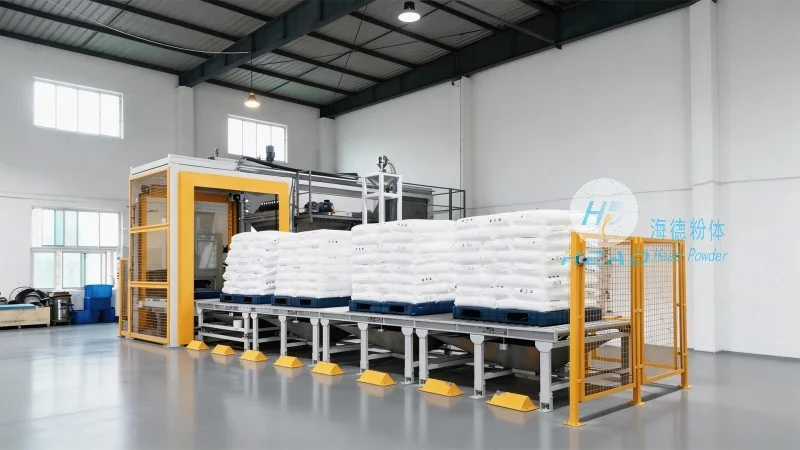
The tonne bag powder conveying line is designed to automate the process of unloading, conveying, and storing bulk powders from tonne bags. It typically consists of several key components, including a hopper for receiving material, a conveyor system (often a screw or pneumatic conveyor), and a storage silo or processing equipment. The system is engineered to handle a wide range of powder types, from fine powders to bulkier granules, while maintaining consistent flow rates and minimizing material loss or contamination.
Each component of the tonne bag powder conveying line plays a critical role in the overall operation. The receiving hopper is the first stage, where tonne bags are placed and the material is discharged into the system. This hopper is usually equipped with a discharge valve or gate to control the flow of material into the conveyor. The conveyor system, which can be either a screw conveyor or a pneumatic conveyor, transports the powder from the hopper to the next stage of processing or storage. Screw conveyors are ideal for dry, free-flowing powders, while pneumatic conveyors are suitable for more delicate or dusty materials. The storage silo or processing equipment is the final stage, where the powder is collected and prepared for further use or distribution.
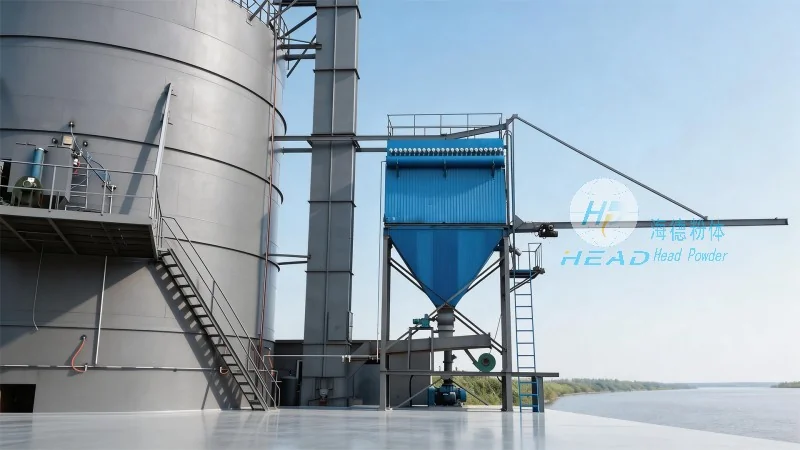
The operation of the tonne bag powder conveying line begins with the placement of a tonne bag into the receiving hopper. The hopper’s discharge valve is then opened, allowing the powder to flow into the conveyor system. The conveyor then moves the material through the system, ensuring a steady and controlled flow. In a screw conveyor, the rotating screw pushes the powder forward, while in a pneumatic conveyor, the powder is carried by a stream of air. The material is then delivered to the storage silo or processing equipment, where it is stored or processed according to the specific requirements of the application.
The working principle of the tonne bag powder conveying line is based on the principles of material handling and fluid dynamics. The system relies on gravity and mechanical force to move the powder from the hopper to the storage or processing equipment. The receiving hopper provides a controlled environment for the material to be discharged, preventing spillage and ensuring a uniform flow. The conveyor system then uses either mechanical or pneumatic pressure to transport the powder, maintaining consistent velocity and preventing blockages. The storage silo or processing equipment is designed to handle the incoming material, ensuring that it is stored or processed efficiently and safely.
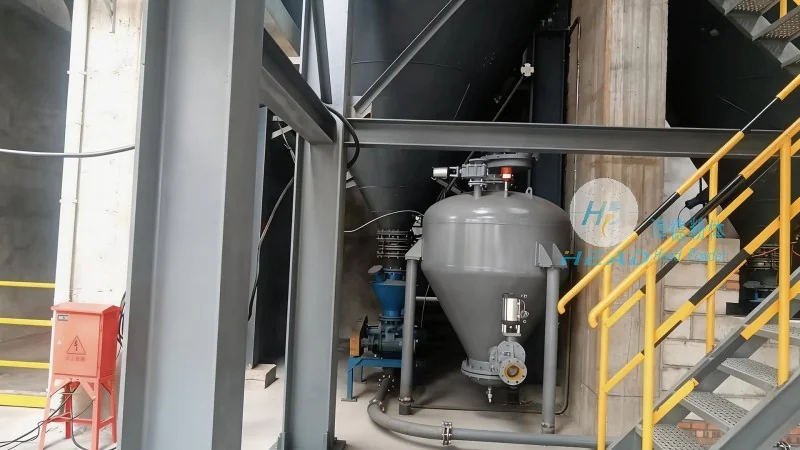
Implementing a tonne bag powder conveying line offers several advantages for industrial operations. Firstly, it significantly improves the efficiency of material handling by automating the process of unloading and conveying bulk powders. This reduces the need for manual labor and minimizes the risk of material loss or contamination. Secondly, the system is designed to handle large volumes of powder, making it suitable for high-production environments. Thirdly, the components are robust and durable, ensuring long-term operation with minimal maintenance. Finally, the system is flexible and can be customized to meet the specific needs of different industries, allowing for adaptation to various powder types and processing requirements.
The tonne bag powder conveying line is widely used in various industries. In the chemical industry, it is used to handle raw materials such as powders and granules, ensuring a smooth supply chain for production processes. In the food industry, it is used to transport ingredients like flour, sugar, and spices, maintaining hygiene and quality standards. In the pharmaceutical industry, it is used to handle active pharmaceutical ingredients (APIs) and other sensitive materials, ensuring that the powder is handled safely and efficiently. These applications highlight the versatility and reliability of the tonne bag powder conveying line as a critical component in modern industrial operations.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top