The negative pressure dilute phase powder conveying line is a specialized system designed for the efficient and safe transportation of bulk powders over long distances. This technology is widely used in various industries such as food, pharmaceuticals, chemicals, and minerals, where maintaining product purity and minimizing contamination is critical. The system operates by creating a negative pressure environment within the conveying pipeline, which draws the powder particles into the air stream and transports them to the destination. The design of this system ensures optimal performance by balancing the air flow, particle size, and pipeline length, making it suitable for a wide range of applications. Developed by Shandong HeadPowder Engineering Co., Ltd. (headpowder), based in China, this system is engineered to meet the highest standards of efficiency and reliability.
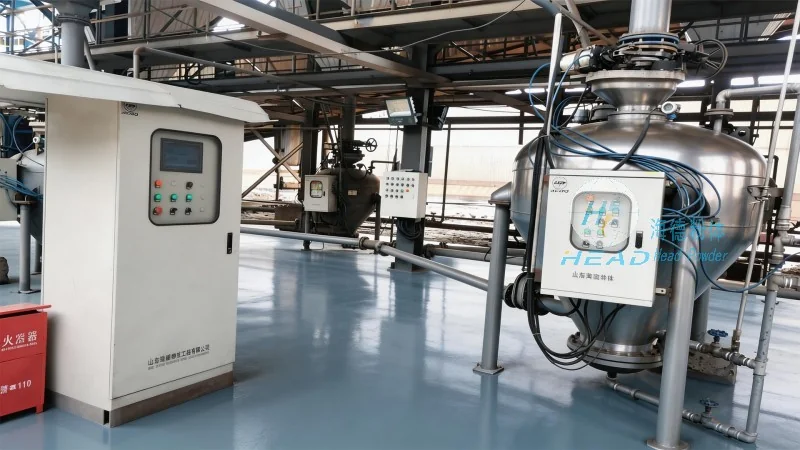
The negative pressure dilute phase powder conveying line consists of several key components that work in tandem to ensure smooth operation. The primary components include the feeding unit, the conveying pipeline, the air compressor, the filter system, and the discharge unit. The feeding unit is responsible for introducing the powder into the system, typically using a rotary valve or a screw feeder to control the flow rate. The conveying pipeline, usually made of stainless steel or other corrosion-resistant materials, is designed to withstand the pressure and temperature conditions of the operation. The air compressor generates the necessary airflow to create the negative pressure, while the filter system ensures that the air is clean and free from dust particles that could affect the product quality. The discharge unit collects the powder at the end of the pipeline and transfers it to the storage or processing equipment.
The working principle of the negative pressure dilute phase powder conveying line is based on the principle of suction. The system creates a lower pressure inside the pipeline compared to the ambient air pressure, which causes the powder particles to be drawn into the air stream. The air flow carries the powder particles through the pipeline, maintaining a dilute phase (i.e., low particle concentration) to prevent blockages and ensure efficient transport. The velocity of the air is carefully controlled to ensure that the powder particles are suspended and transported without settling or clogging the pipeline. The system also incorporates pressure sensors and flow meters to monitor the operation and adjust the air flow as needed to maintain optimal performance.
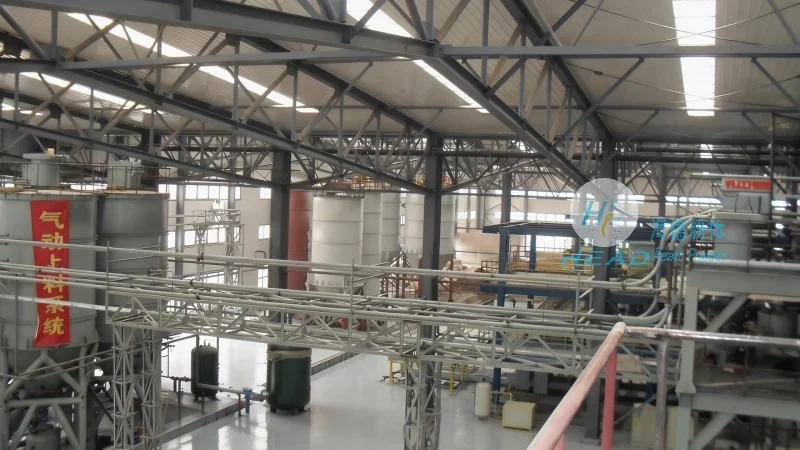
The operation of the negative pressure dilute phase powder conveying line involves several steps that are carefully controlled to ensure safety and efficiency. The process begins with the preparation of the powder, which may include drying or screening to ensure that the particle size and moisture content are within the required specifications. The powder is then fed into the system using the feeding unit, which is controlled by a programmable logic controller (PLC) to maintain a consistent flow rate. The air compressor is started, and the negative pressure is established in the pipeline. The powder is drawn into the pipeline and transported to the discharge unit, where it is collected and transferred to the next stage of processing. The system is equipped with safety features such as pressure relief valves and emergency stop buttons to prevent accidents and ensure the safety of the operators. The control system monitors the pressure, flow rate, and temperature of the system, and adjusts the operation parameters as needed to maintain optimal performance.
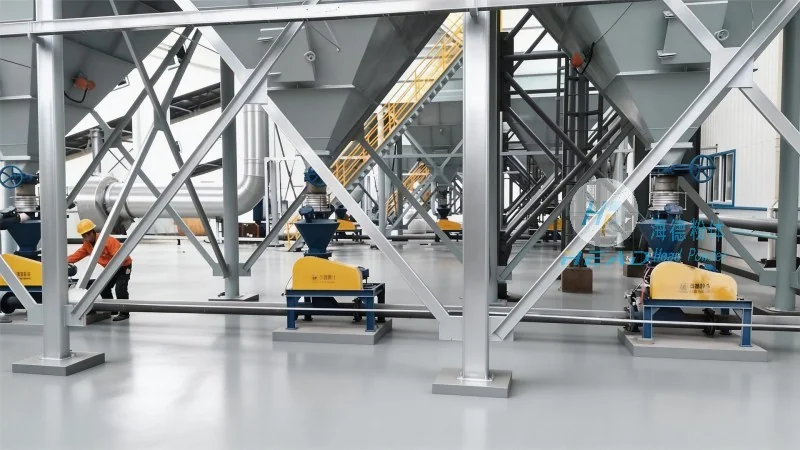
The negative pressure dilute phase powder conveying line offers several advantages over other conveying methods, making it a preferred choice for many industries. One of the main advantages is its ability to transport powders over long distances without the need for intermediate storage or transfer points. This reduces the risk of product contamination and improves the overall efficiency of the process. Another advantage is its ability to handle a wide range of powder types, including fine powders, granules, and bulk materials. The system is also relatively low maintenance, as the components are designed to be durable and resistant to wear and tear. The negative pressure system is particularly suitable for applications where product purity is critical, such as in the food and pharmaceutical industries. The system is also used in the chemical and mineral industries for the transportation of raw materials and finished products.
In conclusion, the negative pressure dilute phase powder conveying line is a highly efficient and reliable system for the transportation of bulk powders. The system operates by creating a negative pressure environment within the pipeline, which draws the powder particles into the air stream and transports them to the destination. The design of the system ensures optimal performance by balancing the air flow, particle size, and pipeline length. The system is widely used in various industries and offers several advantages over other conveying methods. With proper maintenance and operation, the negative pressure dilute phase powder conveying line can provide long-term and cost-effective solutions for powder transportation needs.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top