Camellia seed powder conveying equipment is a specialized system designed to handle the transportation of camellia seed powder efficiently and safely. As a key component in the processing line of camellia seed oil extraction, this equipment ensures the smooth flow of raw material from the processing stage to the subsequent production steps. The design and operation of such equipment are crucial for maintaining the quality and consistency of the final product, making it an essential asset for manufacturers in the camellia seed industry.
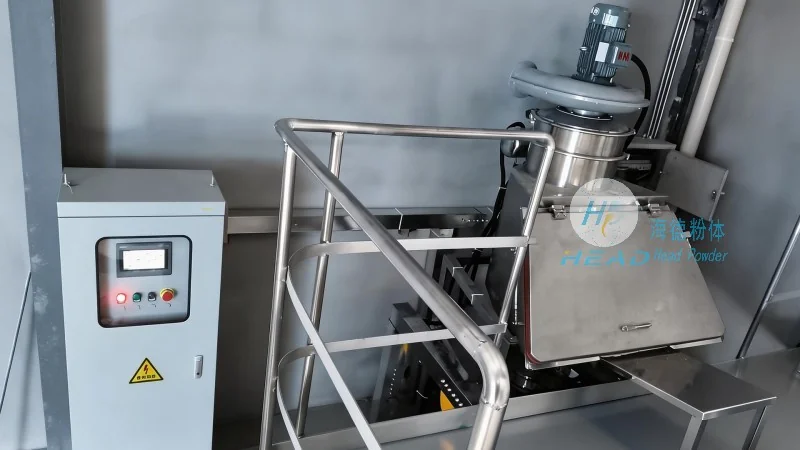
The camellia seed powder conveying equipment typically consists of several core components, each playing a vital role in the overall operation. These components include the hopper, conveyor system, control panel, and dust collection unit. The hopper serves as the storage and feeding section, where raw camellia seed powder is loaded and held before being transferred. The conveyor system, often equipped with a screw or belt mechanism, moves the powder from the hopper to the processing or packaging area. The control panel allows operators to monitor and adjust the speed and flow rate, ensuring precise control over the conveying process. Additionally, the dust collection unit is integrated to manage air quality and prevent dust dispersion, which is critical for maintaining a safe and clean working environment.
The operation of camellia seed powder conveying equipment follows a systematic process that begins with material loading and ends with delivery to the next stage of production. Initially, the raw camellia seed powder is fed into the hopper from a storage silo or processing machine. The hopper’s design, often with a sloped bottom, facilitates the gravity-driven flow of the powder into the conveyor. Once the powder reaches the conveyor, it is moved along the path set by the equipment. The conveyor’s speed can be adjusted based on the required throughput, allowing for flexibility in production rates. As the powder travels, it may pass through a series of sensors or filters to ensure that only the desired material is conveyed, preventing contamination or blockages. Finally, the powder is discharged into a collection bin or directly into the processing machinery, completing the conveying cycle.
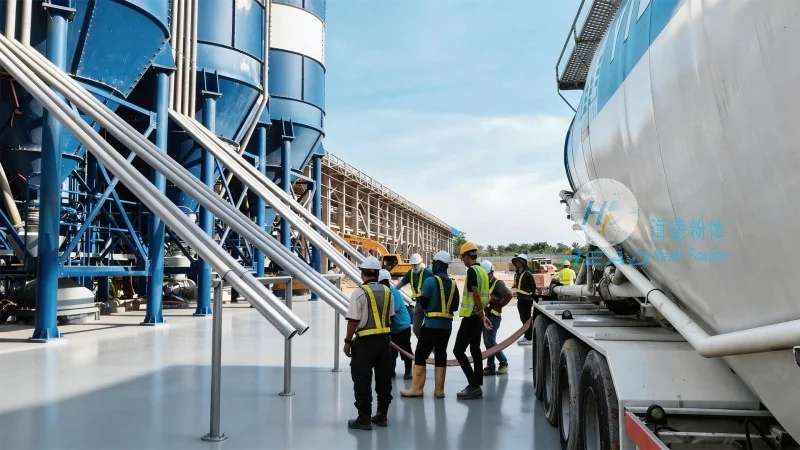
The working principle of camellia seed powder conveying equipment is based on mechanical energy transfer and material handling technology. The primary mechanism involves the use of a conveyor system, which can be either a screw conveyor or a belt conveyor, depending on the specific design and application. In a screw conveyor, a rotating screw blade pushes the powder forward along the trough, while in a belt conveyor, a moving belt carries the material. The control system regulates the speed of the conveyor, which directly impacts the flow rate of the powder. The hopper’s design, with its airtight and dust-proof features, helps maintain the integrity of the powder and prevents moisture or air from entering, which could affect the powder’s quality. The integration of a dust collection system works in conjunction with the conveyor to capture any airborne particles, ensuring compliance with environmental and safety standards. This combination of mechanical and control systems enables the equipment to operate efficiently, with minimal downtime and optimal performance.
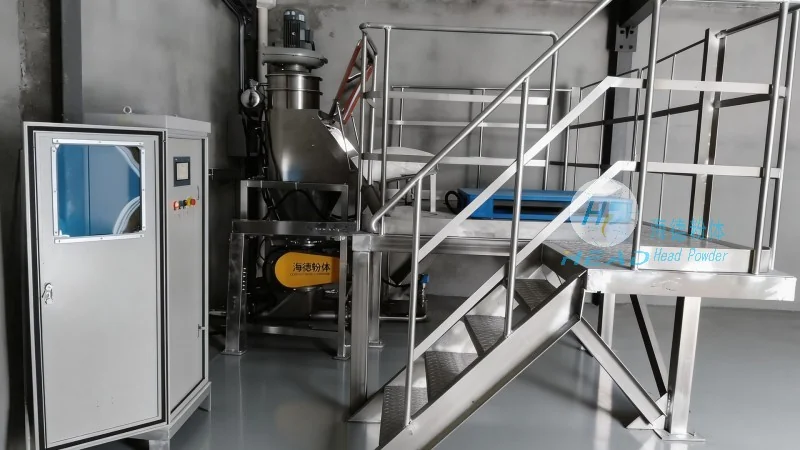
Camellia seed powder conveying equipment offers several benefits to manufacturers, including improved efficiency, reduced labor costs, and enhanced product quality. By automating the material handling process, the equipment minimizes the need for manual labor, which not only saves time but also reduces the risk of human error. The consistent flow of powder ensures that the subsequent processing steps, such as pressing or refining, receive a uniform feed, leading to better product consistency. Additionally, the dust collection system helps maintain a clean and safe working environment, reducing the risk of respiratory issues among workers and minimizing the impact on the surrounding environment. The equipment is widely used in the camellia seed oil industry, where it plays a critical role in the production of high-quality oil and by-products. It is also suitable for other industries that handle fine powders, such as food processing and pharmaceuticals, where precision and safety are paramount.
Shandong HeadPowder Engineering Co., Ltd., operating under the brand name headpowder, is a leading manufacturer of specialized conveying equipment for the powder and bulk material handling industry. With a focus on innovation and quality, the company has developed a range of products tailored to meet the unique needs of various industries, including the camellia seed processing sector. Headpowder’s camellia seed powder conveying equipment is designed and manufactured with precision engineering, ensuring durability, reliability, and efficiency. The company’s commitment to customer satisfaction is reflected in its comprehensive after-sales support and technical assistance, providing users with the necessary guidance to maximize the equipment’s performance. Headpowder’s products are widely recognized for their advanced technology and adherence to international standards, making them a trusted choice for manufacturers seeking reliable and effective conveying solutions.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top