For industrial applications requiring efficient and reliable powder handling, capsule powder conveying systems offer a sophisticated solution. These systems are designed to transport fine powders, granules, and other particulate materials with precision, ensuring minimal product degradation and consistent performance. Understanding the operation process and working principle of such systems is crucial for optimizing production lines and maintaining operational efficiency.
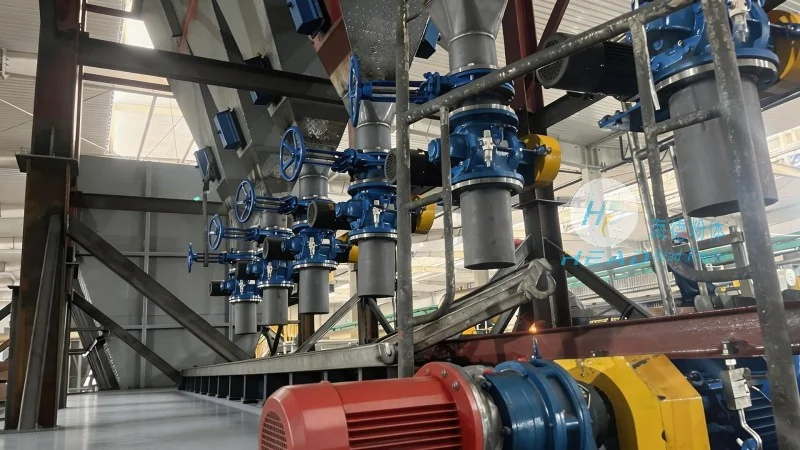
Capsule powder conveying systems, developed by Shandong HeadPowder Engineering Co., Ltd., utilize advanced engineering principles to address the challenges of handling sensitive or abrasive powders. The system's design focuses on maintaining material integrity while ensuring smooth, continuous transport. This approach is particularly beneficial in industries such as pharmaceuticals, food processing, and chemical manufacturing, where product quality and consistency are paramount.
The capsule powder conveying system consists of several key components, each playing a vital role in the overall operation. The primary components include the hopper, conveyor tube, air distribution system, and control unit. The hopper serves as the storage container, holding the powder material ready for transport. The conveyor tube, typically made of flexible or rigid material, forms the path for the powder. The air distribution system generates the necessary airflow to move the powder through the tube, while the control unit manages the system's operation, ensuring precise control over speed and pressure.
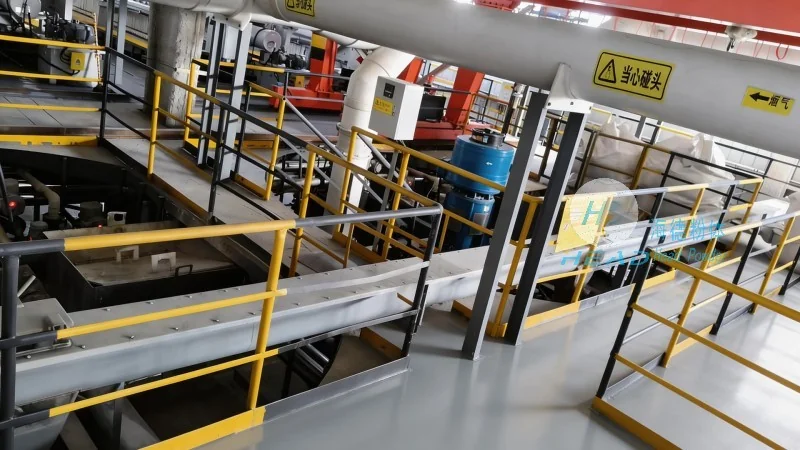
The operation of a capsule powder conveying system follows a systematic process. Initially, the powder is fed into the hopper from a storage silo or bulk container. As the powder accumulates, it is drawn into the conveyor tube by the controlled airflow generated by the system's blower. The airflow, often referred to as pneumatic conveying, propels the powder particles through the tube in a consistent manner. The system's control unit monitors the pressure and flow rate, adjusting the airflow as needed to maintain optimal transport conditions. This dynamic adjustment ensures that the powder moves without clogging or excessive pressure buildup, which could damage the material or the system.
The working principle of capsule powder conveying relies on the principles of fluid dynamics and particle motion. The system uses a combination of pressure and velocity to move the powder. In the pressure-type conveying method, the air is pressurized and forced through the tube, carrying the powder particles along. In the suction-type method, the air is drawn from the tube, creating a vacuum that pulls the powder. The capsule design, which refers to the shape of the conveying tube or the method of material movement, enhances the efficiency of this process by minimizing friction and ensuring uniform particle distribution. This design reduces the risk of material segregation and ensures that all particles are conveyed uniformly.
Implementing a capsule powder conveying system offers several advantages over traditional methods. These include reduced product contamination, as the system operates in a closed environment, preventing exposure to external contaminants. Additionally, the system minimizes material degradation by avoiding direct contact with mechanical components, which can cause abrasion or breakage. The flexibility of the system allows for easy integration into existing production lines, and the modular design enables scalability to accommodate varying production volumes. The consistent performance of the system also contributes to improved process control and reduced downtime, leading to higher overall productivity.
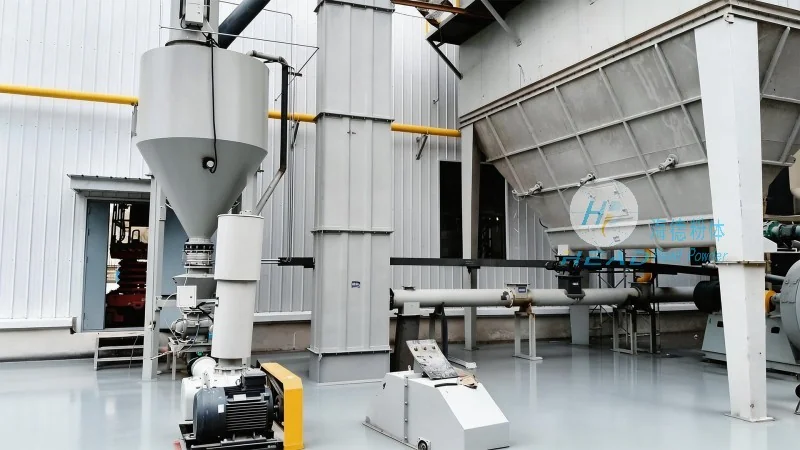
The versatility of capsule powder conveying systems makes them suitable for a wide range of applications. In the pharmaceutical industry, these systems are used to transport active pharmaceutical ingredients (APIs) and excipients, ensuring that the final product meets stringent quality standards. In food processing, they handle ingredients like sugar, flour, and spices, maintaining the purity and freshness of the products. The chemical industry benefits from the system's ability to handle abrasive and corrosive powders, protecting equipment and ensuring safe handling. Overall, the systems provide a reliable solution for industries that require precise and efficient powder handling.
Shandong HeadPowder Engineering Co., Ltd. specializes in the design, manufacturing, and implementation of advanced powder conveying systems, including capsule powder conveying solutions. With a focus on innovation and customer satisfaction, the company provides tailored solutions to meet the specific needs of its clients. The company's headquarters is located in Shandong, China, and it serves a global market with its high-quality products and technical expertise. By understanding the operation process and working principle of capsule powder conveying systems, industries can enhance their operational efficiency and product quality, ensuring long-term success in their respective fields.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top