Organic fertilizer powder conveying lines are critical systems in the agricultural and fertilizer production sectors. These systems are engineered to efficiently transport organic fertilizer powders from storage silos or production areas to processing units or packaging stations. The technology integrates advanced engineering principles with practical application to ensure reliable material handling. For businesses involved in organic fertilizer manufacturing, understanding the working principle and key features of such lines is essential for optimizing production processes and maintaining operational efficiency.
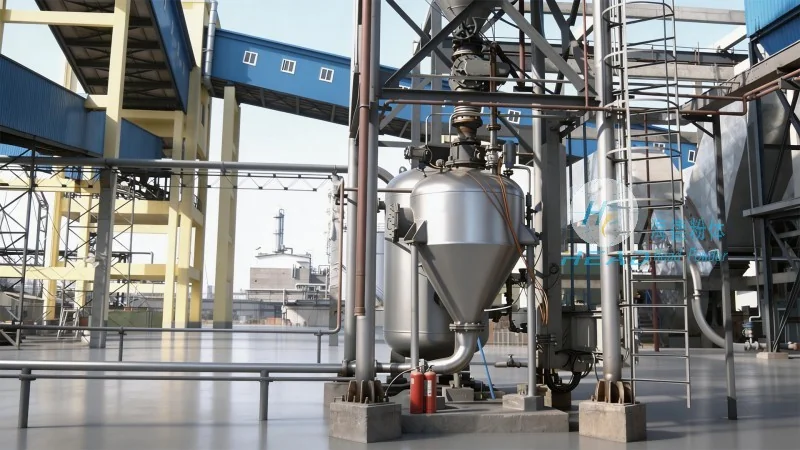
The operation of an organic fertilizer powder conveying line involves interconnected components that work in unison to move the material. The process starts with raw organic fertilizer powders stored in bulk silos or hoppers. The material is then fed into a conveyor system, which may include screw conveyors, pneumatic conveyors, or a hybrid setup. The choice of conveyor type depends on factors like bulk density, moisture content, and particle size. For instance, screw conveyors are suitable for materials with moderate bulk density and low moisture, while pneumatic conveyors are ideal for fine powders requiring dust control and minimal contamination.
Once fed into the conveyor, the material travels through a network of pipes or troughs. In pneumatic systems, compressed air creates a flow of air and powder mixture, propelling the material forward. Air velocity and pressure are carefully regulated to prevent clogging or excessive wear. In screw or belt conveyors, rotating components push or carry the material along, requiring regular maintenance to avoid wear. Intermediate storage hoppers or surge bins may be included to regulate flow and prevent overloading downstream equipment.
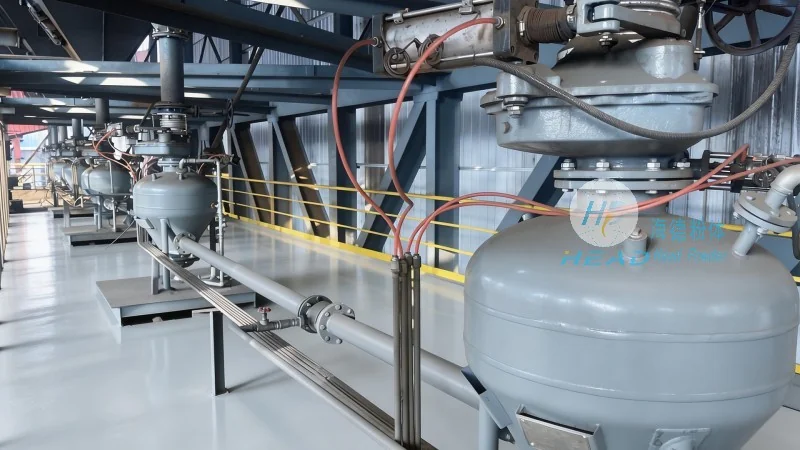
Organic fertilizer powder conveying lines are defined by features that enhance performance and reliability. One primary feature is their ability to handle diverse organic fertilizer types, including compost, manure, and other organic materials. These systems accommodate varying particle sizes and moisture levels, ensuring consistent transport. Another critical feature is dust control. Organic fertilizers are fine powders that generate significant dust, posing health and safety risks. Modern systems incorporate dust collection systems like cyclones or bag filters to capture airborne particles, improving workplace safety and environmental compliance.
Efficiency is a key characteristic, as systems are designed to minimize energy use while maximizing material throughput. Advanced control systems, including variable frequency drives (VFDs) and sensors, enable real-time monitoring and adjustment of conveyor speed and pressure. This dynamic control optimizes energy use while maintaining consistent flow. Additionally, enclosed system designs reduce product degradation and contamination, with components resistant to corrosion and wear from organic fertilizers.
Organic fertilizer powder conveying lines are used across various stages of fertilizer production, from raw material handling to final packaging. In the initial phase, they transport raw organic materials to processing units for mixing or further processing. During blending, conveying lines ensure even distribution of all components, crucial for high-quality organic fertilizers. In the final stage, they move finished powders to packaging machines or storage silos, preparing them for distribution.
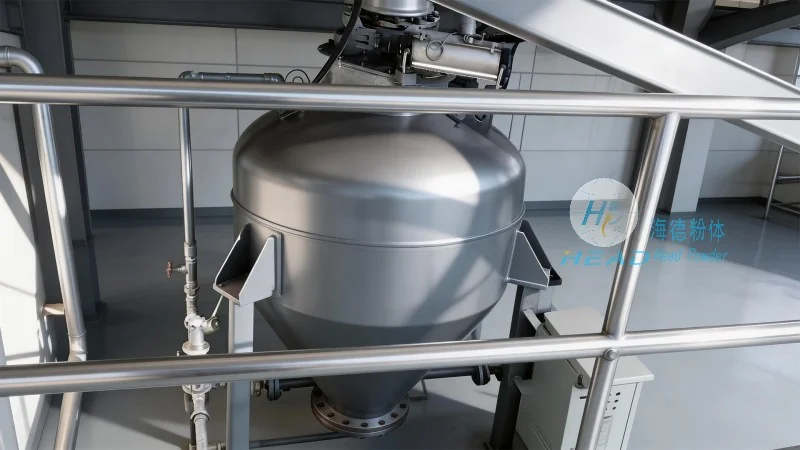
The benefits extend beyond efficiency. By reducing manual handling, these systems enhance workplace safety by minimizing dust exposure and heavy lifting. They also contribute to environmental sustainability by preventing dust emissions and reducing packaging needs. Consistent transport ensures smooth production, reducing downtime and improving productivity. For companies like Shandong HeadPowder Engineering Co., Ltd., specializing in fertilizer industry solutions, these conveying lines are a core product, tailored to meet the unique needs of organic fertilizer manufacturers.
Organic fertilizer powder conveying lines represent a sophisticated technology in modern fertilizer production. Their working principle, combining conveyor mechanisms with advanced control systems, ensures efficient and reliable transport of organic fertilizer powders. Key features like dust control, energy efficiency, and product protection make these systems indispensable for businesses aiming to optimize processes and maintain safety and environmental standards. As a leading provider, Shandong HeadPowder Engineering Co., Ltd. offers comprehensive solutions tailored to organic fertilizer manufacturers, helping them achieve operational excellence and sustainable growth in the agricultural sector.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top