Shandong HeadPowder Engineering Co., Ltd., a leading manufacturer in the field, specializes in the design, development, and production of advanced pneumatic conveying systems tailored for ammonia fertilizer applications. Based in Shandong, China, the company leverages years of industry experience to deliver efficient and reliable solutions that meet the stringent demands of modern fertilizer processing and transportation. This article delves into the operational process and working principles of such systems, highlighting key components, functional mechanisms, and the technical advantages that make them indispensable in the fertilizer industry.
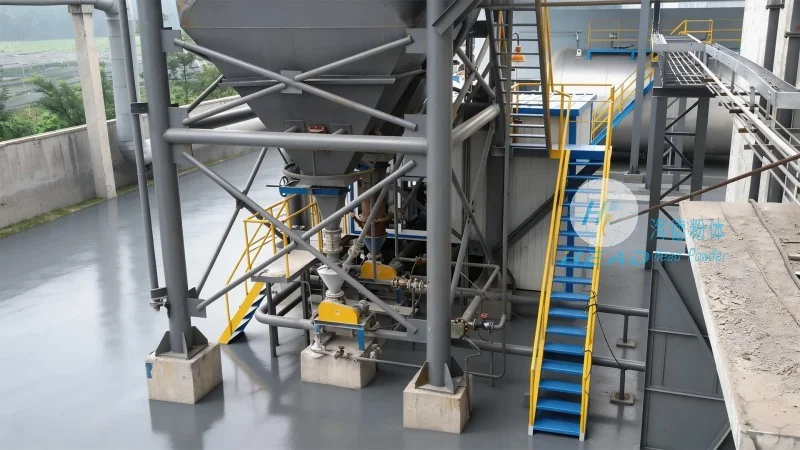
The ammonia fertilizer pneumatic conveying system typically comprises several critical components that work in tandem to ensure smooth material handling. The main elements include the hopper, which serves as the storage and feeding unit for the fertilizer; the air compressor or blower, responsible for generating the necessary airflow to transport the material; the conveying pipeline, which forms the pathway for the material and air mixture; and the control system, which regulates the operation of the entire system. Additionally, auxiliary components such as filters, cyclones, and dust collectors are integrated to maintain air quality and prevent material loss. Each component is meticulously designed to handle the unique properties of ammonia fertilizer, including its granular or powder form, and the potential challenges posed by moisture or corrosive characteristics.
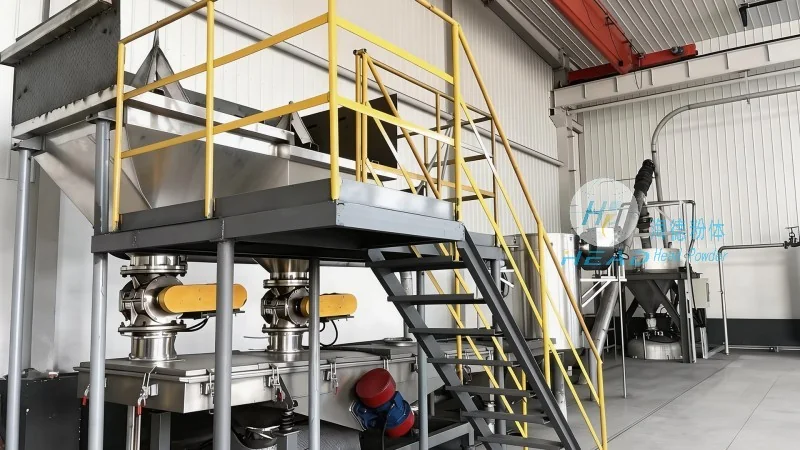
The operation of the ammonia fertilizer pneumatic conveying system follows a systematic sequence that ensures efficient material transport from the storage hopper to the discharge point. The process begins with the material being fed into the hopper, where it accumulates until the system is activated. Once the system is started, the air compressor or blower generates a high-pressure airflow, which is directed into the conveying pipeline. The air then enters the hopper through a venturi or inlet, creating a low-pressure zone that draws the fertilizer particles into the air stream. As the material is entrained by the air, it travels through the pipeline to the discharge point, where the air and material mixture is separated. The separation process often involves a cyclone or filter, where the air is released while the fertilizer is collected in a receiving bin. This separation ensures that the air is clean and can be recirculated, reducing energy consumption and environmental impact. The entire process is controlled by a programmable logic controller (PLC) or similar system, which monitors parameters such as airflow rate, pressure, and material flow, adjusting the operation as needed to maintain optimal performance.
The operational process of the ammonia fertilizer pneumatic conveying system can be broken down into several key steps, each critical to the system's efficiency and reliability. The first step involves material loading into the hopper, where the fertilizer is stored until the system is ready for transport. The second step is the activation of the air compressor, which starts generating the required airflow. The third step is the initiation of the conveying process, where the material is drawn into the air stream and transported through the pipeline. The fourth step is the separation of the material from the air at the discharge point, typically using a cyclone or filter. The fifth step is the collection of the fertilizer in the receiving bin, and the final step is the recirculation of the air back to the system for reuse. Each step is carefully designed to minimize downtime and maximize throughput, with the control system continuously monitoring and adjusting parameters to ensure smooth operation. The system is also equipped with safety features, such as pressure relief valves and emergency stop buttons, to prevent accidents and protect personnel and equipment.
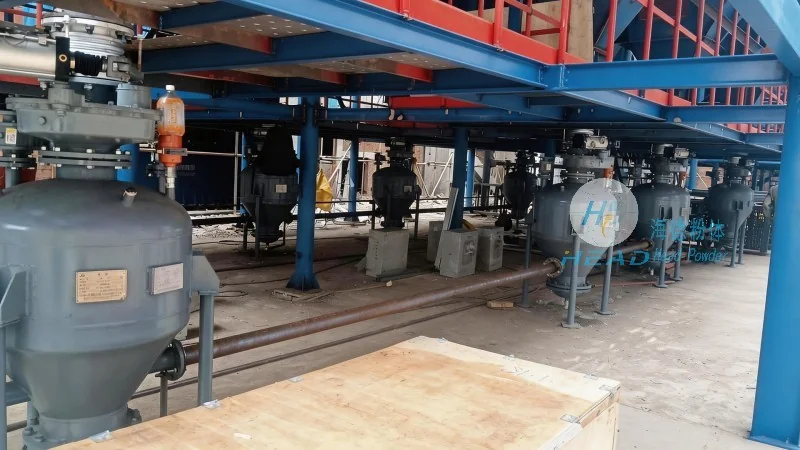
Ammonia fertilizer pneumatic conveying systems offer several technical advantages that make them ideal for modern fertilizer processing and transportation. One of the primary benefits is the ability to handle bulk materials efficiently, reducing the need for manual handling and minimizing the risk of material loss or contamination. The system's design allows for high throughput rates, with the ability to transport large volumes of fertilizer over long distances with minimal energy consumption. Additionally, the system is highly flexible, capable of adapting to different fertilizer types and processing requirements. The use of pneumatic conveying also reduces the need for additional equipment, such as conveyors or elevators, simplifying the overall system layout and reducing maintenance costs. These advantages make the system suitable for a wide range of applications, including fertilizer production plants, storage facilities, and distribution centers. The system's reliability and efficiency also contribute to improved operational performance, allowing companies to meet production targets and customer demands more effectively.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top