HeadPowder, a leading provider in the field, specializes in the design, manufacturing, and installation of pneumatic conveying systems tailored for the food additives industry. This article delves into the operational process and underlying principles of such systems, offering a comprehensive understanding of how they efficiently handle and transport food additives while maintaining strict adherence to hygiene and safety standards.
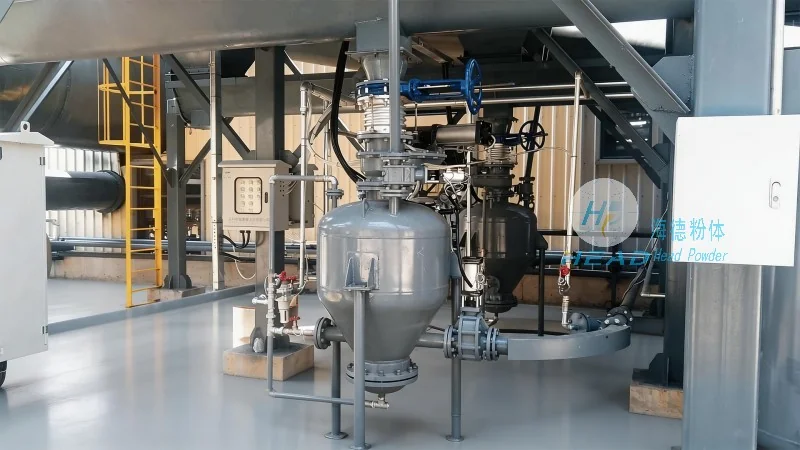
Pneumatic conveying, as a key technology in material handling, utilizes compressed air to move bulk materials through a pipeline network. For food additives, this method is particularly advantageous due to its ability to minimize product contamination, preserve product quality, and ensure a clean, dust-free environment. The system typically consists of several core components, including a hopper for material storage, a conveyor line with appropriate ductwork, a control system for air flow management, and a discharge unit for material release. Each component plays a critical role in the seamless operation of the entire process.
The operational process begins with the loading of food additives into the storage hopper. The hopper is designed with airtight seals and smooth interior surfaces to prevent material degradation and contamination. Once the hopper is filled, the control system activates the compressed air supply, which is regulated to an appropriate pressure and flow rate. The air, introduced into the conveyor line, creates a flow that lifts and propels the food additives through the pipeline. The conveying velocity and pressure are carefully controlled to ensure efficient transport without causing product degradation or excessive wear on the system components.
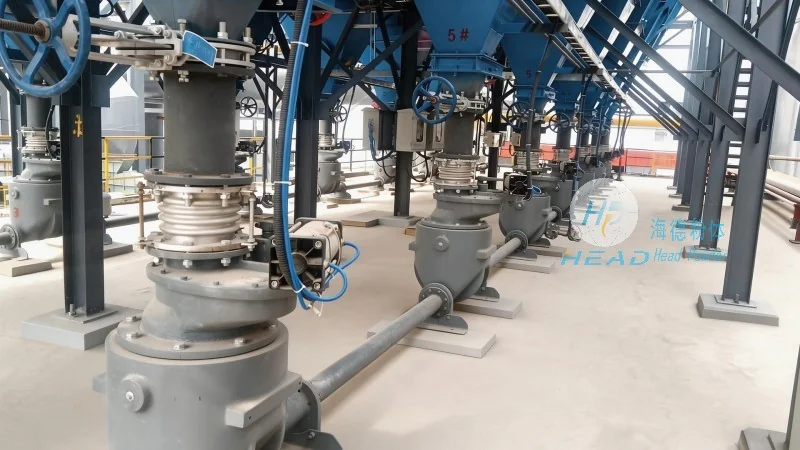
As the food additives travel through the pipeline, they are suspended in the air stream, moving from the hopper to the discharge point. The system may include intermediate components such as cyclones or filters to separate the material from the air stream, ensuring that the product remains clean and free from dust or debris. The discharge unit, often a rotary valve or a metering device, regulates the flow of material out of the system, allowing for precise control over the discharge rate. This control is essential for maintaining consistent product flow and preventing overloading or underloading of downstream processing equipment.
The working principle of pneumatic conveying for food additives is based on the fundamental physics of fluid dynamics and particle movement. The system relies on the Bernoulli principle, which states that an increase in the speed of a fluid occurs simultaneously with a decrease in pressure or a decrease in the fluid's potential energy. In pneumatic conveying, compressed air is introduced into the pipeline, creating a high-velocity air stream that generates a low-pressure zone. This low-pressure zone draws the food additives into the air stream, allowing them to be carried along the pipeline. The air velocity is maintained at a level sufficient to keep the particles suspended and prevent them from settling or sticking to the pipeline walls. The system's design, including the size and shape of the ductwork, the angle of the pipeline, and the type of air distribution, all contribute to optimizing the conveying efficiency and minimizing energy consumption.
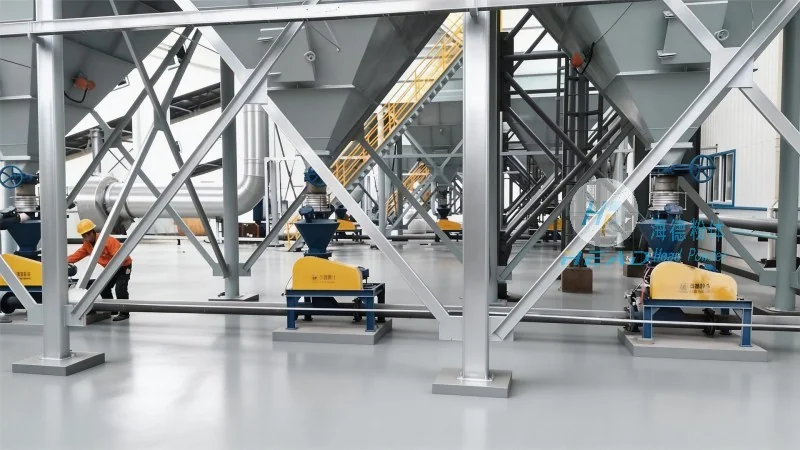
HeadPowder's expertise lies in customizing pneumatic conveying systems to meet the specific requirements of food additive applications. Whether handling fine powders, granules, or bulk materials, the company's engineers design systems that ensure optimal performance, reliability, and compliance with industry standards. The company's facilities in Shandong, China, are equipped with advanced technology and skilled personnel to develop and manufacture high-quality conveying systems that enhance operational efficiency and product quality for clients worldwide.
By understanding the operation process and working principles of pneumatic conveying for food additives, businesses can make informed decisions about implementing or upgrading their material handling systems. The benefits of such systems, including improved hygiene, reduced labor costs, and increased operational efficiency, make them a valuable investment for food additive manufacturers. HeadPowder remains committed to providing innovative solutions that meet the evolving needs of the food industry, ensuring that its clients can maintain competitive advantages through reliable and efficient material handling technologies.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top