HeadPowder, a leading provider in the field of powder handling technology, specializes in the design, manufacturing, and implementation of intelligent powder pneumatic conveying systems. With a strong presence in Shandong, China, the company has established itself as a trusted partner for industries requiring efficient and reliable powder transport solutions. This article delves into the fundamental principles behind these systems and highlights key application scenarios where their advanced capabilities are particularly beneficial.
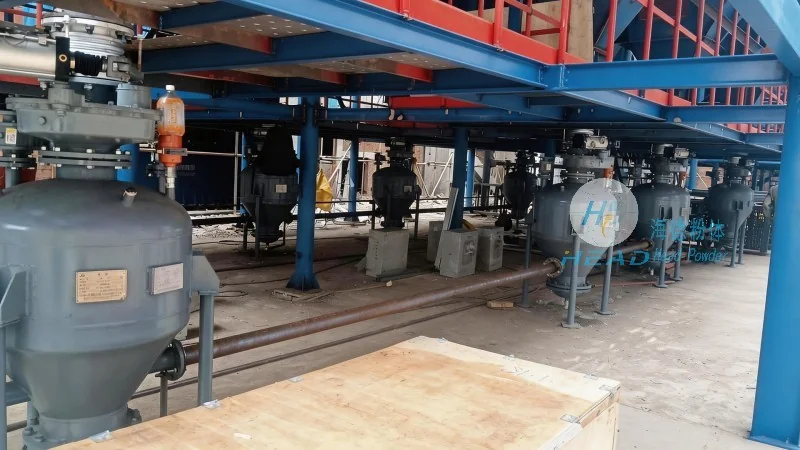
The intelligent powder pneumatic conveying system operates on the principle of using compressed air or other gas to transport bulk powder materials through a network of pipes. Unlike traditional mechanical conveying methods, this technology offers a flexible and efficient approach to moving powders over short to medium distances. The system typically consists of a blower, a hopper for material storage, a conveying line, and a receiver for the discharged material. Advanced control systems, often integrated with sensors and automation, enable real-time monitoring and adjustment of the conveying process, ensuring optimal performance and minimizing downtime.
Key components of the system include the air compressor, which generates the necessary pressure to move the powder, and the material feed mechanism, such as a rotary valve or a screw feeder, that controls the flow rate. The conveying line is designed with appropriate pipe diameters and bends to minimize pressure loss and maintain consistent flow. At the receiving end, a dust collector or a filter may be employed to capture any airborne particles, ensuring environmental compliance and product purity. The intelligent aspect of these systems lies in their ability to adapt to varying material characteristics, such as particle size, density, and moisture content, through programmable logic controllers (PLCs) and advanced algorithms that optimize air pressure, flow rate, and system pressure.
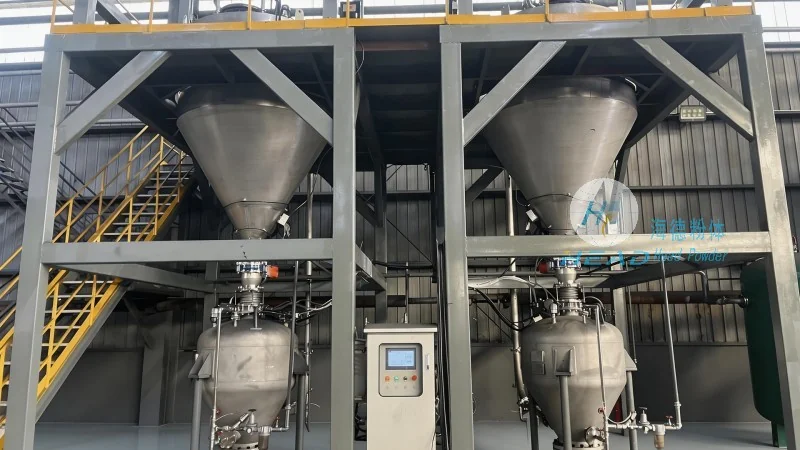
Intelligent powder pneumatic conveying systems find extensive applications across various industries, including pharmaceuticals, food processing, chemical manufacturing, and mining. In the pharmaceutical industry, for instance, these systems are crucial for handling sensitive powders, as they provide a closed-loop system that prevents contamination and cross-contamination, ensuring product quality and regulatory compliance. The food industry benefits from the hygienic design of these systems, which minimizes the risk of microbial growth and maintains the integrity of food products during transport.
In chemical manufacturing, the ability to handle a wide range of powders, from fine chemicals to bulk raw materials, makes these systems versatile. They are particularly useful in processes that require precise dosing and mixing, as the control systems allow for accurate measurement and delivery of materials. The mining sector also utilizes these systems for transporting ore and other mineral powders, where durability and efficiency are paramount. The systems can handle abrasive materials without significant wear and tear, reducing maintenance costs and extending the lifespan of components.
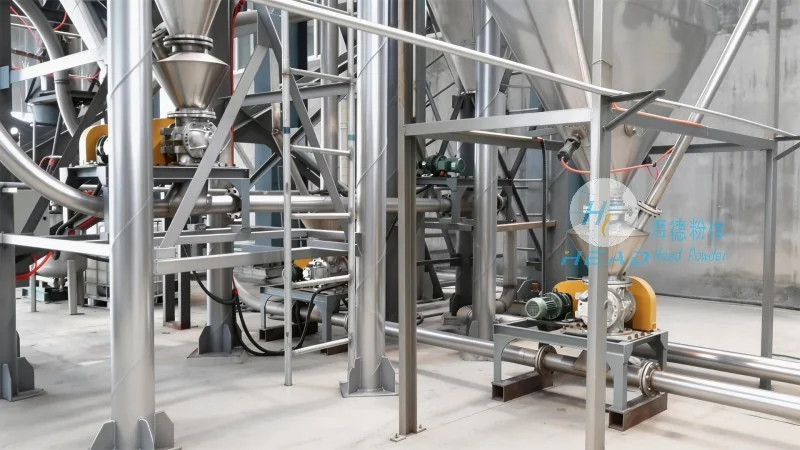
Compared to traditional conveying methods, intelligent powder pneumatic conveying systems offer several advantages. Firstly, they eliminate the need for mechanical components like conveyors or elevators, reducing the risk of material degradation due to friction or impact. This is especially important for delicate or sensitive powders that could be damaged by mechanical handling. Secondly, the closed-loop design prevents dust emissions, enhancing workplace safety and environmental protection. The systems also provide greater flexibility in terms of layout, as the conveying lines can be easily reconfigured to accommodate changes in production processes or facility expansions.
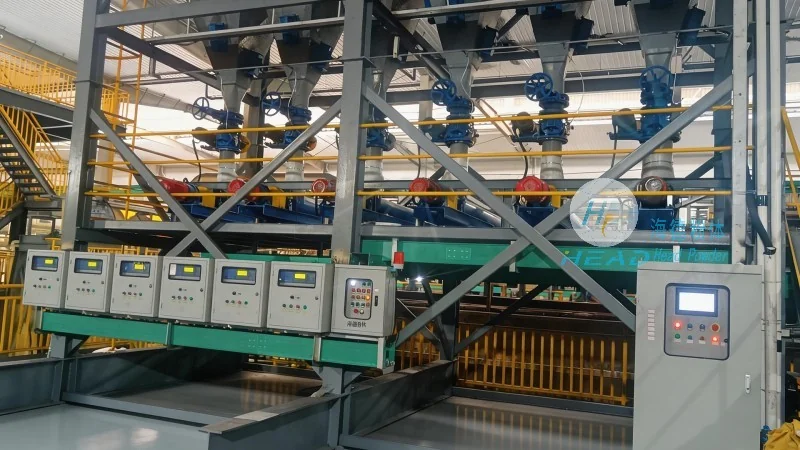
Another significant advantage is the energy efficiency of these systems. Modern intelligent pneumatic conveying systems are designed to operate at lower air pressures and flow rates, reducing energy consumption compared to older, more rudimentary designs. The integration of energy-saving features, such as variable frequency drives (VFDs) and optimized air compressors, further enhances their efficiency. Additionally, the real-time monitoring capabilities allow for predictive maintenance, reducing unexpected breakdowns and increasing overall system uptime.
Intelligent powder pneumatic conveying systems represent a sophisticated solution for the efficient and reliable transport of bulk powders. By leveraging advanced control technologies and flexible design, these systems address the challenges associated with traditional powder handling methods, offering benefits such as improved product quality, enhanced safety, and reduced operational costs. As industries continue to demand higher standards of efficiency and precision, the role of intelligent pneumatic conveying systems is likely to expand, making them an essential component of modern manufacturing and processing operations.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top