HeadPowder, a leading provider in the field of pneumatic conveying technology, specializes in the efficient and reliable transport of rare earth mineral powders. This article provides an in-depth analysis of both negative pressure and positive pressure pneumatic conveying systems, highlighting their technical characteristics, operational principles, and practical applications.
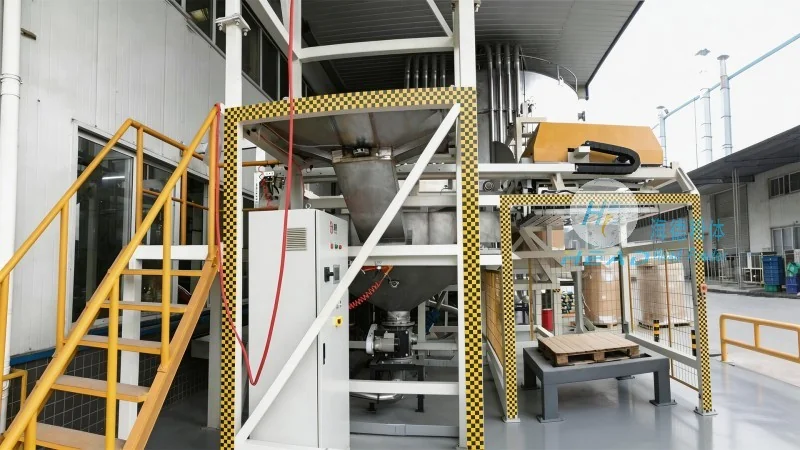
With the increasing demand for rare earth elements in modern industries, such as electronics, renewable energy, and high-tech manufacturing, the efficient handling and transportation of rare earth mineral powders have become critical. Pneumatic conveying offers a solution that minimizes material degradation, reduces labor costs, and enhances process safety compared to traditional methods like belt conveyors or bucket elevators. HeadPowder Engineering Co., Ltd., based in Shandong, China, has been at the forefront of developing advanced pneumatic conveying solutions tailored to the unique challenges of rare earth mineral processing.
Negative pressure (or vacuum) pneumatic conveying systems operate by creating a vacuum at the material pickup point, drawing the powder into the conveying line using air flow. This method is particularly effective for transporting powders over short to medium distances, typically up to several hundred meters, and is well-suited for applications where the material is sensitive to pressure or where the conveying line must be integrated into existing facilities without disrupting operations. The system consists of a vacuum pump, a material hopper, a rotary valve, and a conveying line, with the air flow directed from the material source to the destination, ensuring a clean and controlled transport process.
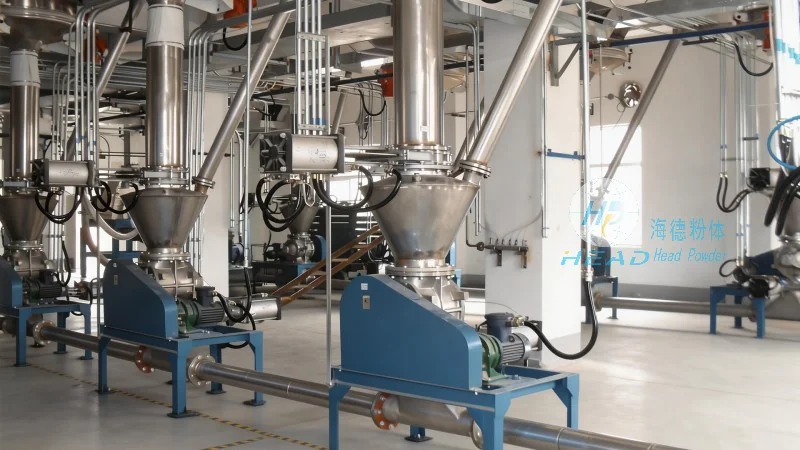
Key advantages of negative pressure systems include their ability to handle fine powders without clogging, their low noise levels, and their suitability for indoor or enclosed environments where dust control is essential. HeadPowder's negative pressure systems are designed with high-efficiency filters and advanced control mechanisms to maintain consistent air quality and prevent material contamination. These systems are commonly used in rare earth processing plants for transporting raw ore, intermediate products, and finished powders between processing stages, ensuring a seamless flow of materials while minimizing downtime and maintenance requirements.
Positive pressure (or pressure) pneumatic conveying systems, in contrast, generate pressure within the conveying line by forcing air through the material, typically using a blower or compressor. This method is ideal for longer distances, often exceeding 1 kilometer, and for transporting bulk quantities of powder. The system includes a material hopper, a rotary valve, a pressure blower, and a conveying line, with air flowing from the blower to the material source, pushing the powder through the line to the destination. Positive pressure systems are more robust and capable of handling a wider range of materials, including abrasive or corrosive powders, making them suitable for heavy-duty industrial applications.
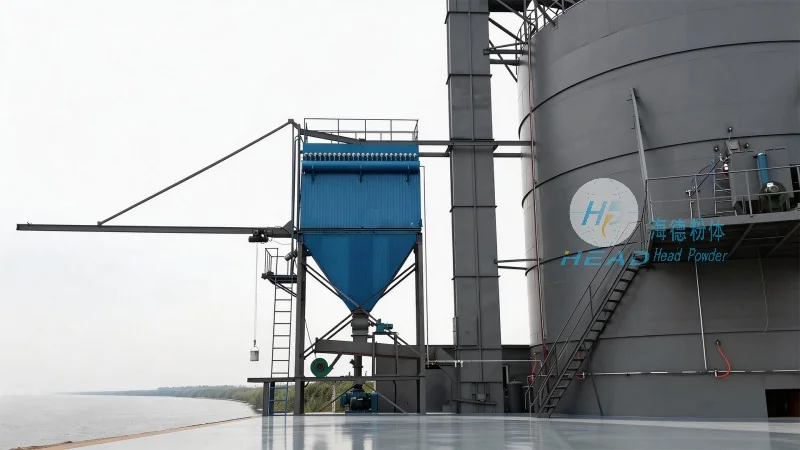
Advantages of positive pressure systems include their higher conveying capacity, ability to handle larger particle sizes, and suitability for outdoor or long-distance transport. HeadPowder's positive pressure solutions incorporate advanced blower technology and flexible hose or pipe systems to accommodate varying conveying distances and material characteristics. These systems are commonly employed in rare earth mining and processing facilities for transporting raw ore from mines to processing plants, or for moving large volumes of finished rare earth powders to storage or shipping facilities. The robust design of HeadPowder's positive pressure systems ensures reliable operation under demanding conditions, with minimal maintenance and high efficiency.
When selecting a pneumatic conveying system for rare earth mineral powders, it is essential to consider the specific requirements of the application, including distance, material properties, and operational environment. Negative pressure systems are generally preferred for shorter distances, indoor use, and for handling fine, sensitive powders, while positive pressure systems are more suitable for longer distances, outdoor applications, and for transporting bulk quantities of abrasive or heavy materials. HeadPowder Engineering Co., Ltd. offers customized solutions that integrate the best features of both systems, allowing clients to optimize their conveying processes based on their unique needs. For example, a rare earth processing plant may use a negative pressure system for transporting fine rare earth oxide powders between grinding and classification stages, while employing a positive pressure system for moving larger volumes of raw ore from the mine to the plant.
HeadPowder has successfully implemented pneumatic conveying systems in numerous rare earth processing facilities across China. One notable case involves a large-scale rare earth mine in Shandong, where the company installed a positive pressure system to transport raw ore from the mine to the processing plant over a distance of 1.5 kilometers. The system, equipped with high-capacity blowers and flexible stainless steel hoses, achieved a conveying rate of 50 tons per hour, significantly improving the plant's production efficiency and reducing material handling costs. Another case involved a rare earth oxide manufacturer that implemented a negative pressure system to transport fine powders between grinding and packaging stages. The system's low-pressure operation and advanced filtration ensured that the powders remained free-flowing and free from contamination, meeting stringent quality standards for export.
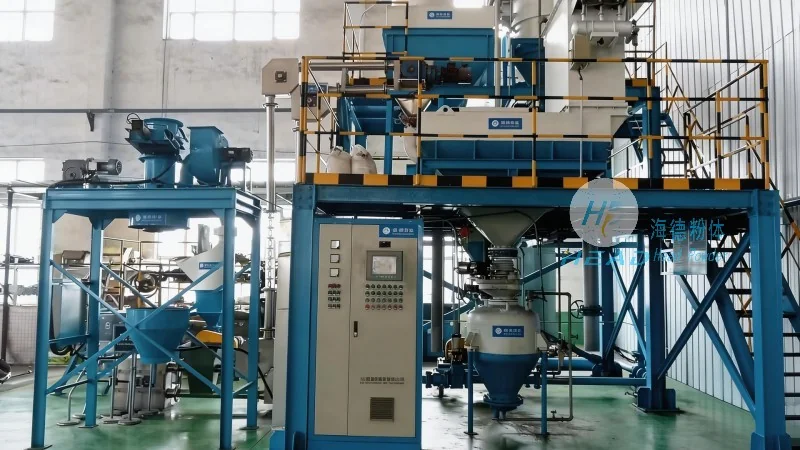
Both negative and positive pressure pneumatic conveying systems offer significant advantages over traditional material handling methods. Negative pressure systems provide a clean, dust-free environment, reducing the risk of occupational health hazards and minimizing the need for extensive dust control measures. Positive pressure systems, on the other hand, offer higher conveying capacities and the ability to handle a wider range of materials, including those with high moisture content or abrasive properties. HeadPowder's systems are designed with energy efficiency in mind, utilizing advanced blower and pump technologies to reduce power consumption while maintaining optimal performance. The company also emphasizes reliability and durability, with components made from high-quality materials such as stainless steel and corrosion-resistant alloys to withstand the harsh conditions of rare earth processing environments.
Pneumatic conveying technology, particularly with the integration of negative and positive pressure systems, plays a crucial role in the efficient and sustainable processing of rare earth minerals. HeadPowder Engineering Co., Ltd., with its expertise in engineering and manufacturing, continues to develop innovative solutions that meet the evolving needs of the rare earth industry. By leveraging advanced materials, control systems, and design principles, HeadPowder ensures that its pneumatic conveying systems not only enhance operational efficiency but also contribute to environmental sustainability by reducing waste and improving process control. As the demand for rare earth elements grows, the importance of reliable and efficient material handling will only increase, making HeadPowder's pneumatic conveying solutions a vital component of modern rare earth processing operations.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top