For industrial applications requiring the precise and clean transport of fine powders, the design and operation of conveying systems are critical to maintaining product integrity and operational efficiency. This article explores the fundamental principles behind purified powder conveying equipment, focusing on mechanisms that ensure minimal contamination and optimal performance across various industrial settings. The solutions are provided by Shandong HeadPowder Engineering Co., Ltd., a leading manufacturer specializing in advanced powder handling technologies.
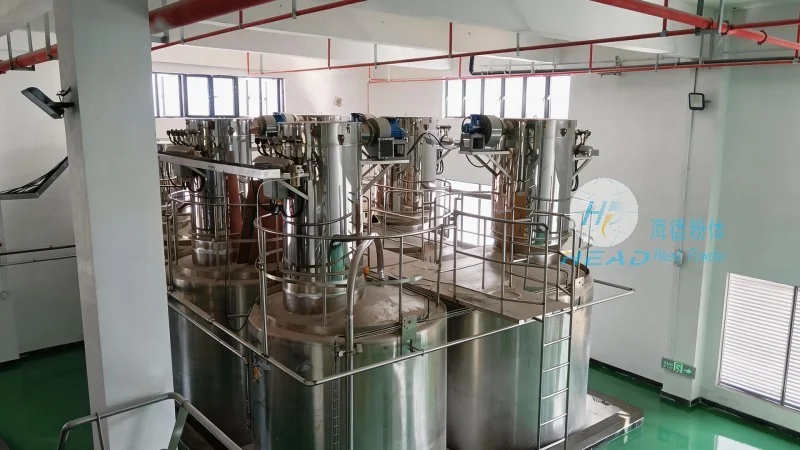
The primary objective of a purified powder conveyor is to move dry, fine materials such as powders, granules, or dust through a system while preventing cross-contamination and maintaining the material's quality. The design typically incorporates sealed systems, specialized components, and controlled environments to achieve these goals. Key principles include the use of airtight enclosures, positive pressure or vacuum systems to control airflow, and materials that are resistant to corrosion and wear. These elements work together to create a closed-loop system that isolates the material from external contaminants, ensuring that the conveyed powder remains pure throughout the process. Shandong HeadPowder Engineering Co., Ltd. specializes in developing such systems that adhere to industry standards for cleanliness and reliability.
Several critical components are integral to the effective operation of purified powder conveying systems. These include the hopper or feed inlet, which provides a controlled entry point for the material; the conveyor mechanism itself, such as a screw, belt, or pneumatic system, which moves the powder through the pipeline; and the discharge outlet, which delivers the material to the next stage of processing. The selection of these components is tailored to the specific characteristics of the powder being conveyed—such as particle size, moisture content, and flowability—to optimize performance and minimize issues like blockages or degradation. Additionally, features like dust collection systems and filtration units are often integrated to further enhance the purity of the conveyed material and protect the environment. The company's expertise lies in customizing these components to meet the unique demands of each application.
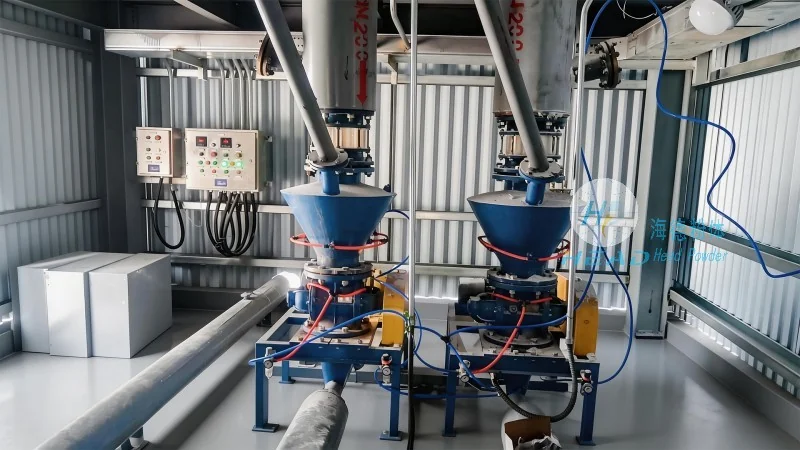
Purified powder conveying systems are widely used across a range of industrial sectors, each with distinct operational requirements and environmental considerations. In pharmaceutical manufacturing, for example, the systems must adhere to stringent regulatory standards for cleanliness and sterility, often operating in controlled environments like cleanrooms. The conveyor design may include HEPA filters and stainless steel components to prevent contamination and ensure product safety. In the food processing industry, the equipment is designed to handle food-grade powders, with materials that are non-toxic and easy to clean, such as food-grade plastics or stainless steel. The working environment may involve high humidity or temperature variations, requiring the conveyor to maintain consistent performance under these conditions. Shandong HeadPowder Engineering Co., Ltd. has extensive experience in providing solutions for these sectors, ensuring compliance with industry regulations.
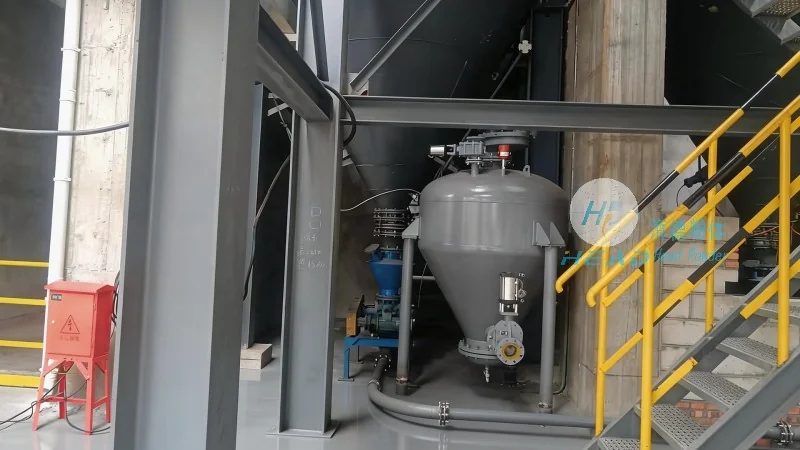
In the chemical and petrochemical sectors, the systems are built to handle abrasive or corrosive powders, with components made from materials like Hastelloy or PTFE to resist wear and chemical attack. The operational environment may involve high temperatures or aggressive chemicals, necessitating robust sealing and insulation to prevent leaks and maintain material purity. Additionally, in the mining and mineral processing industries, purified powder conveyors are used to transport raw materials like ores or minerals, often in large-scale operations. The systems are designed for durability and efficiency, with features like variable speed drives to adjust to changing material flow rates and prevent overloading. The company's engineering team designs systems that are robust enough to handle the demanding conditions of these industries.
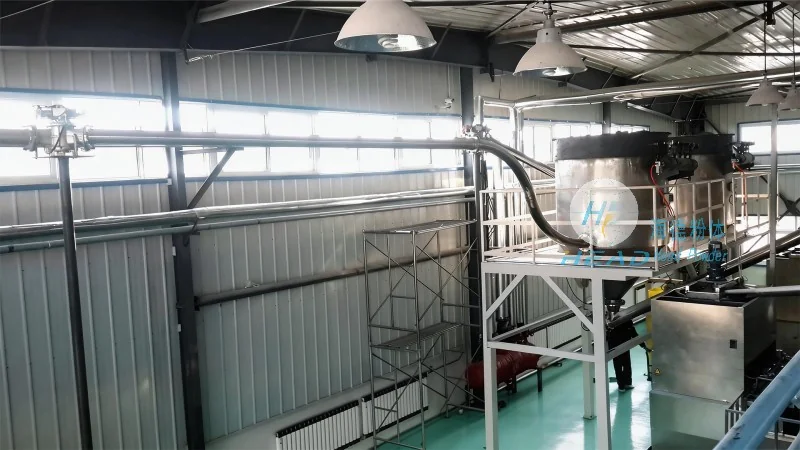
Ensuring the long-term performance and reliability of purified powder conveying systems requires careful attention to operational efficiency and regular maintenance. Proper system design, including the selection of appropriate conveyor speeds and pipeline diameters, helps to minimize energy consumption while maintaining material flow rates. Regular cleaning and maintenance of components, such as the hopper, conveyor screw, and seals, are essential to prevent material buildup and maintain the system's integrity. The use of monitoring systems, such as pressure sensors or flow meters, can help detect issues like blockages or air leaks early, allowing for timely intervention and reducing downtime. Additionally, training operators on proper system operation and maintenance procedures is crucial to ensure that the equipment is used correctly and that any issues are addressed promptly. Shandong HeadPowder Engineering Co., Ltd. offers comprehensive support services, including maintenance plans and operator training, to help clients maximize the lifespan and efficiency of their conveying systems.
Purified powder conveying systems play a vital role in industries where the quality and purity of fine materials are paramount. By adhering to the core principles of sealed systems, controlled airflow, and specialized components, these systems ensure that powders are transported efficiently and without contamination. The working scene characteristics of these systems are tailored to the specific needs of each industry, from pharmaceuticals to food processing and beyond. As industrial demands continue to evolve, the importance of reliable and efficient purified powder conveying equipment will only grow, making it an essential component of modern manufacturing processes. Shandong HeadPowder Engineering Co., Ltd. remains committed to delivering innovative solutions that meet the evolving needs of the industry, ensuring that clients can maintain high standards of product quality and operational efficiency.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top