For industries dealing with powdered stone materials, efficient and reliable material handling is crucial. Pneumatic conveying systems offer a versatile solution for transporting these fine particles over short to medium distances. This article explores the operation process and working principle of such systems, highlighting how they ensure consistent performance and minimal material degradation.
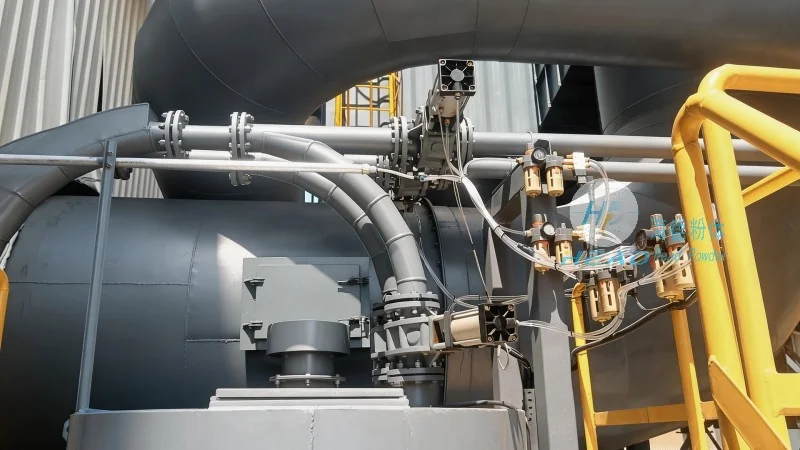
A typical pneumatic conveying system for powdered stone particles consists of several core components. These include a hopper or feeder for material storage and feeding, a conveyor line (often a pipe), a blower or compressor to generate the conveying air, and a receiver or discharge unit. Each component plays a vital role in the overall process, ensuring that the material is moved smoothly and safely.
The operation of a pneumatic conveying system for powdered stone particles involves a series of coordinated steps. First, the powdered stone is fed into the hopper from a storage silo or bulk container. The feeder then regulates the flow rate, ensuring a consistent supply of material into the conveyor line. Next, the blower or compressor creates a high-pressure air stream within the pipe. As the air flows through the pipe, it picks up the stone particles, forming a dense mixture known as a "slurry" or "conveyed stream." The mixture travels through the pipe to the discharge point, where it is separated from the air. Finally, the stone particles are collected in the receiver, while the air is either filtered and recycled or released to the atmosphere.
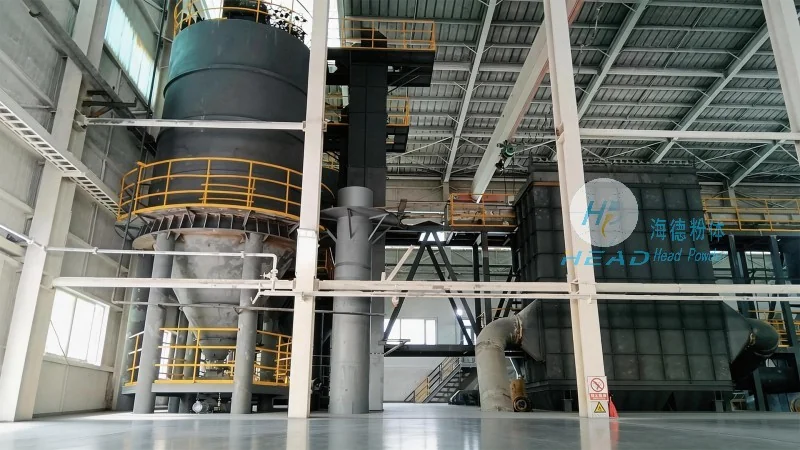
The working principle of pneumatic conveying relies on the interaction between air flow and particle movement. In a positive pressure system, the blower supplies compressed air into the conveyor line, creating a pressure higher than the ambient air. This pressure difference forces the air and particles to move forward. The velocity of the air is critical; it must be sufficient to overcome the gravitational force acting on the particles and any friction within the pipe. The system typically operates at velocities ranging from 20 to 30 meters per second, depending on the particle size and density. The air-particle mixture remains in a suspended state, preventing particle settling and ensuring efficient transport.
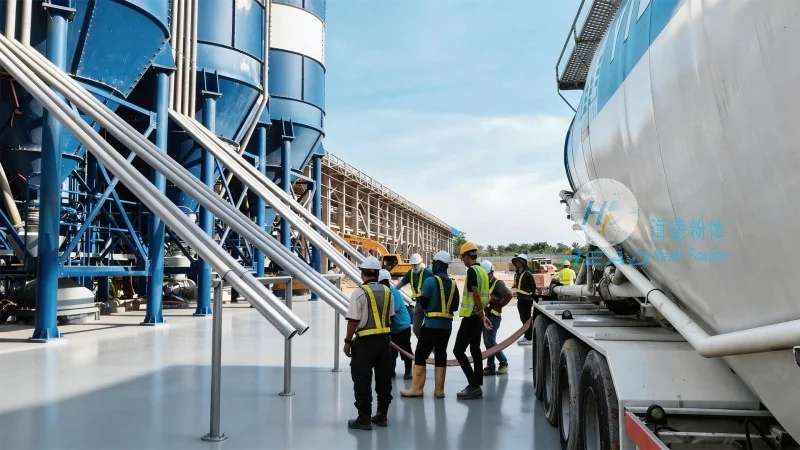
Implementing a pneumatic conveying system for powdered stone offers several advantages. It eliminates the need for mechanical components like belts or buckets, reducing maintenance costs and wear on equipment. The system also minimizes material degradation, as the particles are not subjected to abrasion or impact during transport. Additionally, pneumatic conveying allows for enclosed transport, which helps in controlling dust emissions and maintaining a clean working environment. For industries such as cement, mining, and construction, these benefits translate into improved operational efficiency and product quality.
HeadPowder, or Shandong HeadPowder Engineering Co., Ltd., is a leading provider of engineering solutions for material handling systems. With a focus on innovative and efficient designs, the company specializes in pneumatic conveying equipment tailored to the needs of industries dealing with powdered materials. HeadPowder's expertise lies in designing systems that optimize performance, reduce operational costs, and ensure compliance with industry standards. Based in Shandong, China, the company leverages local manufacturing capabilities and global market knowledge to deliver high-quality solutions to clients worldwide.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top