Shandong HeadPowder Engineering Co., Ltd., a leading provider in the field, specializes in the design, manufacturing, and implementation of advanced pneumatic conveying systems. Among their offerings is the tonne bag pneumatic conveying system, a robust solution tailored for efficient bulk material handling. This system is particularly effective for transporting materials such as powders, granules, and other bulk solids from storage silos or bulk bags to processing units, ensuring seamless and reliable material flow in industrial operations.
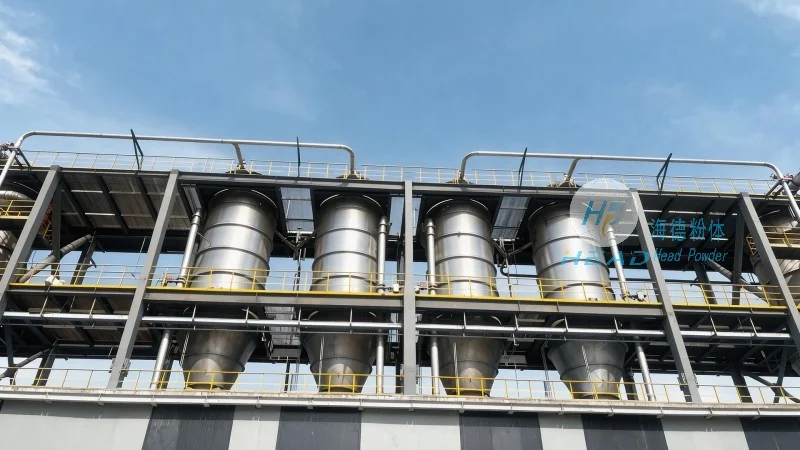
The core of the tonne bag pneumatic conveying system lies in its air-driven mechanism. The system operates by generating a high-pressure air stream, which is then used to lift and transport the material from the source to the destination. The process begins with the material being fed from the tonne bag (or bulk bag) into the conveying line. A series of components, including a hopper, a rotary valve, and a pipeline system, work in tandem to ensure the material is properly introduced and conveyed. The air pressure is carefully controlled to maintain optimal flow rates, preventing material degradation or blockages. This air-driven approach eliminates the need for mechanical components like belts or buckets, reducing maintenance requirements and enhancing operational efficiency.
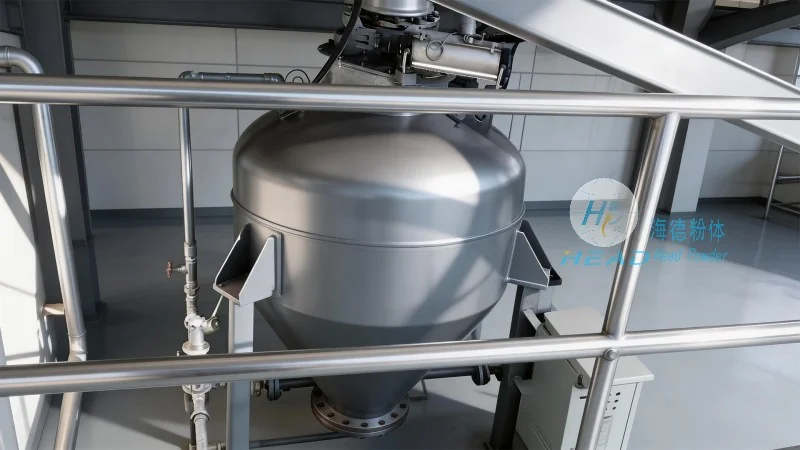
The operation of the tonne bag pneumatic conveying system can be broken down into several key stages, each designed to ensure smooth material transfer. First, the tonne bag is positioned above the system's hopper, allowing the material to be discharged into the hopper through a valve mechanism. The hopper then acts as a buffer, ensuring a consistent flow of material to the conveying line. Next, a rotary valve or feeder controls the rate at which material enters the pipeline, regulating the flow to match the system's capacity. The high-pressure air is then introduced into the pipeline, creating a vacuum or pressure differential that propels the material forward. As the material travels through the pipeline, it is mixed with the air stream, maintaining a stable suspension. Finally, the material is discharged at the receiving end, typically into a storage silo or processing equipment. This entire process is automated, with sensors and controls monitoring pressure, flow, and material levels to ensure continuous and efficient operation.
Several critical components contribute to the effective operation of the tonne bag pneumatic conveying system. The hopper is the initial point of material collection, designed to hold the bulk material from the tonne bag and feed it into the conveying line. The rotary valve or feeder plays a crucial role in controlling the material flow rate, preventing overloading or underflow. The pipeline system, often made of durable materials like stainless steel or plastic, transmits the material and air stream. The air compressor or blower generates the necessary pressure to move the material, with the pressure levels adjusted based on the material's characteristics and the system's length. Additionally, filters and cyclones are used to separate the material from the air at the receiving end, ensuring that the material is delivered in a clean and dry state. These components work together to create a reliable and efficient system that minimizes downtime and maximizes productivity.
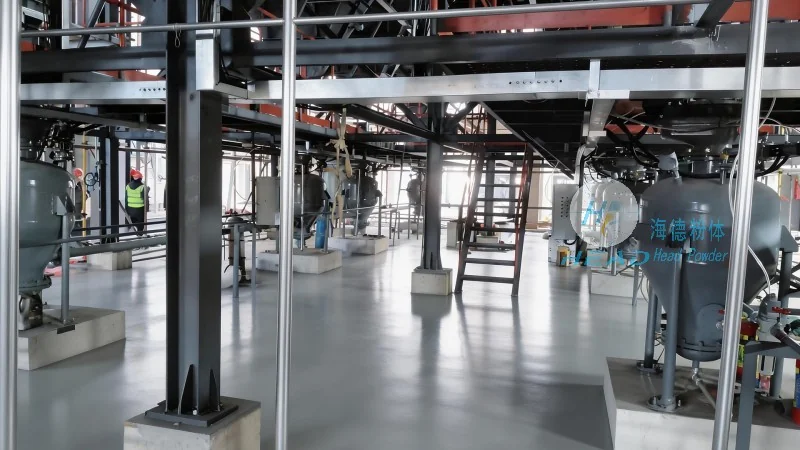
The tonne bag pneumatic conveying system offers several advantages over traditional mechanical conveying methods. Its air-driven operation reduces wear and tear on components, leading to lower maintenance costs and longer equipment life. The system is also highly flexible, capable of transporting materials over long distances and through complex layouts without the need for multiple transfer points. Additionally, it provides a hygienic and dust-free environment, which is particularly important for food, pharmaceutical, and chemical industries where material purity is critical. The system's ability to handle a wide range of materials, from fine powders to coarse granules, makes it suitable for various applications, including chemical processing, food manufacturing, and mining operations. By integrating this technology, industries can achieve improved efficiency, reduced labor costs, and enhanced safety in their material handling processes.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top