HeadPowder, a leading provider in the field, specializes in advanced powder handling solutions. The tonne bag unloading powder conveying system is a critical component for efficient material transfer in various industrial applications. This system is designed to handle bulk powders from tonne bags, ensuring smooth and safe operation. It integrates mechanical and pneumatic technologies to facilitate the seamless transfer of materials, making it an essential tool for industries that rely on bulk powder processing.
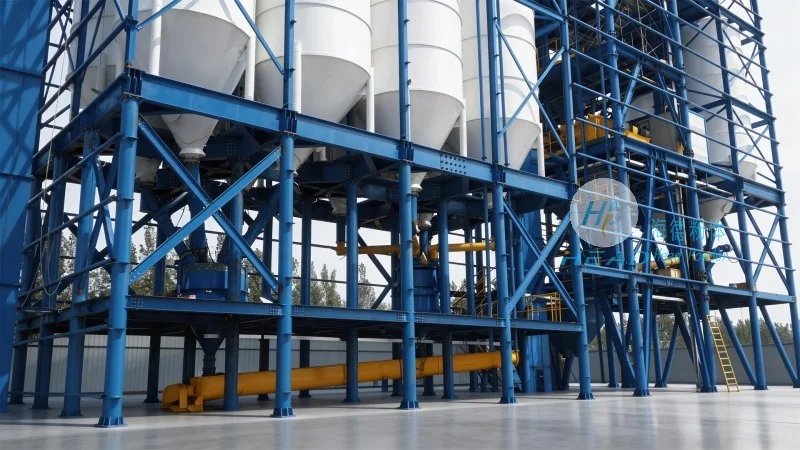
The tonne bag unloading powder conveying system operates on a principle that combines vacuum or pressure-based conveying methods with a robust unloading mechanism. The system typically begins with the placement of a tonne bag onto a support frame or a hopper. The unloading valve, often a pneumatic or electrically actuated device, opens to allow the powder to flow from the bag into the conveying line. For vacuum systems, a suction port draws the powder into the system, while pressure systems use compressed air to push the material through the pipeline. The design ensures that the material is transferred without degradation, maintaining its quality and consistency. The system may include components such as a filter, a silencer, and a control panel to regulate the flow and pressure, ensuring optimal performance.
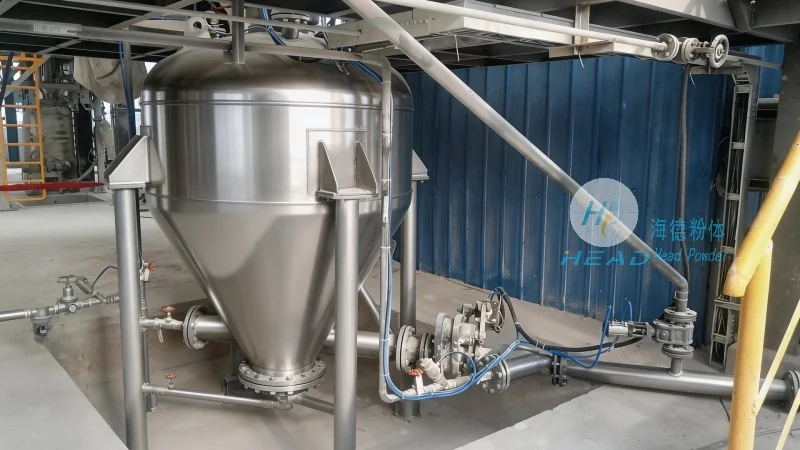
The working scene characteristics of the tonne bag unloading powder conveying system are tailored to meet the diverse needs of industrial environments. These systems are commonly used in sectors such as pharmaceuticals, food processing, chemical manufacturing, and mining. In pharmaceutical applications, the system must adhere to stringent hygiene standards, ensuring that the powders are handled in a sterile environment. The design incorporates features like stainless steel construction and easy-to-clean components to meet these requirements. In food processing, the system is designed to handle food-grade materials, with components that are non-toxic and resistant to corrosion. The working scene also includes considerations for space efficiency, as many industrial facilities have limited floor space. The system is often compact and modular, allowing for easy installation and integration into existing production lines. Additionally, the system is designed for high reliability and low maintenance, ensuring continuous operation with minimal downtime. The working scene characteristics also include the ability to handle different bag sizes and types, from standard tonne bags to custom-made containers. This flexibility allows the system to adapt to various production needs and material specifications.
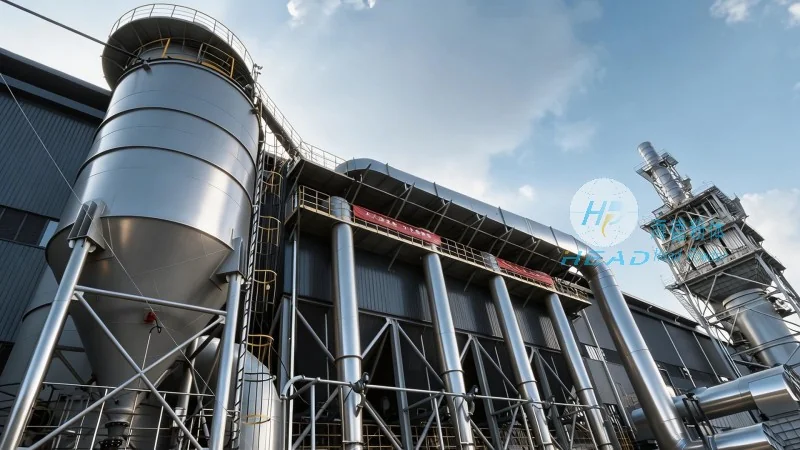
The tonne bag unloading powder conveying system from HeadPowder offers several key features that enhance its performance and usability. One of the primary benefits is its ability to handle large quantities of bulk powders efficiently, reducing the time and labor required for material transfer. The system is designed to minimize dust generation, which is crucial for maintaining a clean and safe working environment. The use of advanced materials and construction techniques ensures durability and long-term reliability. Another important feature is the system's adaptability, allowing it to be customized to meet specific operational requirements. This includes options for different conveying speeds, material types, and bag sizes. The system also includes safety features such as overload protection and emergency stop buttons, ensuring the safety of operators and equipment. The benefits of using this system extend beyond efficiency, as it also helps in maintaining the quality of the powders by preventing contamination and degradation.
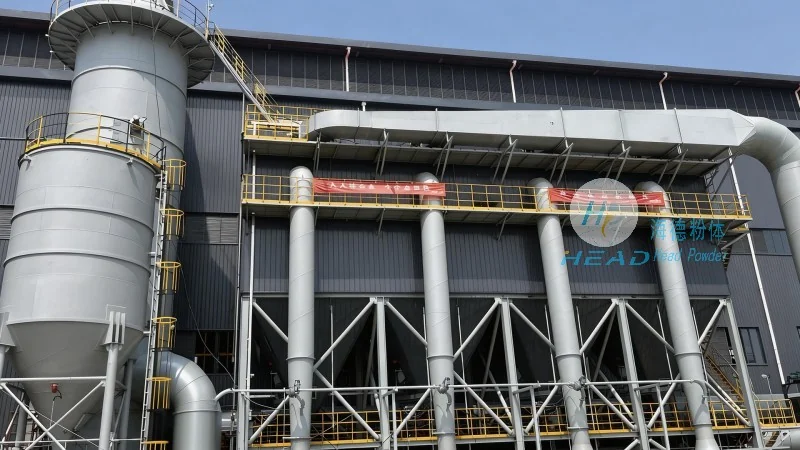
The tonne bag unloading powder conveying system is widely used in various industrial applications. For example, in a pharmaceutical factory, the system is used to transfer raw materials such as powders and granules from tonne bags into storage silos or processing equipment. The system ensures that the materials are handled hygienically and efficiently, meeting the strict regulations of the pharmaceutical industry. In a food processing plant, the system is used to transfer ingredients like flour, sugar, and spices from bulk bags into mixing or packaging equipment. The system's ability to handle food-grade materials and maintain cleanliness is essential for meeting food safety standards. In a chemical manufacturing facility, the system is used to transfer chemicals and reagents from tonne bags into reactors or storage tanks. The system's robust design and ability to handle corrosive materials make it suitable for such applications. In mining operations, the system is used to transfer ore and other minerals from bulk bags into processing equipment. The system's high capacity and reliability are crucial for meeting the demands of mining operations.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top