Cereal pneumatic conveying systems represent a sophisticated approach to material handling, particularly for bulk materials like cereals. These systems utilize air as the primary transport medium, enabling the efficient movement of products over significant distances. The technology has evolved to address the challenges of traditional conveying methods, such as mechanical belts or buckets, by offering a more flexible and adaptable solution for industrial applications.
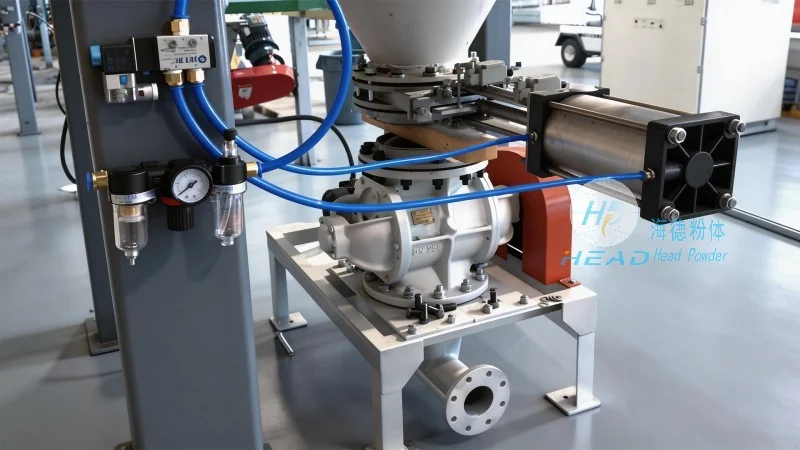
At the heart of cereal pneumatic conveying is the use of compressed air to create a flow that propels the material through a pipeline. This process involves several key components, including a blower or air compressor, a hopper for material storage, and a series of pipes with appropriate fittings. The system operates by drawing material from the hopper into the air stream, which then carries the product to the destination point. This method is particularly effective for handling fine or powdery materials, as it minimizes product degradation and loss compared to other methods.
One of the most significant advantages of modern cereal pneumatic conveying systems is their ability to overcome traditional distance limitations. Traditional mechanical conveyors often struggle with long-distance transport, as they require multiple drives and support structures. In contrast, pneumatic systems can transport materials over hundreds of meters or even kilometers with a single or a few connected pipelines. This capability is achieved through optimized air pressure management and the use of high-efficiency blower technology, which ensures consistent material flow without excessive energy consumption.
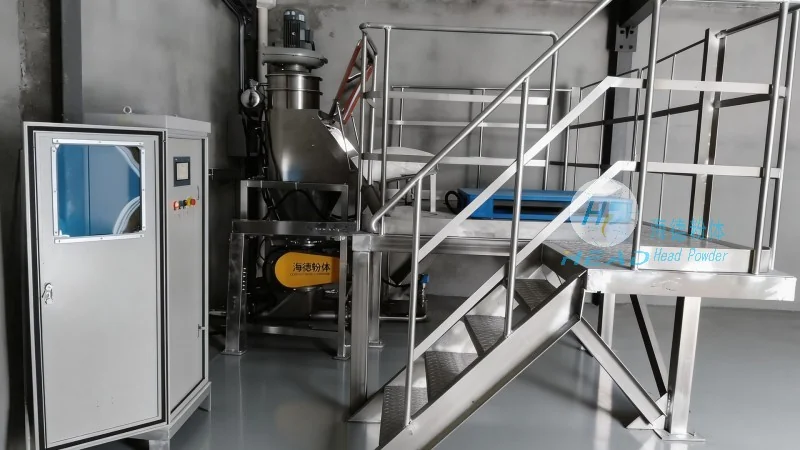
The application of pneumatic conveying in the cereal industry is widespread, covering various stages from raw material handling to finished product distribution. For instance, in a cereal manufacturing plant, the system can be used to transport raw grains from storage silos to processing lines, ensuring a continuous and clean supply. Similarly, during the packaging phase, the system can move finished cereal products from production lines to storage or shipping areas. The technology is also suitable for handling different types of cereals, including wheat, oats, and corn, adapting to the varying particle sizes and densities of each product.
Compared to traditional conveying methods, cereal pneumatic conveying offers several distinct advantages. Firstly, it provides a hygienic and clean environment, which is crucial for food products like cereals. The enclosed pipeline system prevents contamination from external sources and reduces the risk of product spoilage. Secondly, the system is highly flexible, allowing for easy reconfiguration or expansion as production needs change. This adaptability is particularly valuable in dynamic manufacturing environments where production volumes or product lines may shift. Thirdly, pneumatic conveying reduces labor costs and operational complexity, as it eliminates the need for manual handling or frequent maintenance of mechanical components.
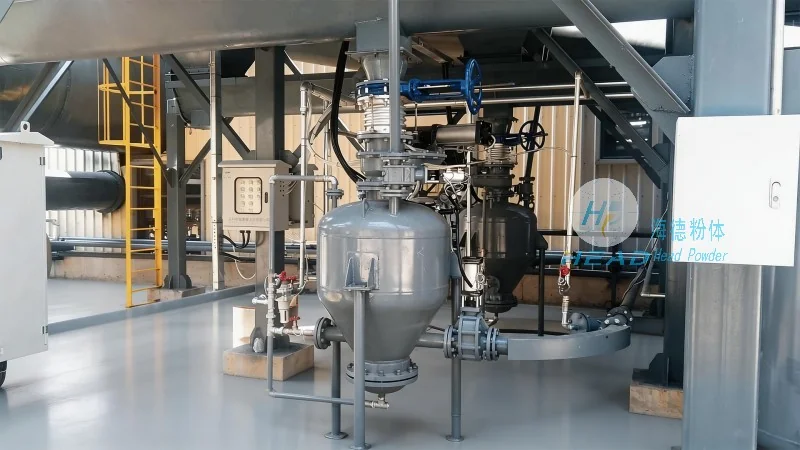
Shandong HeadPowder Engineering Co., Ltd., commonly known as HeadPowder, is a prominent provider of advanced pneumatic conveying systems tailored for the cereal industry. With a focus on innovation and customer-centric solutions, HeadPowder has developed a range of products designed to meet the specific needs of cereal manufacturers. The company’s expertise lies in customizing systems to ensure optimal performance, energy efficiency, and compliance with industry standards. By leveraging cutting-edge technology and rigorous testing, HeadPowder ensures that its systems deliver reliable and consistent material handling, helping clients improve operational efficiency and product quality.
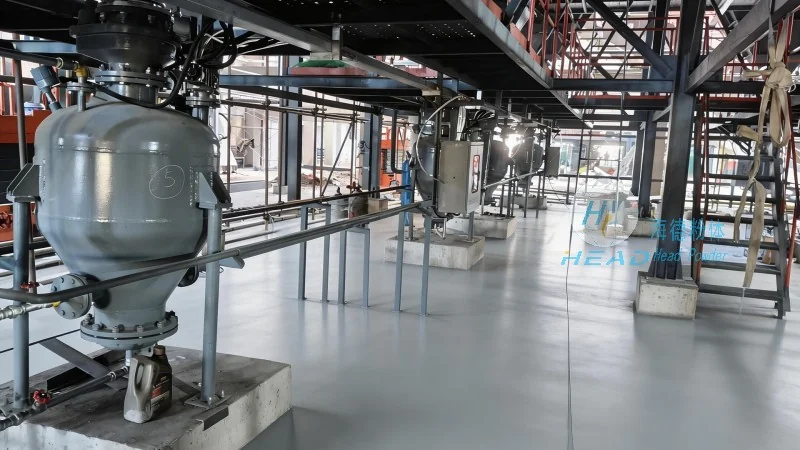
HeadPowder understands that each cereal processing facility has unique requirements, and thus offers comprehensive customization options for its pneumatic conveying systems. This includes the design of specialized hoppers, adjustable air pressure controls, and integrated monitoring systems to track material flow and system performance. The company works closely with clients to assess their specific production processes, material characteristics, and operational goals, ensuring that the final solution is both effective and cost-efficient. Additionally, HeadPowder provides installation and maintenance services to support clients throughout the lifecycle of their equipment, ensuring long-term reliability and performance.
As the cereal industry continues to evolve, the demand for efficient and reliable material handling solutions remains high. Pneumatic conveying, with its ability to overcome distance limitations and offer superior performance, is poised to play an increasingly important role in modern cereal processing. Companies like Shandong HeadPowder Engineering Co., Ltd. are at the forefront of this technological advancement, providing innovative solutions that enhance productivity and product quality. By investing in advanced pneumatic conveying systems, cereal manufacturers can achieve greater operational efficiency, reduce costs, and maintain the high standards required in the food industry.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top