HeadPowder, a leading provider of industrial material handling solutions, specializes in advanced pneumatic conveying systems designed to meet diverse material transport needs. This article explores the core principles and operational characteristics of multi-hopper pneumatic conveying systems, highlighting their applications and benefits in various industrial settings.
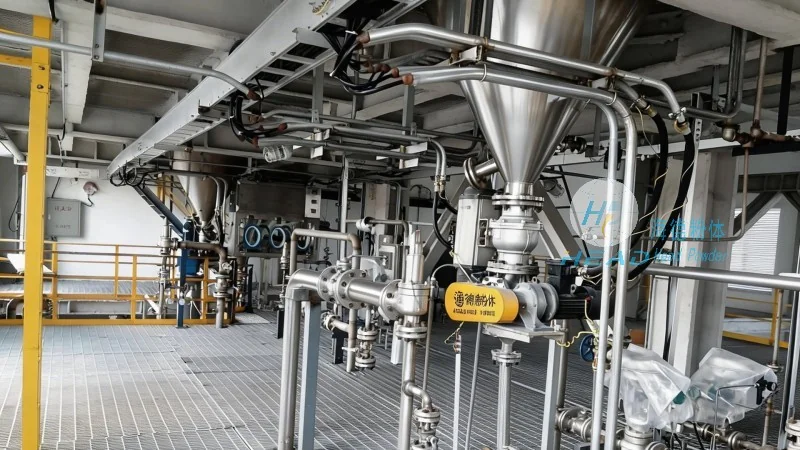
HeadPowder, formally known as Shandong HeadPowder Engineering Co., Ltd., is headquartered in Shandong, China. The company has established itself as a trusted partner in the field of material handling technology, delivering innovative solutions that enhance efficiency and reliability in bulk material transport. With a focus on research and development, HeadPowder continuously improves its systems to address the evolving demands of modern industries.
Multi-hopper pneumatic conveying systems represent a sophisticated approach to transporting bulk powders and granules over long distances or within complex layouts. These systems are designed with multiple hoppers that allow for the sequential or simultaneous discharge of different materials, enabling precise control over the flow and composition of the conveyed product. The core principle involves using compressed air or other gases to create a pressure differential that propels the material through a network of pipes and ducts.
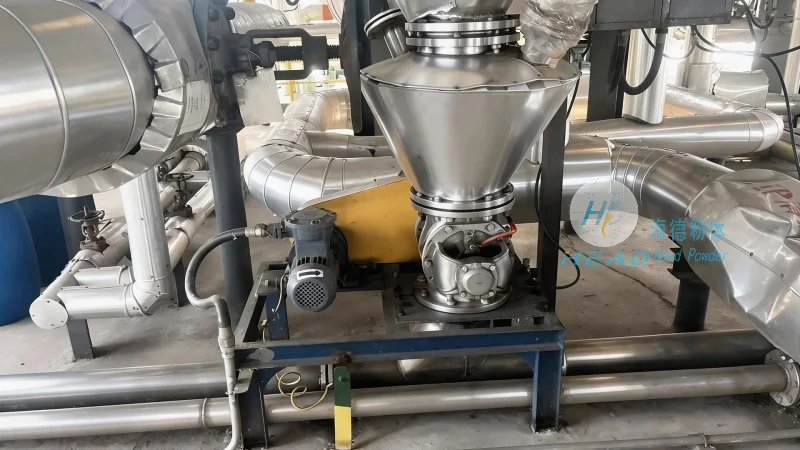
The operation of a multi-hopper system begins with the loading of each hopper with the respective material. Once loaded, the system activates the air supply, which generates a vacuum or pressure within the conveying line. This air flow entrains the material particles, forming a slurry that moves through the system. The multi-hopper design allows for the independent control of each hopper's discharge, enabling the system to handle multiple product types or grades without cross-contamination. Key components include hoppers, airlocks, filters, and control valves, all working in tandem to ensure smooth and efficient material transport.
Multi-hopper pneumatic conveying systems offer several advantages that make them suitable for a wide range of applications. These include the ability to handle a variety of materials, from fine powders to coarse granules, with minimal degradation. The system's modular design allows for easy expansion or modification to accommodate changing production requirements. Additionally, the enclosed nature of the system prevents dust emissions and maintains product purity, which is critical in industries such as pharmaceuticals, food processing, and chemical manufacturing. The precise control over material flow also reduces waste and improves overall operational efficiency.
The working scene characteristics of multi-hopper systems vary based on the industry and specific application. In the chemical industry, for example, these systems are used to transport reactive powders or hazardous materials, where containment and safety are paramount. The multi-hopper design allows for the segregation of different chemical grades, preventing cross-contamination and ensuring compliance with safety regulations. In the food and beverage sector, the systems are employed to handle ingredients like flour, sugar, or spices, where hygiene and product integrity are critical. The enclosed conveying process maintains the quality of the food products, while the modular design allows for easy cleaning and maintenance.
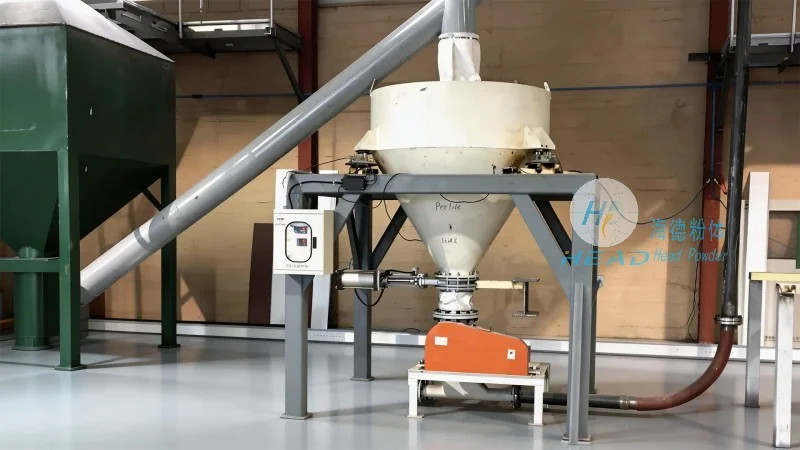
Multi-hopper pneumatic conveying systems find applications across multiple industries, each with unique requirements. In the mining and minerals sector, they are used to transport raw materials from storage silos to processing facilities, enabling efficient material handling in large-scale operations. The system's ability to handle abrasive materials and high volumes makes it ideal for this industry. In the pharmaceutical industry, the systems are used to transport active pharmaceutical ingredients (APIs) and excipients, where the strictest standards of purity and contamination control are required. The multi-hopper design allows for the segregation of different drug formulations, ensuring that each product is handled separately and without cross-contamination. In the agricultural sector, these systems are used to transport fertilizers, seeds, or animal feed, improving the efficiency of material distribution in farms and processing plants.
Multi-hopper pneumatic conveying systems, as exemplified by the solutions offered by Shandong HeadPowder Engineering Co., Ltd., represent a highly effective and versatile method for bulk material transport. By leveraging advanced engineering and modular design, these systems provide reliable, efficient, and safe material handling solutions for diverse industrial applications. The principles and characteristics discussed in this article highlight the importance of such systems in modern industrial operations, where efficiency, product quality, and safety are paramount.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top