Understanding the working principle and features of a pulverized fly ash material pneumatic conveying system is crucial for industries dealing with the efficient handling of this specific type of material. This article provides a detailed overview of how such equipment operates and its key characteristics, tailored for applications involving the transportation of pulverized fly ash from sources like power plants to processing or disposal sites.
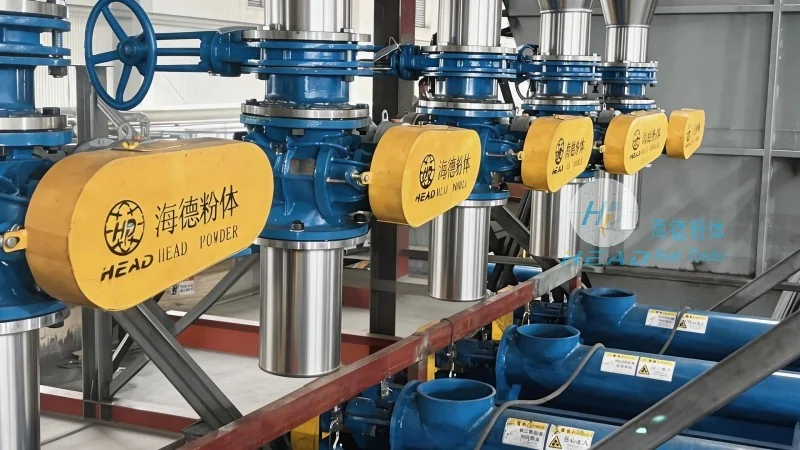
The core mechanism of a pulverized fly ash pneumatic conveying system involves the use of air pressure to transport dry, fine particles through a pipeline. The process typically begins with the material being fed into a hopper or feeder, where it is then introduced into a high-pressure air stream. As the air flows through the pipeline, it entrains the fly ash particles, creating a slurry-like mixture that moves along the system. The equipment may include components such as a blower or compressor to generate the necessary air pressure, a filter system to capture any fine particles that escape the pipeline, and a control unit to regulate the flow rate and pressure. The design of the system is optimized to minimize particle degradation and ensure consistent flow, which is essential for maintaining the quality of the fly ash during transportation.
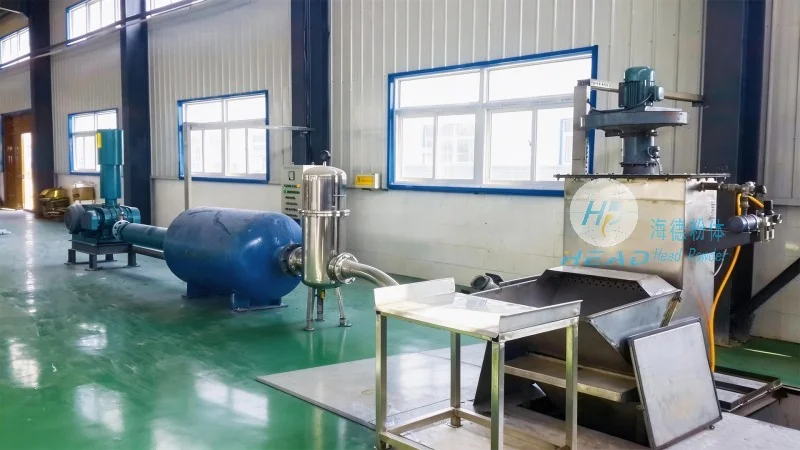
Several notable features distinguish effective pulverized fly ash pneumatic conveying systems. Firstly, the system is designed for low maintenance and high reliability, with components engineered to withstand the abrasive nature of fly ash particles. This includes the use of corrosion-resistant materials for the pipeline and hopper to prevent wear and extend the equipment's lifespan. Secondly, the conveying system offers flexibility in terms of layout, allowing for horizontal, vertical, or combined horizontal-vertical configurations to accommodate different site topographies and material handling requirements. Thirdly, advanced control systems are integrated to monitor and adjust the air pressure, flow rate, and particle concentration in real-time, ensuring optimal performance and preventing system failures. Additionally, the equipment is equipped with safety features such as pressure relief valves and particle detection sensors to protect both the system and personnel from potential hazards.
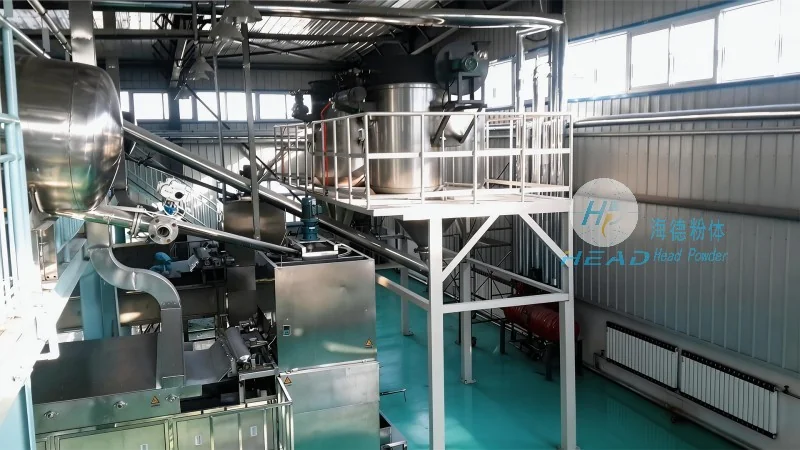
Pulverized fly ash, a byproduct of coal combustion, is widely used in construction and industrial applications due to its pozzolanic properties. The pneumatic conveying equipment developed by Shandong HeadPowder Engineering Co., Ltd. is specifically designed to handle this material efficiently, ensuring minimal loss and contamination during transport. The benefits of using such a system include reduced labor costs, as automated feeding and conveying eliminate the need for manual handling, and improved safety by minimizing exposure to dust and particles. Furthermore, the system's ability to transport fly ash over long distances without the need for intermediate storage points enhances operational efficiency and reduces environmental impact by preventing the accumulation of waste material at source locations.
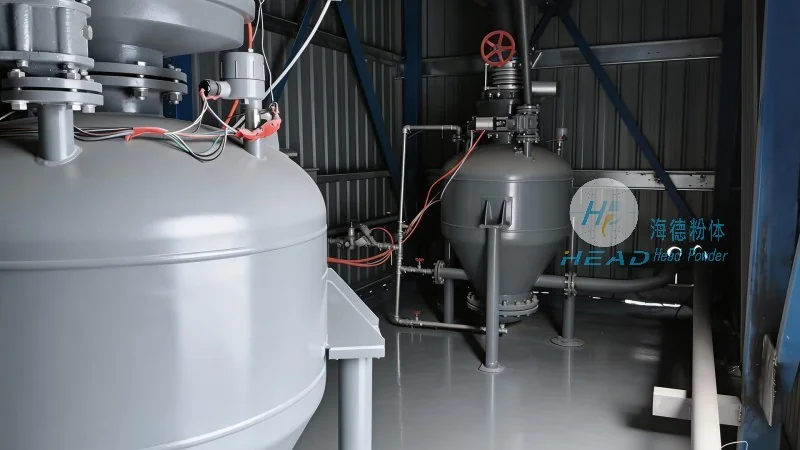
In summary, the working principle and features of pulverized fly ash material pneumatic conveying equipment involve sophisticated air pressure management and material handling technology. The systems are engineered to provide reliable, low-maintenance operation while addressing the unique challenges of transporting fine, abrasive materials like fly ash. Shandong HeadPowder Engineering Co., Ltd., based in Shandong, China, specializes in the design and manufacturing of such equipment, leveraging years of experience to deliver solutions that meet the demands of modern industrial applications. By focusing on efficiency, safety, and durability, these systems play a critical role in the sustainable handling of fly ash, supporting industries in their efforts to minimize waste and maximize resource utilization.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top