Cement raw material powder conveying systems are critical components in the production of cement, ensuring the efficient and reliable transport of raw materials such as limestone, clay, and iron ore from storage to processing units. These systems are designed to handle large volumes of fine powders with high precision, supporting the overall productivity and quality of cement manufacturing operations.
HeadPowder, a leading engineering firm based in Shandong, China, specializes in the design, manufacturing, and installation of advanced powder handling solutions. With a strong commitment to innovation and quality, HeadPowder has established itself as a trusted partner for cement and other industrial sectors, delivering customized conveying systems that meet stringent operational requirements.
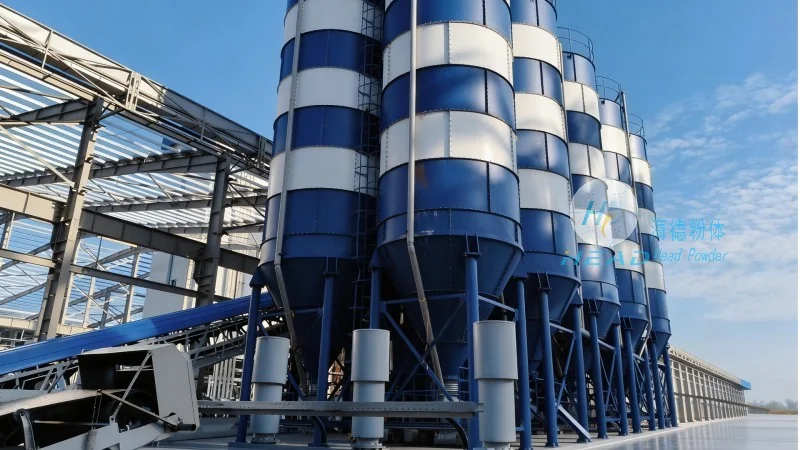
The cement raw material powder conveying system typically consists of several key components, each playing a vital role in the overall operation. These include raw material storage silos, feeders, conveyors (such as pneumatic or mechanical systems), and control panels. The storage silos are used to hold bulk raw materials, while feeders regulate the flow rate to the conveyor. The conveyor itself transports the powders to the processing units, with control panels monitoring and adjusting the system parameters for optimal performance.
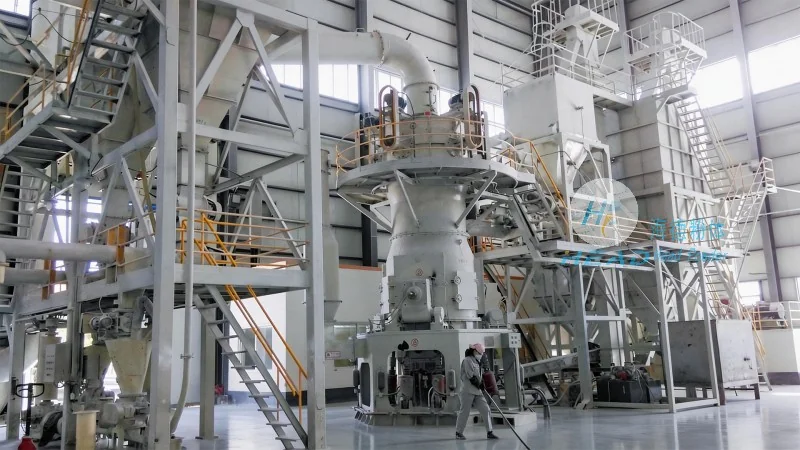
The operation process of the cement raw material powder conveying system begins with the loading of raw materials into the storage silos. Once the silos are filled, the feeders start to discharge the materials at a controlled rate. The powders then enter the conveyor system, which may use air pressure (pneumatic) or mechanical force (e.g., screw conveyors) to move the material. The conveyor transports the raw materials to the cement production line, where they are further processed into clinker and then cement. Throughout the process, the control system continuously monitors parameters such as flow rate, pressure, and temperature to ensure stable and efficient operation.
The working principle of the cement raw material powder conveying system is based on the principles of fluidization and pneumatic transport. In pneumatic systems, raw materials are lifted and transported by a stream of air, which creates a suspension of particles. The air flow is controlled by fans and ducts, ensuring that the powders are moved efficiently without clogging. Mechanical conveyors, on the other hand, use rotating components (such as screws or belts) to push the material forward. Both systems rely on precise control mechanisms to maintain consistent flow rates and prevent material degradation or loss.
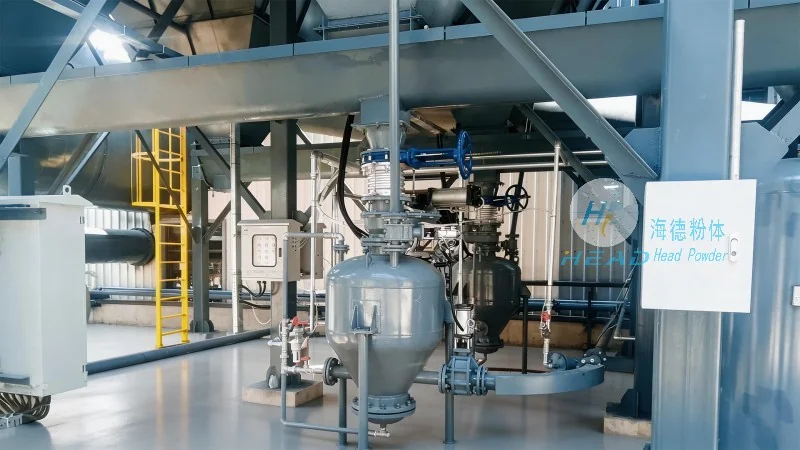
HeadPowder's cement raw material powder conveying systems offer several advantages, including high efficiency, low maintenance costs, and the ability to handle a wide range of raw materials. The systems are designed to minimize dust emissions and ensure environmental compliance, making them suitable for modern cement plants. Technical specifications vary based on the specific application, but typical systems can handle capacities ranging from 10 to 500 tons per hour, with adjustable flow rates to match production demands. The use of advanced materials and corrosion-resistant components ensures long-term durability and reliability.
In conclusion, the cement raw material powder conveying system is a critical technology in the cement industry, enabling the efficient transport of raw materials from storage to processing. HeadPowder's expertise in designing and implementing these systems ensures that cement manufacturers can achieve high productivity, consistent quality, and operational efficiency. By leveraging advanced engineering and quality control, HeadPowder continues to provide reliable solutions that meet the evolving needs of the cement industry.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top