Understanding the operation process and working principle of a cobalt hydroxide powder conveying system is crucial for optimizing material handling in industrial applications. This system is designed to efficiently transport cobalt hydroxide powder, a key component in various industries such as battery manufacturing and chemical processing. The following sections will delve into the detailed operation process and the underlying working principles of this system, providing insights into its functionality and benefits.
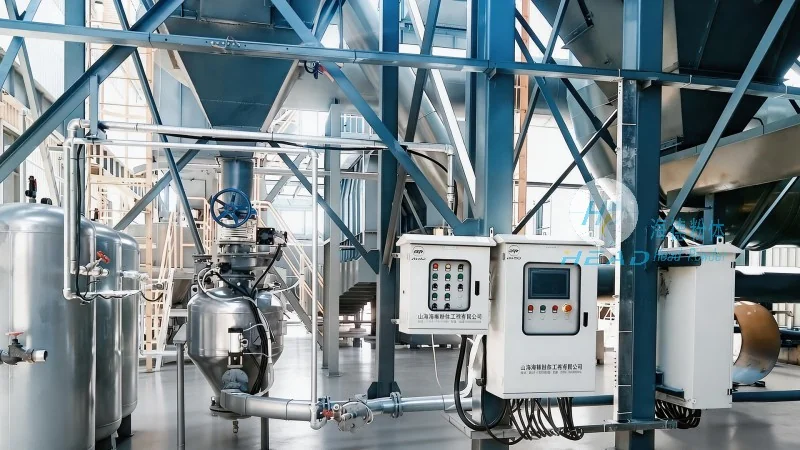
Cobalt hydroxide is a fine powder with specific properties that require specialized handling to prevent agglomeration and ensure consistent flow. The conveying system developed by Shandong HeadPowder Engineering Co., Ltd. addresses these challenges by integrating advanced technologies and robust design. The system is tailored to meet the demands of high-purity material transport, maintaining the integrity of the cobalt hydroxide powder throughout the conveying process. HeadPowder, a leading manufacturer in this field, has leveraged years of experience to create a reliable solution that enhances productivity and reduces operational costs for clients in China and beyond.
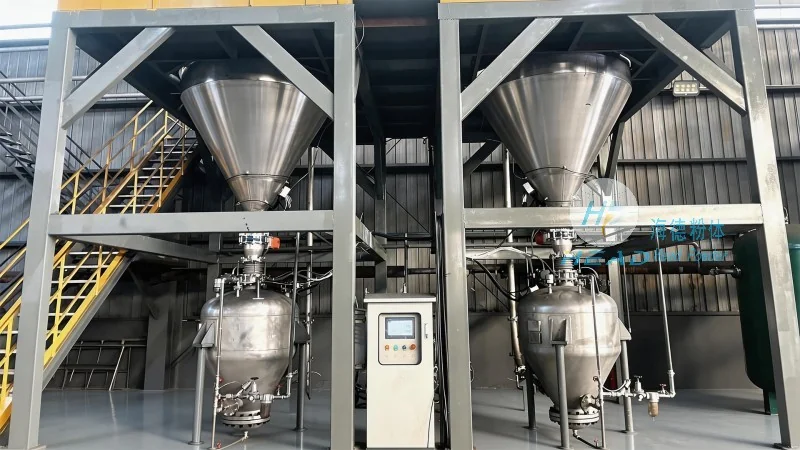
The cobalt hydroxide powder conveying system consists of several critical components, each playing a vital role in the overall operation. These components include a hopper for material storage, a feeding mechanism to control the flow rate, a conveying pipeline (often using pneumatic or mechanical methods), and a discharge unit for delivering the powder to the target location. The hopper is designed with a smooth interior surface to minimize powder buildup and ensure uniform feeding. The feeding mechanism, typically a rotary valve or a screw feeder, regulates the amount of powder entering the pipeline, preventing overloading and maintaining a steady flow. The conveying pipeline may utilize air pressure (pneumatic conveying) or mechanical force (e.g., screw conveyors or belt conveyors) to move the powder. The discharge unit, such as a rotary valve or a bagging machine, ensures the powder is released in a controlled manner, avoiding spills and maintaining safety standards.
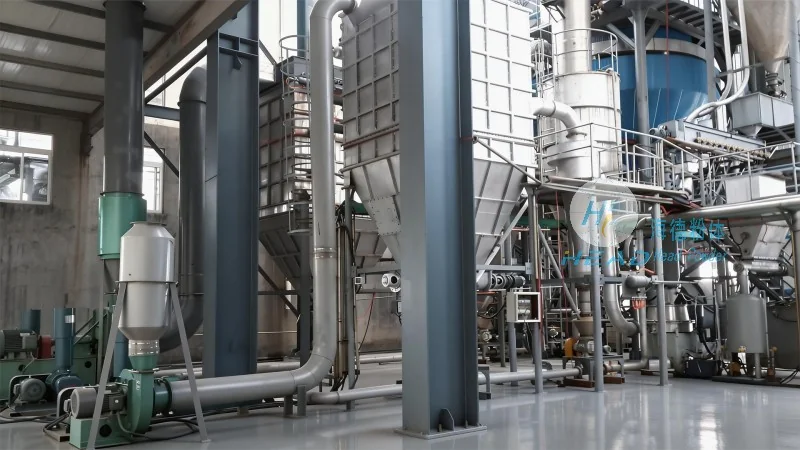
The operation of the cobalt hydroxide powder conveying system follows a systematic sequence of steps to ensure efficient and safe material transport. The process begins with the loading of cobalt hydroxide powder into the hopper. The powder is then fed into the conveying pipeline through the controlled feeding mechanism. Depending on the chosen conveying method (pneumatic or mechanical), the powder is propelled through the pipeline to the discharge point. In pneumatic conveying systems, compressed air is used to create a flow that carries the powder particles. Mechanical conveyors, on the other hand, rely on rotating components to move the powder along the pipeline. The system is equipped with sensors and control systems to monitor the flow rate, pressure, and other parameters, allowing for real-time adjustments to maintain optimal performance. The discharge unit then receives the powder and delivers it to the next stage of processing or storage. Throughout the operation, the system is designed to minimize dust generation and ensure compliance with environmental and safety regulations.
The working principle of the cobalt hydroxide powder conveying system is based on the principles of fluid dynamics and mechanical motion. In pneumatic conveying systems, the system uses compressed air to create a flow that entrains the powder particles, transporting them through the pipeline. The air velocity is carefully controlled to ensure that the powder particles are carried without causing excessive wear or damage to the pipeline. The pressure drop along the pipeline is managed to maintain a consistent flow rate, preventing blockages or uneven distribution. In mechanical conveying systems, the principle of continuous motion is applied, where rotating screws or belts move the powder along the pipeline. The design of the conveying components, such as the pitch and diameter of the screws, is optimized to handle the specific characteristics of cobalt hydroxide powder, ensuring smooth and efficient transport. The system also incorporates features like airlocks and filters to prevent dust leakage and maintain a clean working environment. The control system integrates sensors to monitor the system's performance, providing feedback to adjust the operation parameters as needed. This ensures that the conveying process is efficient, reliable, and safe, meeting the high standards required for handling cobalt hydroxide powder.
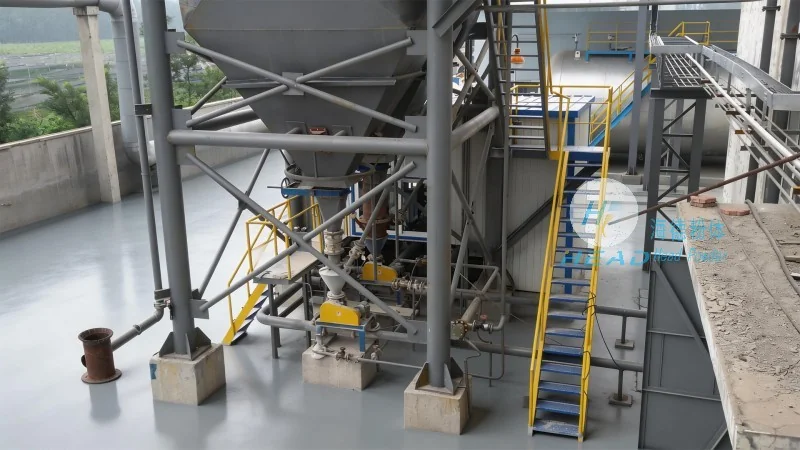
The cobalt hydroxide powder conveying system offers several benefits that make it an ideal choice for industrial applications. One of the primary advantages is its ability to handle fine powders without causing agglomeration or degradation, which is critical for maintaining the quality of the material. The system's design minimizes dust generation, reducing the risk of inhalation hazards and improving workplace safety. Additionally, the system enhances productivity by providing a continuous and consistent flow of powder, reducing downtime and increasing throughput. The modular design of the system allows for easy integration into existing production lines, making it a flexible solution for various processing needs. The system is widely used in the battery manufacturing industry, where cobalt hydroxide is a key component in lithium-ion batteries. It is also applicable in chemical processing plants, where the powder is used as a catalyst or in the production of other chemical compounds. The system's reliability and efficiency make it a preferred choice for companies seeking to optimize their material handling processes and improve overall operational performance.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top