Deeply engaged in industrial bulk material scenarios, providing integrated intelligent environmental solutions for automatic batching, centralized feeding, dry desulfurization and denitrification!
Your current position:首页 >> News >> Technical Q&A

Operation Process and Working Principle of Expanded Perlite Powder Conveying System

Release time:2026-09-20 16:01:37
name of the company:Shandong Headpowder Engineering Co., Ltd.
telephone:156-6277-7102
contacts:Manager Zhang

HeadPowder, a leading manufacturer in the field, specializes in advanced powder conveying systems tailored for the efficient handling of expanded perlite powders. This article delves into the operational process and underlying principles of such systems, providing a comprehensive understanding for industry professionals and potential clients. Based in Shandong, China, HeadPowder Engineering Co., Ltd. has established itself as a trusted provider of high-quality conveying solutions for various industrial sectors.
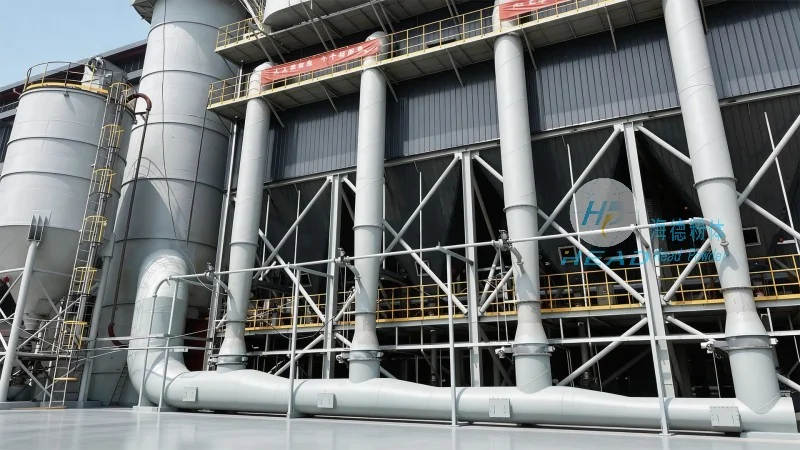
Operation Process and Working Principle of Expanded Perlite Powder Conveying System

Overview of Expanded Perlite Powder Conveying Systems

Expanded perlite powder, a lightweight, inorganic insulating material, is widely used in construction, industrial applications, and other sectors requiring thermal insulation or lightweight fillers. The efficient transportation of this fine powder from storage to processing or packaging units is critical for maintaining product quality and operational efficiency. HeadPowder’s conveying systems are engineered to address these challenges, ensuring reliable, low-dust, and energy-efficient powder handling.

Key Components and Their Functions

The expanded perlite powder conveying system typically comprises several core components, each playing a vital role in the overall operation. These include:
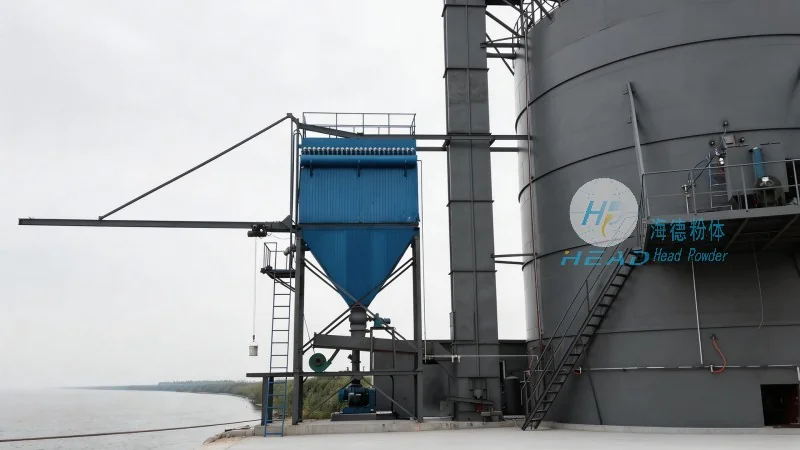
Operation Process and Working Principle of Expanded Perlite Powder Conveying System

  • Storage Hopper: A large, airtight container designed to store bulk expanded perlite powder. The hopper is equipped with a discharge valve to control the flow of material into the conveying system.
  • Pneumatic Conveying Unit: This is the heart of the system, utilizing air pressure to transport the fine powder through a network of pipes. The unit includes a blower or compressor that generates the necessary airflow to move the powder particles.
  • Conveying Pipelines: Flexible or rigid pipes that connect the storage hopper to the discharge point. The design of these pipelines is crucial to minimize pressure drop and prevent powder accumulation or blockages.
  • Control System: An automated control panel that monitors and regulates the operation of the blower, valve positions, and overall system pressure. This ensures precise control over the conveying process.
  • Dust Collection and Filtration: To maintain a clean and safe working environment, the system incorporates dust collection equipment that captures any airborne particles during the conveying process.

Operation Process: Step-by-Step

The operation of the expanded perlite powder conveying system follows a systematic sequence to ensure smooth and efficient material transfer. Here is a detailed breakdown of the process:

  1. Material Preparation: The expanded perlite powder is loaded into the storage hopper from a bulk delivery truck or other storage container. The hopper is then sealed to prevent moisture or contamination.
  2. System Initialization: The control system is activated, and the blower is started to generate the required airflow. The pressure in the system is monitored to ensure it is within the optimal range for conveying the powder.
  3. Material Discharge: The discharge valve in the storage hopper is opened, allowing the expanded perlite powder to enter the pneumatic conveying unit. The air flow pulls the powder particles into the pipelines.
  4. Pipeline Transport: The powder travels through the conveying pipelines under the force of the air current. The system’s design ensures that the powder moves at a consistent velocity, preventing clogging or uneven distribution.
  5. Discharge and Processing: At the end of the pipeline, the expanded perlite powder is discharged into a processing unit, such as a mixer, packaging machine, or storage silo. The control system adjusts the discharge rate to match the downstream processing requirements.
  6. Dust Management: Throughout the process, the dust collection system captures any fine particles that may escape, ensuring compliance with environmental regulations and maintaining a clean workspace.

Working Principle: The Physics Behind the System

The working principle of the expanded perlite powder conveying system is based on the principles of fluid dynamics and particle transport. The key mechanism involves the use of air as a carrier medium to move the fine powder particles. Here’s how it works:

When the blower generates airflow, it creates a pressure difference between the inlet and outlet of the conveying system. The expanded perlite powder particles are entrained by the air stream and carried through the pipelines. The velocity of the air must be sufficient to overcome the gravitational force acting on the powder particles and any frictional resistance within the pipelines.
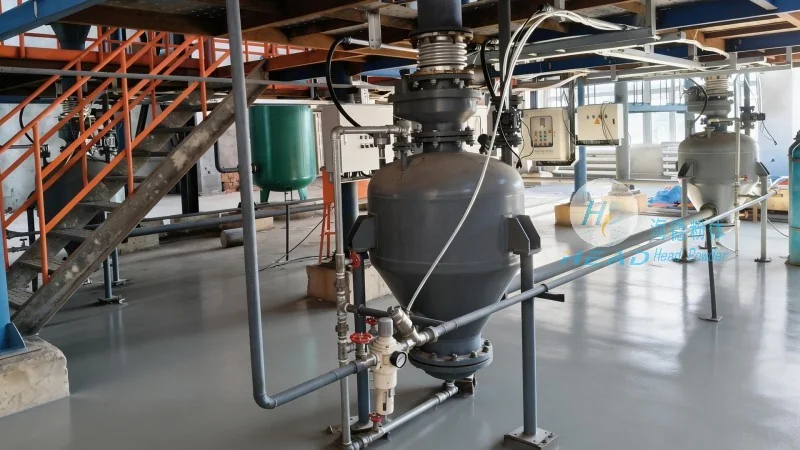
Operation Process and Working Principle of Expanded Perlite Powder Conveying System

The system’s efficiency depends on several factors, including the particle size and density of the expanded perlite, the air velocity, and the length and diameter of the conveying pipelines. Proper design and maintenance of the system are essential to ensure optimal performance and minimize energy consumption.

Benefits and Advantages of HeadPowder’s Conveying Systems

HeadPowder’s expanded perlite powder conveying systems offer several advantages that make them ideal for industrial applications:

recommend

Copyright © Shandong Headpowder Engineering Co., Ltd. All Rights Reserved.    营业执照公示 网站地图

top
