At Shandong HeadPowder Engineering Co., Ltd., we specialize in advanced solutions for handling dust ash and other fine powders through pneumatic conveying technology. Our systems are designed to efficiently transport these materials from one location to another, ensuring optimal performance and reliability in industrial applications. The dust ash powder pneumatic conveying line is a critical component in many manufacturing and processing facilities, enabling seamless material transfer while maintaining environmental standards.
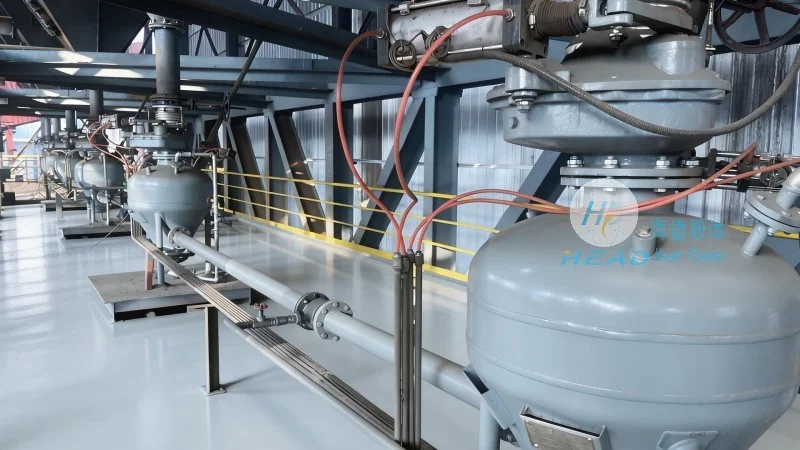
The core mechanism of a dust ash powder pneumatic conveying line involves the use of air pressure to move particulate materials through a network of pipes. There are primarily two types of systems: positive pressure and negative pressure. In positive pressure systems, compressed air is introduced into the material hopper, creating an upward flow that lifts and transports the dust ash particles through the pipeline. This method is often preferred for long-distance or high-volume applications due to its ability to handle abrasive materials and maintain consistent flow rates. Negative pressure systems, on the other hand, operate by creating a vacuum in the receiving hopper, drawing the dust ash particles into the pipeline as air is drawn out. This approach is typically used for shorter distances or when the material is sensitive to pressure changes. The system includes key components such as a hopper for material storage, a blower or compressor to generate the air flow, a pipeline network for material transport, and a receiver or discharge hopper to collect the material at the destination. The entire process is controlled by a system of valves, sensors, and control panels that ensure smooth operation and prevent blockages or over-pressurization.
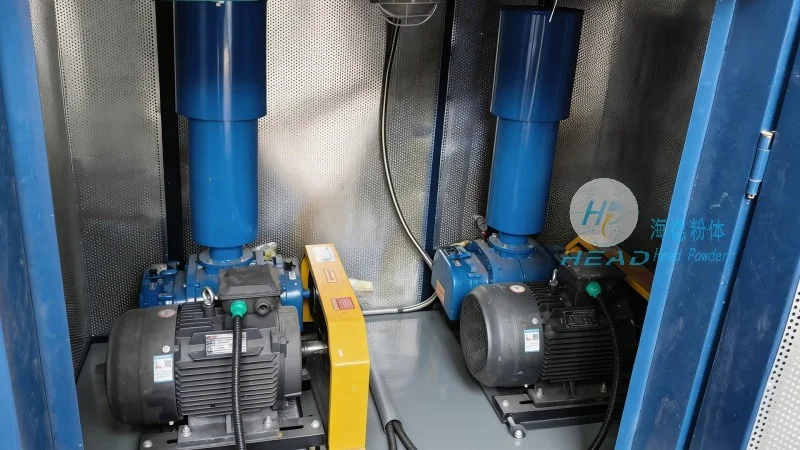
One of the most significant advantages of dust ash powder pneumatic conveying lines is their high efficiency in material handling. Unlike traditional methods like bucket elevators or belt conveyors, pneumatic systems can transport materials over longer distances with minimal energy consumption and reduced maintenance. The technology also offers excellent flexibility, allowing for changes in the layout or direction of material flow without major modifications to the system. Environmental benefits are another critical characteristic, as these systems are designed to minimize dust emissions and comply with air quality regulations. By containing the material within a sealed pipeline, the risk of dust contamination and air pollution is significantly reduced. Additionally, the systems are highly scalable, making them suitable for both small-scale operations and large industrial facilities. The use of advanced materials and engineering in the construction of the pipelines and components ensures durability and resistance to corrosion, even when handling abrasive dust ash particles. Automation features, such as real-time monitoring and control, further enhance operational efficiency and safety, reducing the need for manual intervention and minimizing the risk of accidents.
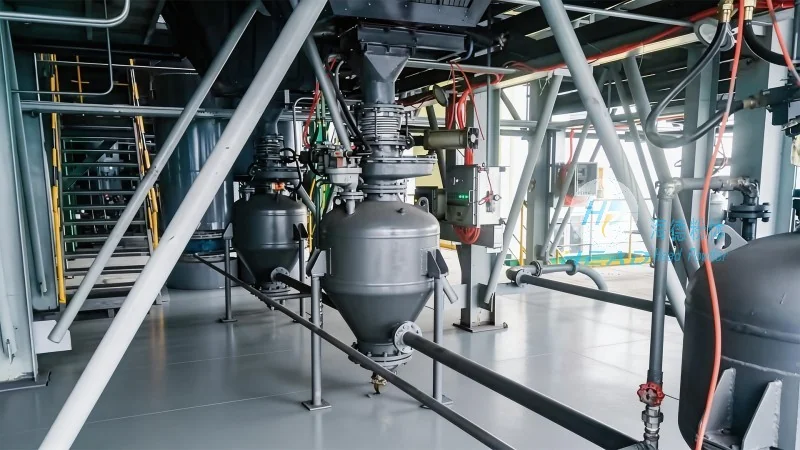
Dust ash powder pneumatic conveying lines are widely used across various industries, including power generation, cement production, and waste management. In power plants, these systems are essential for transporting fly ash from boilers to storage silos or for reusing it in cement production. The high efficiency and reliability of the systems ensure that the ash is handled safely and efficiently, reducing the risk of environmental contamination. In the cement industry, the technology is used to transport raw materials like limestone and clinker, as well as to handle waste materials such as slag. The ability to handle abrasive and fine particles makes the system ideal for these applications, where traditional methods may struggle with material buildup or blockages. Waste management facilities also benefit from these systems, as they can efficiently transport ash and other solid waste materials from incinerators to disposal sites or for recycling purposes. The systems are also used in chemical and pharmaceutical industries, where the handling of fine powders requires strict control over dust and contamination. Overall, the versatility and adaptability of dust ash powder pneumatic conveying lines make them a preferred choice for industries that require reliable, efficient, and environmentally friendly material handling solutions.
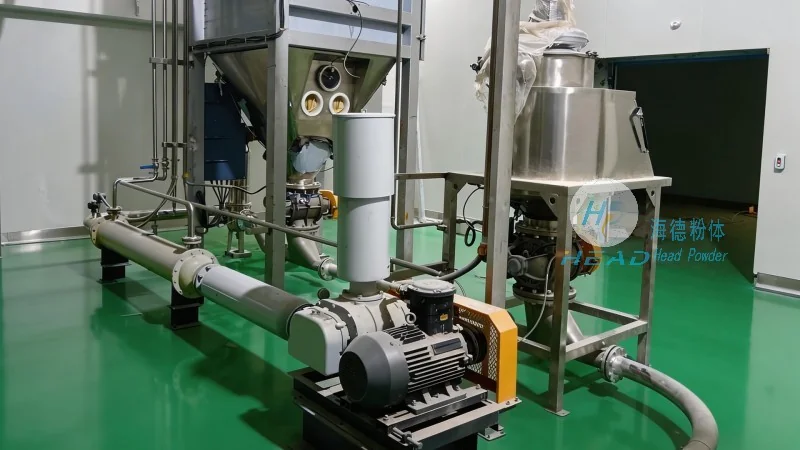
Shandong HeadPowder Engineering Co., Ltd. stands as a leading provider of dust ash powder pneumatic conveying systems, leveraging decades of expertise in material handling technology. Our commitment to innovation and quality ensures that our systems meet the highest standards of performance, reliability, and environmental compliance. By understanding the unique challenges of dust ash and other fine powders, we design and manufacture solutions that address the specific needs of each industrial application. Whether for long-distance transport, high-volume handling, or environmental compliance, our pneumatic conveying lines offer a cost-effective and efficient solution. With our headquarters in Shandong, China, we serve clients globally, providing tailored solutions that enhance operational efficiency and reduce costs. The working principle and characteristics of our dust ash powder pneumatic conveying lines are designed to deliver optimal results, making them an essential component in modern industrial operations.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top