Shandong HeadPowder Engineering Co., Ltd. specializes in providing advanced solutions for the handling and transportation of powdered desulfurization and denitrification agents through pneumatic conveying systems. With a focus on efficiency and reliability, our company has developed innovative technologies to address the unique challenges associated with transporting these critical industrial chemicals. Based in Shandong, China, HeadPowder Engineering is committed to delivering high-quality equipment and services tailored to meet the demands of modern industrial applications.
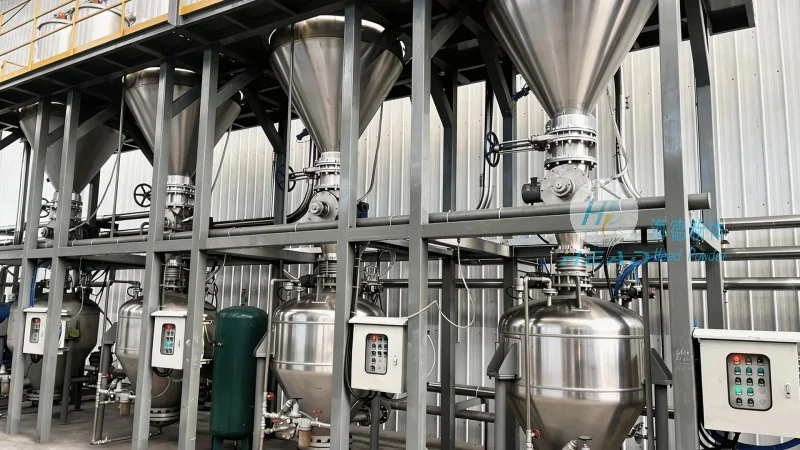
Our primary product is a specialized system designed to handle powdered desulfurization and denitrification agents using pneumatic conveying. This technology involves the use of compressed air to transport dry powders over long distances, eliminating the need for traditional bulk handling methods such as trucks or conveyor belts. The system is engineered to maintain the integrity of the powder, ensuring that the chemical properties of the desulfurization and denitrification agents remain stable during transportation. This is crucial for maintaining the effectiveness of these agents in industrial processes, particularly in power generation and chemical manufacturing.
The core mechanism of our pneumatic conveying system for desulfurization and denitrification agents operates on the principle of air flow and pressure differentials. The system typically consists of a hopper, a rotary valve, a pipeline, and a receiver. The powdered agents are fed into the hopper, where a rotary valve controls the flow rate into the pipeline. Compressed air is then introduced into the pipeline, creating a low-pressure environment that draws the powder particles into the air stream. The mixture of air and powder travels through the pipeline to the receiver, where the powder is separated from the air using a cyclone or other separation equipment. The separated powder is then collected for further use, while the air is either filtered or recycled back into the system. This process ensures a continuous and efficient flow of the desulfurization and denitrification agents, minimizing downtime and maximizing operational efficiency.
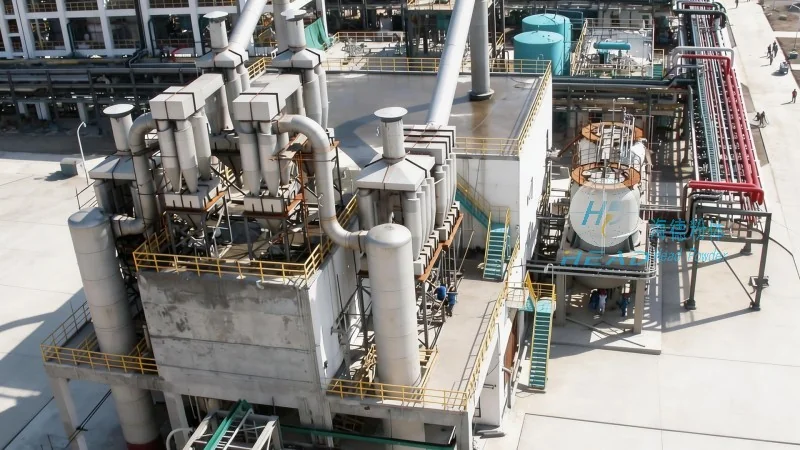
Several distinct characteristics make our pneumatic conveying system for desulfurization and denitrification agents highly effective and suitable for industrial applications. First, the system offers a high degree of flexibility in terms of transportation distances and layout. It can be configured to handle materials over short or long distances, adapting to the specific needs of different industrial sites. Second, the system provides excellent control over the flow rate and pressure, allowing for precise regulation of the powder transport. This is essential for maintaining the quality of the desulfurization and denitrification agents, as fluctuations in flow or pressure can affect their performance. Third, the system is designed for low maintenance and durability, with components that are resistant to corrosion and wear from the abrasive nature of the powdered agents. This reduces operational costs and ensures long-term reliability. Fourth, the system is equipped with safety features to prevent dust explosions and other hazards, ensuring compliance with industrial safety standards. Finally, the system is scalable, allowing for expansion as the industrial needs grow, making it a cost-effective solution for both new and existing facilities.
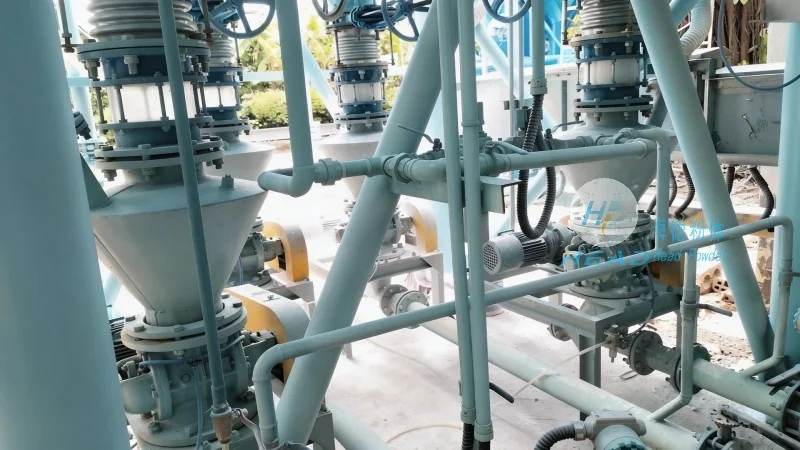
Implementing a pneumatic conveying system for desulfurization and denitrification agents offers numerous advantages over traditional handling methods. One of the most significant benefits is the reduction in material handling costs. By eliminating the need for trucks or conveyor belts, the system reduces labor and equipment expenses associated with bulk transport. Additionally, the system minimizes the risk of material contamination, as the powder is contained within the pipeline and does not come into contact with external elements. This is particularly important for desulfurization and denitrification agents, which are sensitive to moisture and other environmental factors. The system also improves safety by reducing the exposure of workers to dust and other hazardous materials. Furthermore, the continuous operation of the system ensures a steady supply of the agents, which is critical for maintaining the efficiency of industrial processes. Finally, the system is environmentally friendly, as it reduces the carbon footprint associated with traditional transportation methods by minimizing the use of vehicles and other equipment.
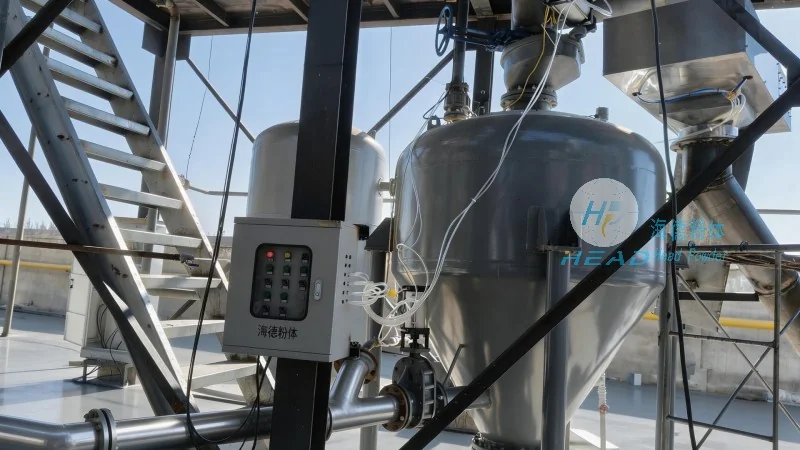
Our pneumatic conveying system for desulfurization and denitrification agents is widely used in various industrial applications, particularly in power generation and chemical manufacturing. In power plants, the system is used to transport limestone or other alkaline materials to the desulfurization units, where they react with sulfur dioxide to form calcium sulfite or calcium sulfate. The denitrification agents, such as ammonia or urea, are then transported to the denitrification units, where they react with nitrogen oxides to form harmless nitrogen gas. The system ensures that these agents are delivered to the reaction points in a controlled and efficient manner, maximizing the effectiveness of the pollution control processes. In chemical manufacturing, the system is used to transport various powdered chemicals used in the production of fertilizers, pharmaceuticals, and other industrial products. The system's ability to handle abrasive and sensitive materials makes it ideal for these applications, where maintaining the quality and purity of the chemicals is essential.
Shandong HeadPowder Engineering Co., Ltd. provides a reliable and efficient pneumatic conveying system for powdered desulfurization and denitrification agents. The system operates on a well-defined working principle, utilizing compressed air to transport the agents over long distances while maintaining their integrity. The key characteristics of the system, including flexibility, control, durability, and safety, make it an ideal solution for industrial applications. The advantages of using this system include reduced material handling costs, minimized contamination risk, improved safety, and environmental benefits. With its application in power generation and chemical manufacturing, the system plays a crucial role in modern industrial processes, contributing to the reduction of air pollution and the enhancement of operational efficiency. HeadPowder Engineering is committed to continuing to innovate and improve its pneumatic conveying systems to meet the evolving needs of the industrial sector.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top