Mineral particle material conveying systems are essential in various industrial applications, designed to efficiently transport bulk materials such as ores, powders, and granules from one location to another. These systems play a crucial role in optimizing production processes, enhancing operational efficiency, and ensuring safe material handling. The following sections will explore the working principle and key features of such systems, providing a comprehensive understanding of their functionality and benefits. Shandong HeadPowder Engineering Co., Ltd., a leading manufacturer based in Shandong, China, specializes in the design and production of high-quality mineral particle material conveying systems.
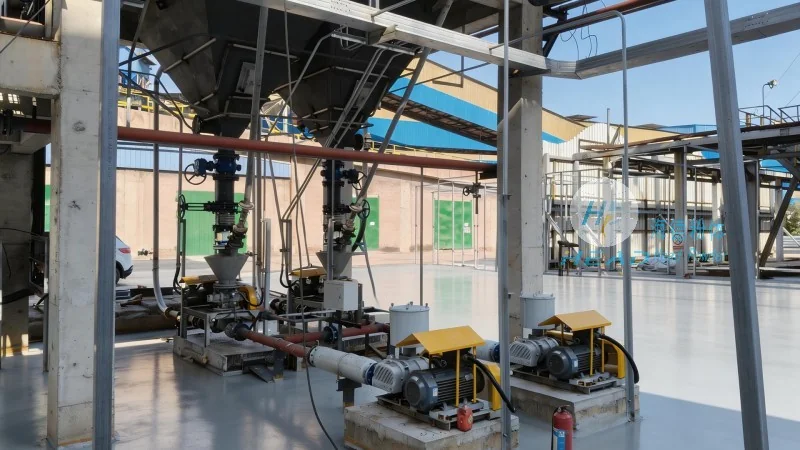
Mineral particle material conveying systems are engineered to handle a wide range of bulk materials, including minerals, ores, and processed powders. These systems are typically used in mining, construction, and manufacturing industries where large volumes of materials need to be transported over short or long distances. The primary goal is to achieve reliable, continuous, and efficient material movement while minimizing downtime and operational costs.
The core working principle of mineral particle material conveying systems revolves around the use of mechanical components to move materials through a defined path. Common mechanisms include screw conveyors, belt conveyors, and pneumatic conveyors, each tailored to specific material characteristics and operational requirements. For instance, screw conveyors utilize a rotating helical screw to push materials forward, while belt conveyors rely on a continuous belt that transports materials via friction. Pneumatic conveyors, on the other hand, use air pressure to transport materials through a pipeline, making them suitable for fine powders and granules.
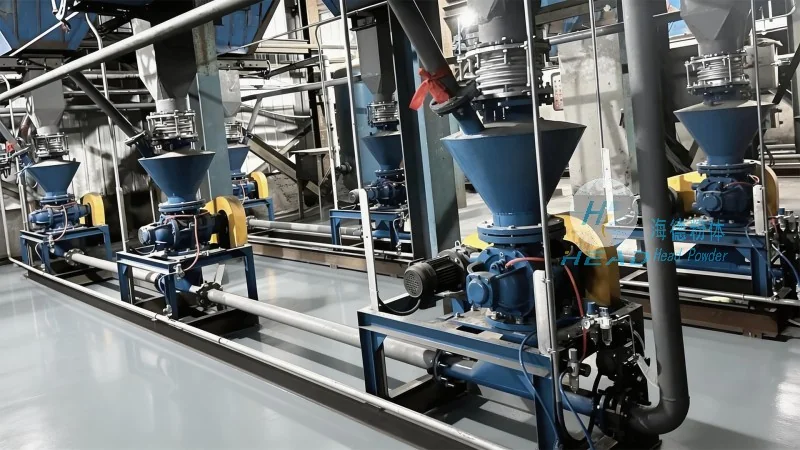
Several key features distinguish effective mineral particle material conveying systems, contributing to their reliability and performance. First, durability and robust construction are critical, as these systems often operate in harsh environments with abrasive materials. Materials such as stainless steel or high-strength alloys are commonly used to ensure longevity and resistance to wear. Second, efficiency and energy savings are paramount. Modern systems incorporate advanced drive technologies and variable speed controls to optimize power consumption while maintaining consistent material flow rates. Third, safety features are integrated to prevent accidents and ensure compliance with industrial standards. This includes emergency stop mechanisms, overload protection, and proper sealing to prevent dust emissions and material spillage.
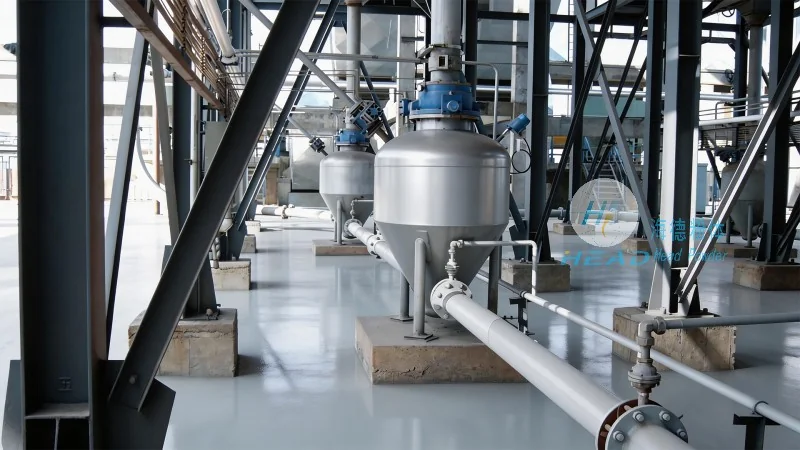
The design of mineral particle material conveying systems is tailored to meet the specific needs of different applications. For example, in mining operations, systems may need to handle large, heavy particles and operate in high-temperature environments. In contrast, systems used in food processing or pharmaceutical industries require strict hygiene standards and non-contaminating materials. The choice of conveyor type, material of construction, and control systems is carefully evaluated to ensure optimal performance and compliance with industry regulations.
Implementing mineral particle material conveying systems offers numerous benefits for industrial operations. These systems enhance productivity by enabling continuous material flow, reducing manual handling and labor costs. They also improve safety by minimizing human exposure to hazardous materials and reducing the risk of accidents. Additionally, efficient conveying systems contribute to cost savings through reduced energy consumption and lower maintenance requirements. The ability to customize systems to specific material and operational needs further enhances their value, making them a versatile solution for diverse industrial applications.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top