Gray silo powder conveying systems are essential equipment in industrial processes, particularly for handling bulk materials like powders and granules. These systems are designed to efficiently transport materials from storage silos to processing units, ensuring smooth and reliable operation. The following article explores the working principle and key features of such systems, highlighting their importance in modern industrial applications.
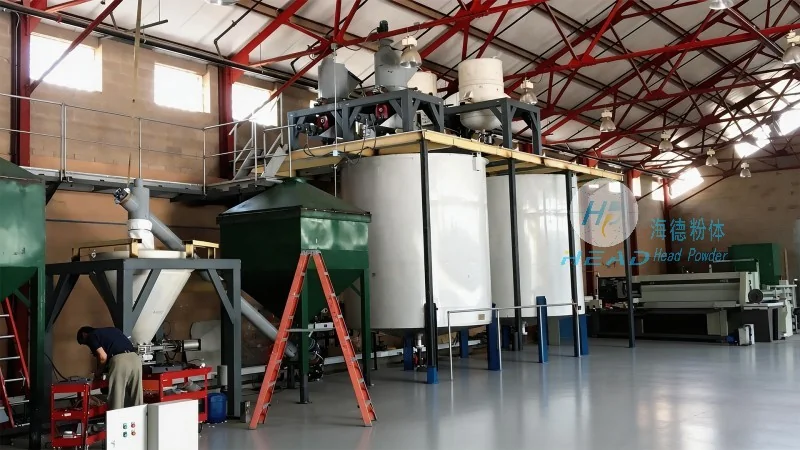
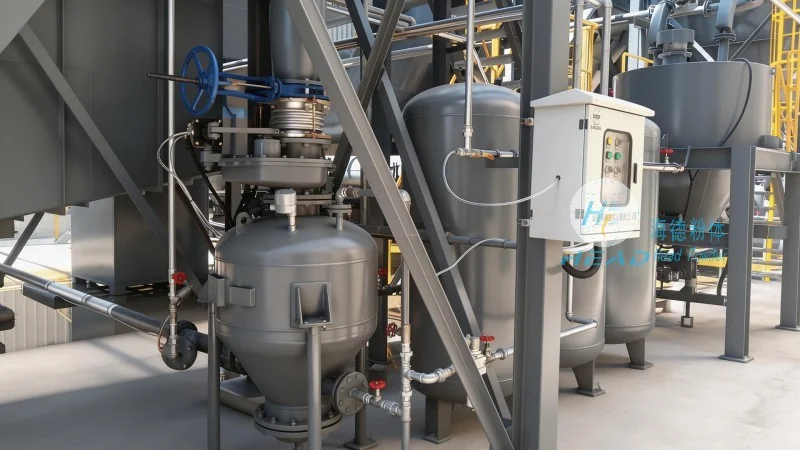
The core working principle of gray silo powder conveying systems revolves around the use of air pressure or vacuum to move powder materials through a network of pipes. Typically, these systems employ a combination of positive pressure and negative pressure techniques to achieve material transport. The process begins with the material being drawn from the silo through a hopper or feeder, where it is then introduced into a conveying line. Air is then introduced into the system, either by a blower or a vacuum pump, creating a flow that carries the powder particles along the pipeline. The design of the silo and the conveying line is critical, as it must prevent material buildup and ensure consistent flow rates. The system often includes components such as rotary valves, airlocks, and filters to maintain material integrity and prevent contamination. By controlling the air pressure and flow rate, operators can adjust the conveying speed and capacity to meet specific production requirements.
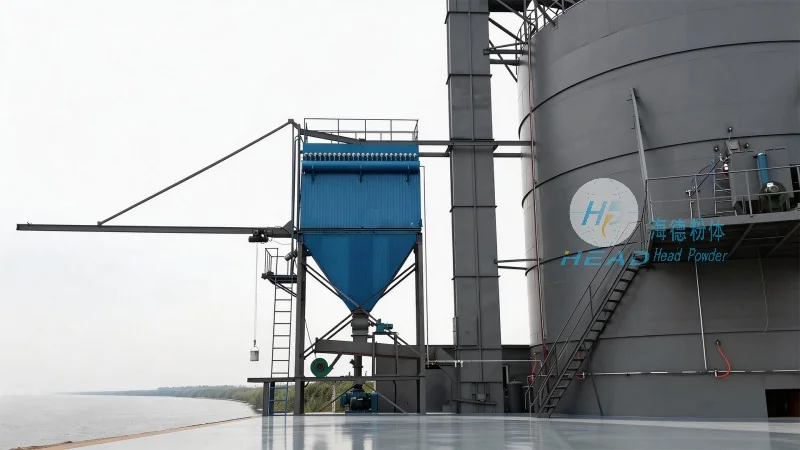
Gray silo powder conveying systems offer several distinct features that make them suitable for a wide range of industrial applications. One of the primary features is their ability to handle a variety of powder types, including fine powders, granules, and even abrasive materials. The systems are designed to minimize material degradation and maintain product quality throughout the conveying process. Another important feature is their energy efficiency, as they typically consume less power compared to traditional mechanical conveying methods. The modular design of these systems allows for easy installation and integration into existing production lines, reducing downtime and installation costs. Additionally, gray silo powder conveying systems are equipped with safety features such as pressure relief valves and overfill protection to ensure safe operation. The systems also provide flexibility in terms of conveying distance and height, making them suitable for both short and long-distance material transport. Furthermore, the use of advanced materials in the construction of the silo and conveying line ensures durability and resistance to corrosion, extending the lifespan of the equipment.
Shandong HeadPowder Engineering Co., Ltd., commonly known as HeadPowder, is a leading manufacturer and supplier of industrial powder handling equipment. With a strong focus on innovation and quality, the company has established itself as a trusted partner in the industry. HeadPowder specializes in the design, manufacturing, and installation of gray silo powder conveying systems, as well as other related equipment such as silos, feeders, and storage solutions. The company's products are widely used in sectors like food processing, pharmaceuticals, chemicals, and mining. HeadPowder's commitment to customer satisfaction is reflected in its comprehensive after-sales service and technical support. The company's facilities are located in Shandong, China, where it leverages advanced manufacturing technologies and skilled workforce to produce high-quality equipment. HeadPowder's team of engineers and technicians continuously research and develop new solutions to meet the evolving needs of the industry, ensuring that its products remain at the forefront of technology.
Gray silo powder conveying systems find extensive applications in various industries due to their versatility and efficiency. In the food industry, these systems are used to transport ingredients such as flour, sugar, and spices from storage silos to processing lines, ensuring consistent quality and hygiene. In the pharmaceutical sector, the systems are employed to handle active pharmaceutical ingredients (APIs) and other sensitive materials, maintaining strict contamination control. The chemical industry utilizes gray silo powder conveying systems for the transport of raw materials and intermediates, improving production efficiency and safety. Additionally, in the mining and mineral processing industries, these systems are used to convey bulk materials like ores and powders from storage to processing facilities. The benefits of using gray silo powder conveying systems include improved operational efficiency, reduced labor costs, and enhanced safety. By automating the material handling process, these systems minimize the risk of human error and accidents, while also increasing the overall productivity of the production line. Furthermore, the systems contribute to better material management by ensuring accurate inventory control and reducing material waste.
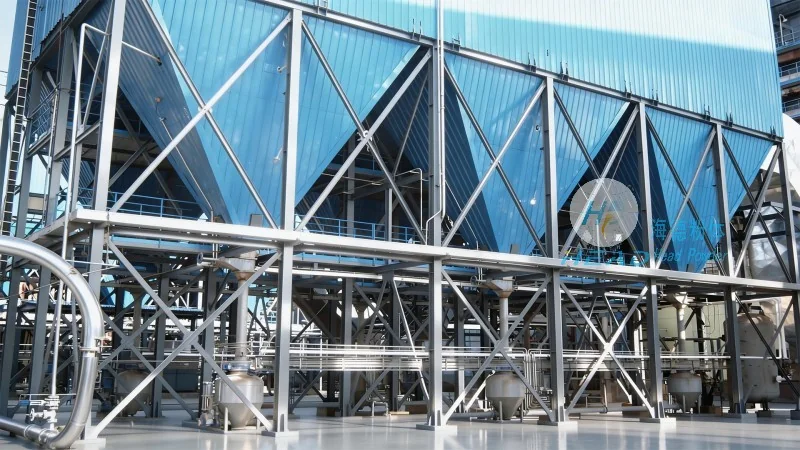
In conclusion, gray silo powder conveying systems are crucial components in modern industrial operations, offering efficient and reliable material transport solutions. The working principle, which relies on air pressure and vacuum, enables these systems to handle a wide range of powder materials with minimal degradation. The key features, including energy efficiency, modular design, and safety measures, make them ideal for various applications. Shandong HeadPowder Engineering Co., Ltd. plays a significant role in providing high-quality equipment and services to meet the industry's demands. As technology advances, the future of gray silo powder conveying systems looks promising, with ongoing innovations aimed at improving performance, reducing costs, and enhancing sustainability. The continued development of these systems will undoubtedly contribute to the growth and efficiency of industrial processes worldwide.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top