Soil material conveying is a critical process in various industries, including construction, mining, and environmental management. It involves the efficient transport of soil, sand, and other granular materials from one location to another. Understanding the working principles and key characteristics of soil material conveyors is essential for optimizing operational efficiency and ensuring safety in material handling applications.
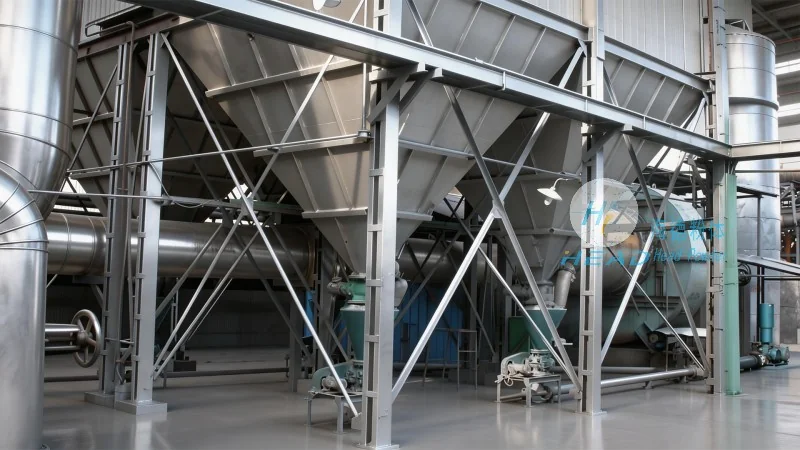
At the core of soil material conveying systems are mechanisms designed to move bulk materials through a pipeline or conveyor structure. These systems typically operate on principles of gravity, mechanical force, or a combination of both. The most common types of soil material conveyors include screw conveyors, belt conveyors, and pneumatic conveyors, each utilizing distinct operational methods to achieve material transport.
Screw conveyors, for instance, employ a rotating helical screw within a tube to push material forward. This mechanism is particularly effective for handling cohesive materials like soil and clay, as the screw's rotation creates a continuous flow without the need for additional external forces. The design of the screw, including its pitch and diameter, is tailored to the specific characteristics of the soil being conveyed, ensuring optimal performance and minimal wear.
Belt conveyors, on the other hand, use a continuous belt that moves over rollers or pulleys to transport materials. This method is widely used in open-pit mining and construction sites due to its ability to handle large volumes of material over long distances. The belt's speed and tension are carefully controlled to prevent slippage and ensure consistent material movement. For soil material conveying, the belt is often reinforced with materials like rubber or polyurethane to withstand the abrasive nature of soil and prevent tearing.
Pneumatic conveyors utilize air pressure to move materials through a pipeline. This system is particularly advantageous for handling fine powders and granular soils, as it can transport materials vertically and horizontally with minimal disruption. The air pressure is generated by a blower or compressor, creating a flow that propels the material through the system. Pneumatic conveyors are often used in applications where dust control is a priority, as the enclosed pipeline prevents airborne particles from spreading.
When evaluating soil material conveying equipment, several key characteristics must be considered to ensure suitability for specific applications. These characteristics include material handling capacity, system efficiency, durability, and operational flexibility.
Material handling capacity refers to the volume of soil that a conveyor can transport per unit of time. This is typically measured in cubic meters per hour (m³/h) or tons per hour (t/h). The capacity of a conveyor system is determined by factors such as the screw diameter, belt width, or pipeline diameter, and is critical for meeting production demands in construction and mining projects. For example, a large-scale mining operation may require a conveyor with a capacity of several hundred tons per hour to transport earth materials efficiently.
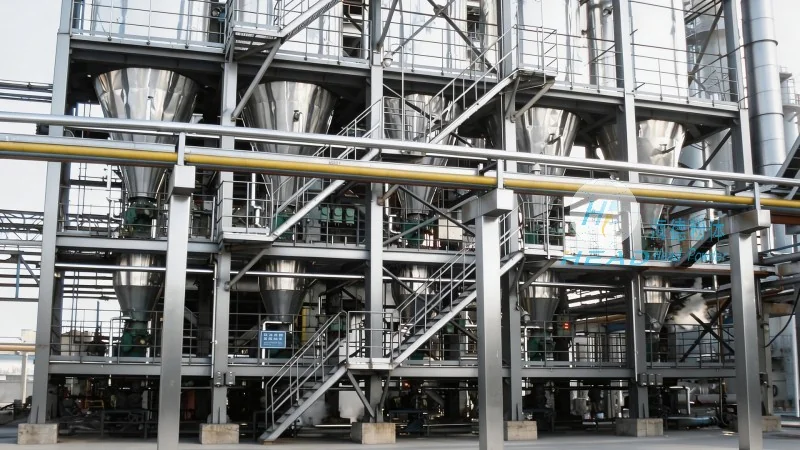
System efficiency is another crucial characteristic, as it relates to the energy consumption and operational costs of the conveying system. Efficient soil material conveyors minimize energy usage while maximizing material throughput. This is achieved through optimized design, such as using variable speed drives for screw conveyors or adjustable air pressure for pneumatic systems. Energy efficiency not only reduces operational costs but also contributes to environmental sustainability by lowering carbon emissions.
Durability is a vital characteristic, especially when dealing with abrasive soil materials that can cause wear and tear on conveyor components. High-quality materials like stainless steel, hardened steel, or specialized polymers are used to construct conveyor parts, ensuring long service life and minimal maintenance. For instance, the screw flights in a soil conveyor are often made of hardened steel to resist the abrasive action of soil particles, while the belt is reinforced with a steel cord to prevent tearing under heavy loads.
Operational flexibility is also an important consideration, as soil material conveying systems often need to adapt to changing conditions or project requirements. Flexible conveyors, such as those with adjustable lengths or modular components, can be easily reconfigured to accommodate different material types or transport routes. This adaptability is particularly valuable in construction projects where the layout of the site may change during the course of work.
Soil material conveying systems are widely used in various industries, offering numerous benefits that enhance operational performance and safety. In the construction industry, these systems are essential for transporting earth materials during site preparation, foundation work, and backfilling. By using conveyors, construction companies can reduce the need for manual labor and heavy machinery, improving efficiency and minimizing the risk of accidents.
In the mining sector, soil material conveyors play a critical role in transporting ore and overburden from mining sites to processing facilities. The ability to handle large volumes of material over long distances makes these systems indispensable for large-scale mining operations. Additionally, the use of enclosed pneumatic conveyors helps control dust and prevent environmental contamination, which is increasingly important in modern mining practices.
Environmental management applications also benefit from soil material conveying systems. For example, in land reclamation projects, conveyors are used to transport soil and other materials for site restoration. This process helps restore ecosystems and prevent soil erosion, contributing to environmental sustainability. The efficient transport of materials in these projects reduces the need for multiple trips by trucks, lowering fuel consumption and emissions.
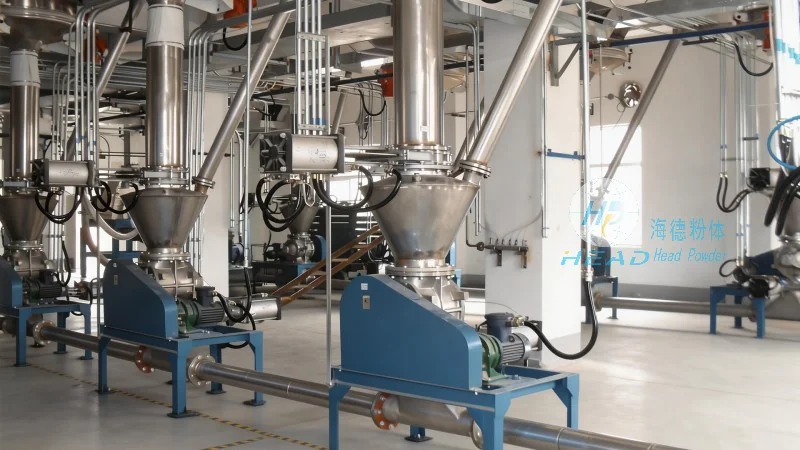
Another key benefit of soil material conveying is the improvement in workplace safety. By eliminating the need for manual handling of heavy loads, conveyors reduce the risk of injuries and accidents. This is particularly important in industries where workers are exposed to hazardous materials or difficult working conditions. The automation of material transport also allows for better monitoring and control of the process, ensuring that safety protocols are consistently followed.
Selecting the appropriate soil material conveying system requires careful consideration of several factors, including the type of soil being handled, the distance to be covered, and the desired throughput. Each type of conveyor—screw, belt, or pneumatic—has its own advantages and limitations, making it essential to match the system to the specific requirements of the application.
For cohesive soils like clay, screw conveyors are often the preferred choice due to their ability to handle materials that might stick to traditional belts. The rotating screw provides consistent movement, preventing material buildup and ensuring smooth transport. However, for dry, loose soils, belt conveyors may be more suitable, as they can handle larger volumes and longer distances with less maintenance.
Pneumatic conveyors are ideal for fine powders and granular soils that are prone to dust generation. The enclosed pipeline prevents dust from spreading, making these systems suitable for applications where air quality is a concern. Additionally, pneumatic conveyors can transport materials vertically, which is often necessary in construction and mining sites where space is limited.
When evaluating conveyor systems, it is also important to consider the overall cost of ownership, including initial investment, maintenance, and energy consumption. A well-designed system from a reputable manufacturer like Shandong HeadPowder Engineering Co., Ltd. can provide long-term benefits by reducing operational costs and minimizing downtime. The company, with its headquarters in Shandong, China, specializes in providing high-quality soil material conveying solutions tailored to the needs of various industries.
Shandong HeadPowder Engineering Co., Ltd. offers a range of soil material conveying equipment, including screw conveyors, belt conveyors, and pneumatic systems, each designed to meet the specific requirements of different applications. The company's products are known for their durability, efficiency, and reliability, making them a trusted choice for businesses in construction, mining, and environmental management. By choosing a system from HeadPowder, companies can enhance their operational performance, reduce costs, and ensure safe and effective material handling.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top