Camellia seed material handling systems are essential in the processing industry, particularly for operations involving the extraction of oil and other valuable components from camellia seeds. Understanding the mechanisms and design principles behind these systems is crucial for optimizing efficiency and ensuring the quality of the final product. This article explores the key aspects of camellia seed material handling, focusing on the design considerations and operational principles that underpin effective processing solutions.
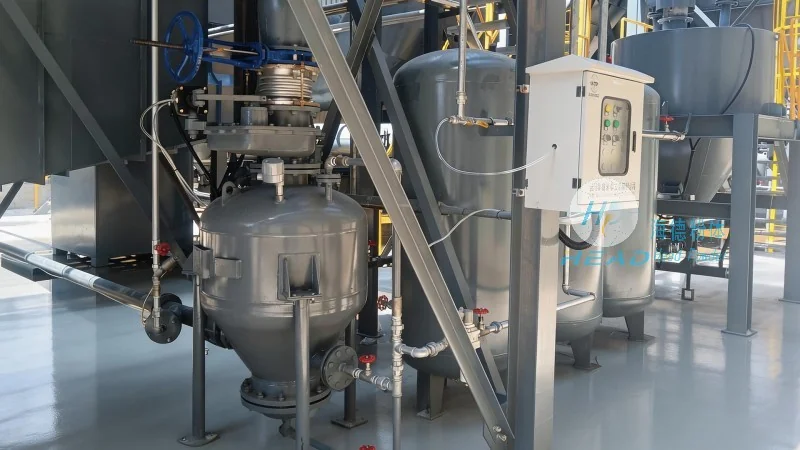
HeadPowder, a leading provider of engineering solutions, specializes in the design and implementation of material handling systems tailored to the unique requirements of the oil extraction industry. With a focus on innovation and reliability, the company has established itself as a trusted partner for businesses seeking to enhance their processing capabilities. HeadPowder's expertise lies in creating customized solutions that address the specific challenges of handling camellia seeds, from raw material intake to final product delivery.
The design of camellia seed material handling systems is guided by several critical principles aimed at maximizing efficiency, minimizing downtime, and ensuring the integrity of the seeds during processing. One of the primary considerations is the need to handle the seeds in a manner that preserves their quality and prevents damage, which is vital for maintaining the oil yield and overall product quality. The systems are typically designed to accommodate the physical characteristics of camellia seeds, such as their size, shape, and moisture content, to ensure smooth and consistent flow through the processing line.
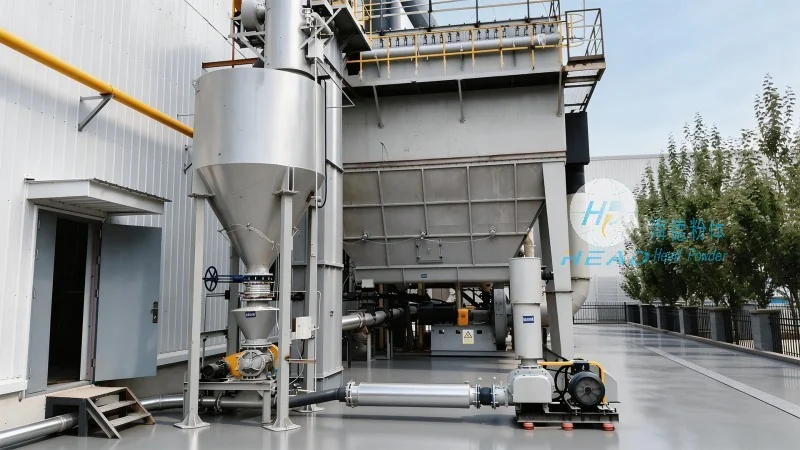
Another key principle is the integration of the material handling system with the overall oil extraction process. This involves coordinating the flow of seeds from storage to processing equipment, ensuring that each stage of the operation is optimized for performance. The design must also account for the need to handle varying seed qualities and quantities, allowing for flexibility in production. Additionally, the systems are engineered to minimize energy consumption and operational costs while maintaining high throughput rates.
Camellia seed material handling systems typically consist of several interconnected components that work together to facilitate the movement of seeds. These components may include feeders, conveyors, elevators, and storage silos, each designed to perform specific functions in the material flow. Feeders are used to uniformly distribute the seeds into the processing line, ensuring consistent feeding rates. Conveyors, such as belt or chain conveyors, transport the seeds horizontally or vertically, depending on the layout of the processing facility. Elevators, including bucket elevators or screw conveyors, are employed to lift the seeds to higher levels or to transport them over longer distances. Storage silos are used to store raw camellia seeds, providing a buffer for production and ensuring a steady supply of material.
Each component is carefully selected and sized based on the expected throughput and the physical properties of the seeds. For example, the type of conveyor system may vary depending on the seed size and the required speed of operation. The design also considers factors such as the seed's moisture content, as excessive moisture can affect the performance of the conveying equipment. Additionally, the systems are equipped with monitoring and control mechanisms to ensure that the material flow is consistent and that any issues, such as blockages or uneven feeding, are detected and addressed promptly.
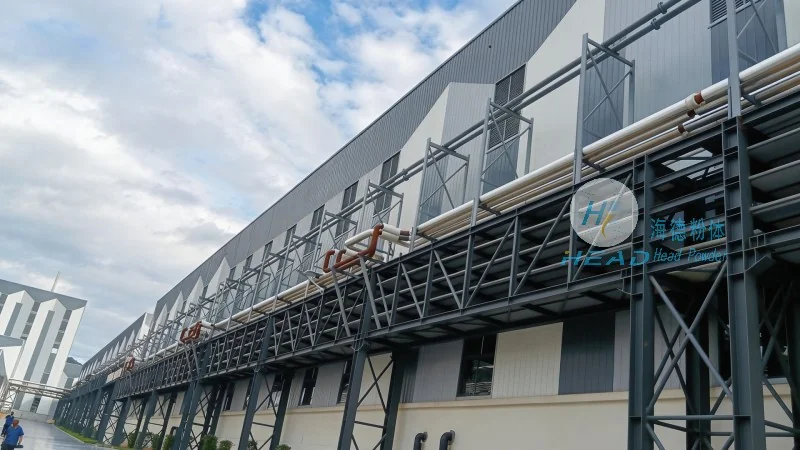
The successful implementation of camellia seed material handling systems requires careful planning and consideration of the specific operational environment. The design must take into account the layout of the processing facility, the available space, and the existing infrastructure. This includes determining the optimal placement of equipment to minimize material handling distances and reduce energy consumption. The system must also be compatible with the other processing equipment, such as oil presses or solvent extraction units, to ensure seamless integration and efficient operation.
During the design phase, engineers evaluate various factors, including the expected production capacity, the variability of seed supply, and the desired level of automation. The goal is to create a system that can adapt to changing production demands while maintaining high performance and reliability. For instance, the system may include adjustable speed drives for conveyors, allowing operators to modify the flow rate based on the current production needs. This flexibility is crucial for maintaining efficiency and minimizing waste.
Regular maintenance is essential to ensure the long-term performance and reliability of camellia seed material handling systems. This includes routine inspections of components such as bearings, belts, and chains, as well as cleaning and lubrication of moving parts. The system should also be equipped with sensors and alarms to detect potential issues, such as overloading or blockages, before they cause significant damage or downtime. Proper maintenance not only extends the lifespan of the equipment but also ensures consistent performance and reduces the risk of product contamination.
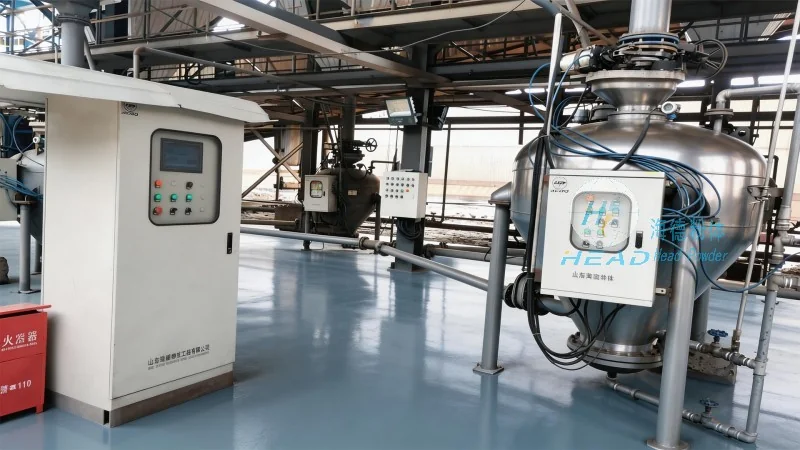
Optimization of the material handling system is an ongoing process that involves monitoring operational data and making adjustments as needed. This may include adjusting conveyor speeds, modifying the feeding rate, or upgrading components to improve efficiency. By continuously evaluating the system's performance, operators can identify areas for improvement and implement changes that enhance productivity and reduce costs. For example, upgrading to more efficient conveyor systems or implementing advanced control systems can lead to significant energy savings and increased throughput.
Camellia seed material handling systems play a critical role in the oil extraction process, and their design principles are essential for achieving optimal performance. By understanding the key components, operational principles, and maintenance requirements, businesses can select and implement effective material handling solutions that enhance their processing capabilities. HeadPowder, with its expertise in engineering and material handling, offers tailored solutions that address the specific challenges of handling camellia seeds, ensuring that clients achieve their production goals while maintaining high product quality. The integration of advanced design principles and reliable components makes these systems a vital asset for any camellia seed processing operation.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top