HeadPowder, a leading engineering firm based in Shandong, China, specializes in advanced material handling solutions, including pneumatic conveying systems tailored for water-in-powder applications. This article explores the different types of pneumatic conveying systems and their practical applications in industrial settings.
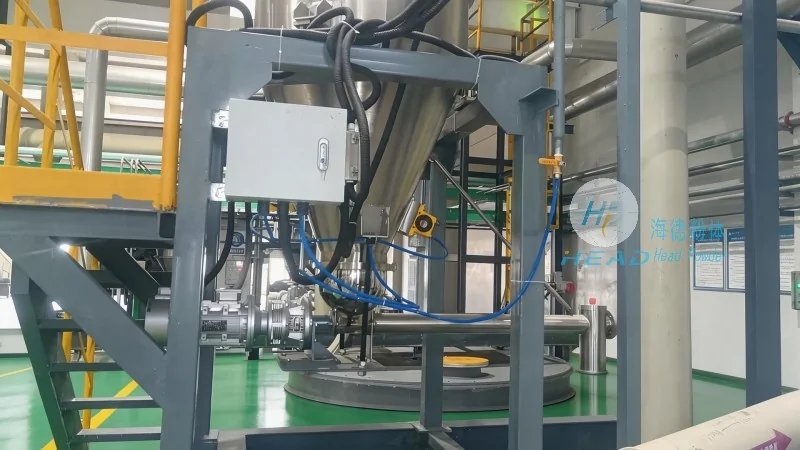
Pneumatic conveying systems are essential for transporting dry powders, granules, and other particulate materials in various industries. These systems utilize air or gas to move materials through a pipeline, offering a flexible and efficient method for material transfer. The choice of system type depends on factors such as material characteristics, distance, and required flow rates.
There are primarily two types of pneumatic conveying systems: positive pressure and negative pressure systems. Positive pressure systems, also known as pressure or blow-through systems, use compressed air to push material through the pipeline. These systems are suitable for short to medium distances and can handle abrasive or sticky materials. Negative pressure systems, or vacuum systems, use a vacuum to draw material into the pipeline. They are ideal for long-distance transport and can handle fine powders that are prone to dusting.
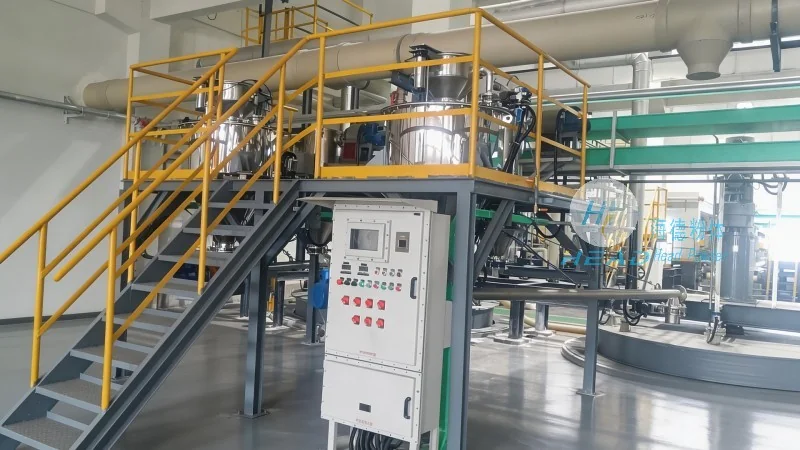
Positive pressure systems operate by injecting compressed air into the material stream, creating a pressure differential that propels the material forward. This type of system is commonly used in applications where the material needs to be transported over short to medium distances, typically up to several hundred meters. The system consists of a blower, a material feed hopper, and a pipeline network. The compressed air is introduced at the feed point, and the material is carried along with the air flow. Positive pressure systems are particularly effective for handling materials that are prone to caking or agglomeration, as the air flow helps to keep the material in suspension.
Negative pressure systems work by creating a vacuum at the discharge end of the pipeline, which draws material from the source. The system includes a vacuum pump, a material source, and a pipeline. The vacuum is maintained by the pump, and the material is pulled into the pipeline and transported to the discharge point. Negative pressure systems are advantageous for long-distance transport, as they can handle materials over distances of several kilometers. They are also suitable for applications where the material is sensitive to pressure or where the environment needs to be kept dust-free, as the system operates under a negative pressure, preventing dust from escaping.
In water-in-powder delivery applications, pneumatic conveying systems are used to transport powdered ingredients, such as cement, flour, or chemical powders, along with water to form a slurry or suspension. The system ensures that the powder and water are mixed uniformly and transported efficiently to the target location. This is particularly important in industries like construction, food processing, and chemical manufacturing, where precise control over the material mixture is critical.
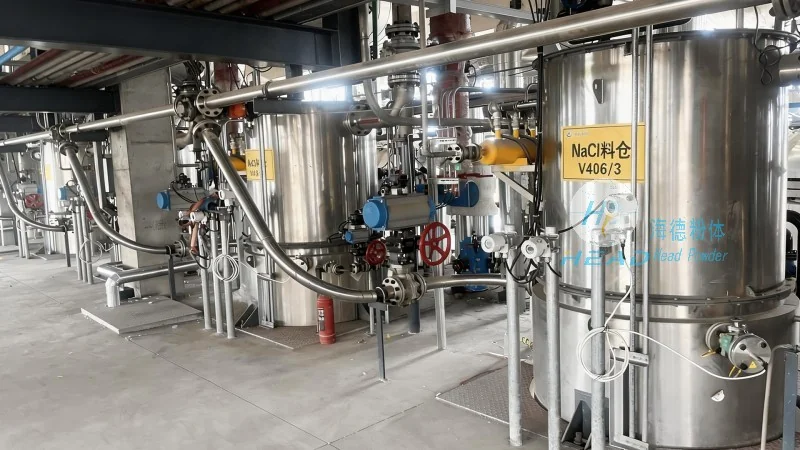
In the construction industry, pneumatic conveying systems are widely used for transporting cement and other dry powders to job sites. The positive pressure system is often preferred for short-distance transport from storage silos to mixing equipment. The system ensures that the cement is delivered in a consistent and controlled manner, reducing the risk of clogging and improving the quality of the concrete mix. For longer distances, negative pressure systems may be employed to transport the material from the factory to the construction site, ensuring efficient and dust-free delivery.
In the food processing industry, pneumatic conveying systems are used to transport powdered ingredients, such as flour, sugar, or protein powders, along with water to form a batter or dough. The system maintains hygiene and prevents contamination, as the pipeline is sealed and the material is transported under controlled conditions. The positive pressure system is commonly used for short-distance transport within the processing plant, while the negative pressure system may be used for longer distances, such as from storage silos to the production line.
In chemical manufacturing, pneumatic conveying systems are used to transport various chemical powders, such as pigments, catalysts, or reagents, along with water to form a slurry for processing. The system ensures that the chemical mixture is uniform and free from contamination, which is crucial for maintaining product quality and safety. The negative pressure system is often preferred for long-distance transport, as it can handle the material over several kilometers without compromising the quality of the mixture.
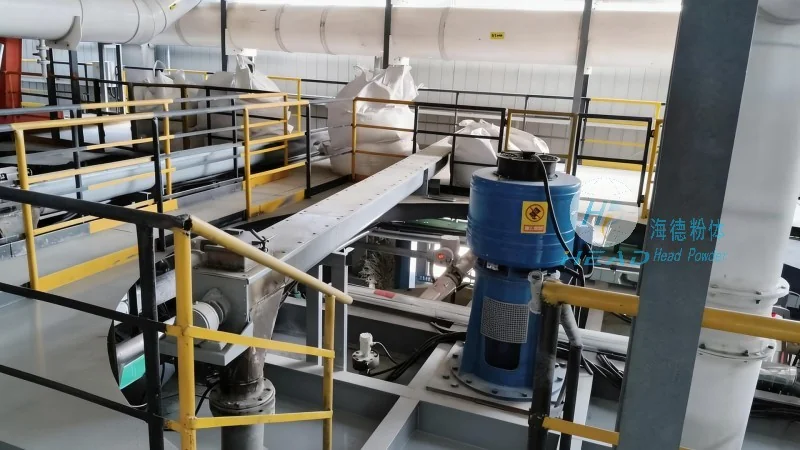
Pneumatic conveying systems offer several benefits for water-in-powder delivery applications. These include improved efficiency in material transport, reduced labor costs, and enhanced safety by minimizing dust exposure. The systems also provide better control over the material mixture, ensuring consistent quality of the final product. Additionally, pneumatic conveying systems are flexible and can be easily integrated into existing production lines, allowing for scalability and adaptability to changing production needs.
HeadPowder Engineering, with its expertise in pneumatic conveying systems, provides tailored solutions for water-in-powder delivery applications. By understanding the different types of systems and their practical applications, industries can optimize their material handling processes, improve efficiency, and enhance product quality. The company’s commitment to quality and innovation ensures that clients receive reliable and effective solutions for their material transport needs.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top